HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for the transportation of potassium carbonate fertilizer materials. These systems are engineered to ensure efficient, reliable, and safe material handling in agricultural and industrial applications. The following sections detail the operational process and working principles of such equipment, highlighting key components and their functions.
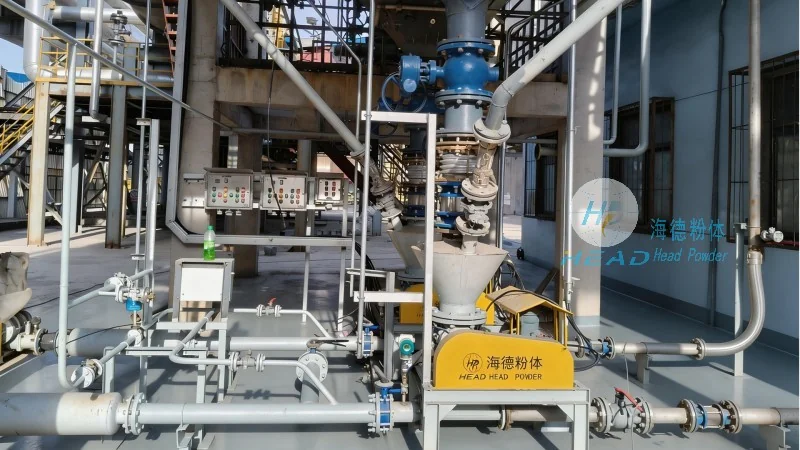
Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system for potassium carbonate fertilizer materials is the use of air or gas to transport bulk materials through a pipeline network. The system typically operates on the principle of creating a pressure differential between the inlet and outlet of the conveying line. By injecting air at high pressure or using vacuum suction, the material is entrained and carried through the pipeline to the destination point. This method eliminates the need for mechanical components like conveyors or elevators, reducing maintenance costs and increasing operational efficiency.
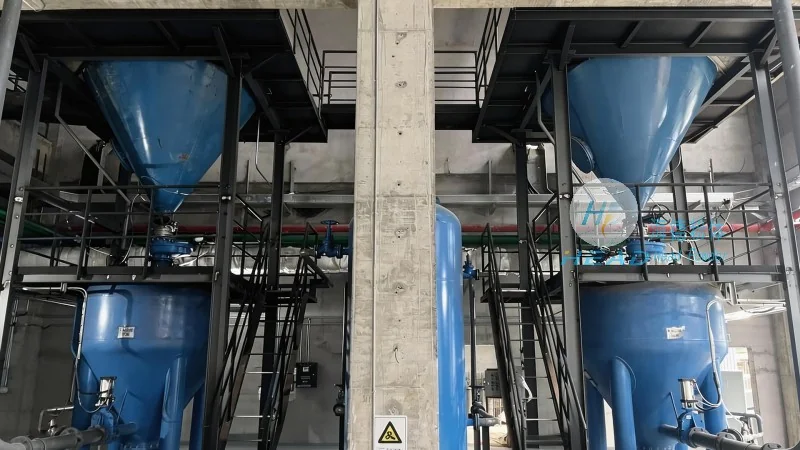
Operational Process of the Equipment
The operation of a pneumatic conveying system for potassium carbonate fertilizer materials involves several key steps. First, the material is fed into the hopper or feeder, where it is metered and prepared for transport. The feeder then delivers the material to the conveying line, either by pressure or suction. The air is introduced into the system, either at the inlet (pressure system) or the outlet (vacuum system), creating the necessary flow. The material is then carried through the pipeline, which may include bends, expansions, or filters to ensure smooth transport. At the receiving end, the material is discharged into a storage silo or processing unit. The system is equipped with control mechanisms to regulate the flow rate, pressure, and air volume, ensuring consistent and reliable operation.
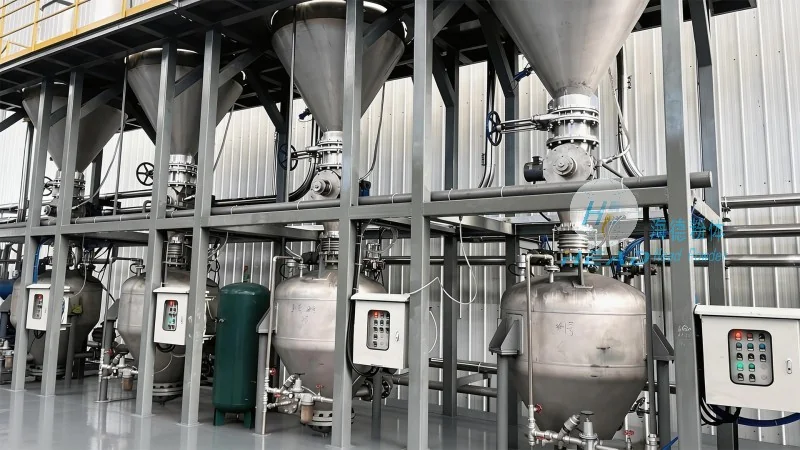
Key Components and Their Functions
Several critical components contribute to the effective operation of a pneumatic conveying system for potassium carbonate fertilizer materials. These include: 1. **Feeder/Hopper**: This component stores and meters the material, ensuring a consistent feed rate to the conveying line. 2. **Conveying Pipeline**: The pipeline network through which the material and air travel. It is typically made of durable materials like stainless steel or plastic to withstand the abrasive nature of the fertilizer. 3. **Air Supply System**: This system provides the necessary air pressure or vacuum. It includes compressors, air dryers, and filters to ensure clean and dry air, preventing material contamination and equipment damage. 4. **Control Valves and Regulators**: These components regulate the air flow and pressure, allowing precise control over the conveying process. 5. **Filters and Cyclones**: These are used to separate the material from the air at the receiving end, ensuring clean air is released and the material is properly collected.
Advantages of Pneumatic Conveying for Potassium Carbonate Fertilizer
Implementing a pneumatic conveying system for potassium carbonate fertilizer materials offers numerous advantages over traditional mechanical conveying methods. These include: 1. **Reduced Labor Costs**: The automated system minimizes the need for manual handling, reducing labor expenses and improving safety. 2. **Increased Efficiency**: The system operates continuously, with minimal downtime, leading to higher production throughput. 3. **Improved Product Quality**: The enclosed system prevents contamination from dust, moisture, or other environmental factors, maintaining the quality of the fertilizer. 4. **Space Efficiency**: The compact design of the system saves valuable space in industrial facilities, making it suitable for both large and small operations. 5. **Environmental Benefits**: The system reduces dust emissions and noise pollution, contributing to a cleaner and safer working environment.
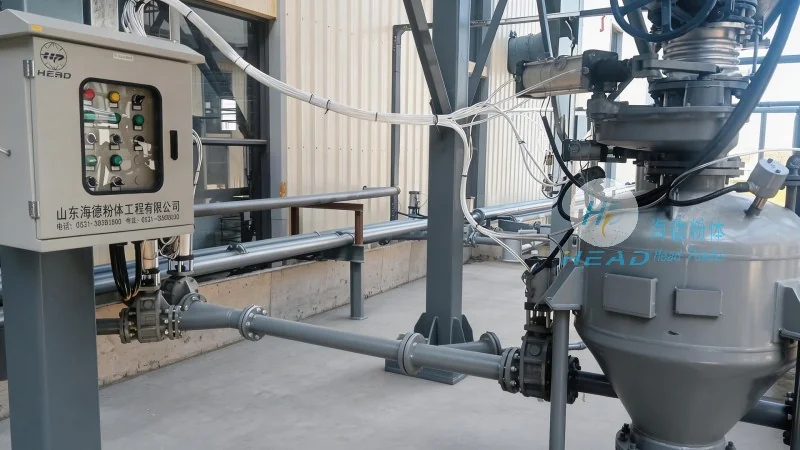
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in the design, production, and installation of pneumatic conveying equipment for various industrial applications. With years of experience in the field, the company has developed advanced solutions tailored to the specific needs of fertilizer manufacturers, ensuring reliable and efficient material handling. HeadPowder's commitment to quality and innovation has made it a trusted partner for businesses seeking to enhance their operational efficiency and product quality.




