HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced dust removal and material conveying solutions. The pulse dust removal material conveying system is a sophisticated piece of equipment designed to efficiently handle bulk materials while simultaneously ensuring high-efficiency dust collection. This system integrates multiple functional components to achieve optimal performance in industrial applications.
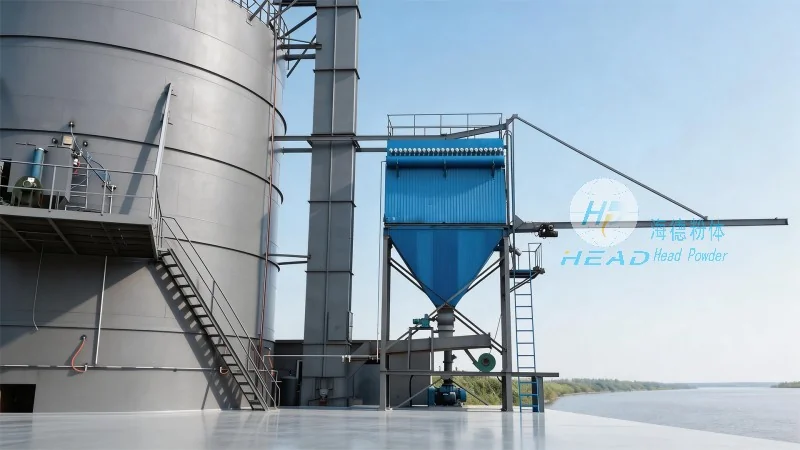
Overview of the System's Operation
The operation of the pulse dust removal material conveying system begins with the initial setup and startup procedures. The system is typically activated by a control panel that manages the flow of material and the timing of the pulse cleaning cycles. Once started, the equipment initiates the material feeding process, where bulk materials are drawn from a hopper or storage silo and transported through a series of pipes or ducts. Simultaneously, the dust removal mechanism is engaged, utilizing a series of pulses to agitate and remove accumulated dust from the system's filter bags or other filtration components.
Step-by-Step Operation Process
1. **Material Loading**: The bulk material is loaded into the hopper, which acts as the initial storage and feeding point. The hopper's design ensures a consistent flow of material into the conveying line, minimizing blockages and ensuring smooth operation.
2. **Conveying Initiation**: The control system activates the conveyor motor, which drives the material through the pipeline. The speed of the conveyor is adjustable based on the material's characteristics and the required throughput.
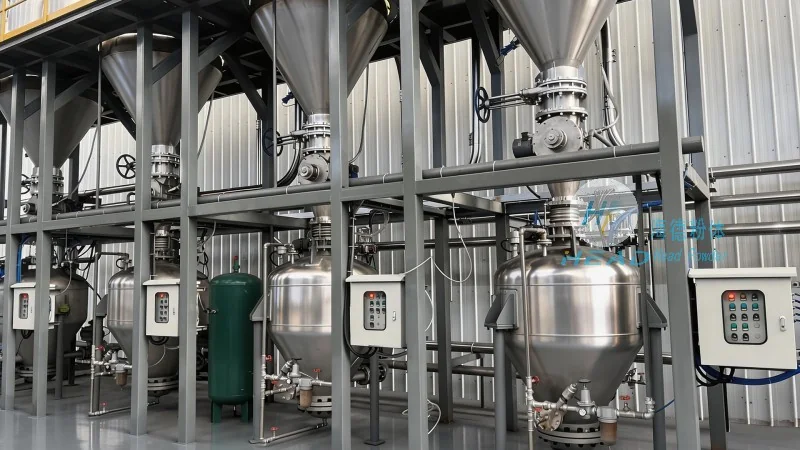
3. **Pulse Cleaning Cycle**: At regular intervals, the control system triggers a pulse sequence. This involves a rapid increase in air pressure within the filter housing, which causes the filter bags to expand and contract. This action dislodges dust particles that have accumulated on the filter surfaces, allowing them to fall into a dust hopper for collection.
4. **Dust Collection and Disposal**: The collected dust is stored in a separate hopper or container, which can be emptied at regular intervals. The system's design ensures that the dust removal process does not interrupt the material conveying operation, maintaining continuous production.
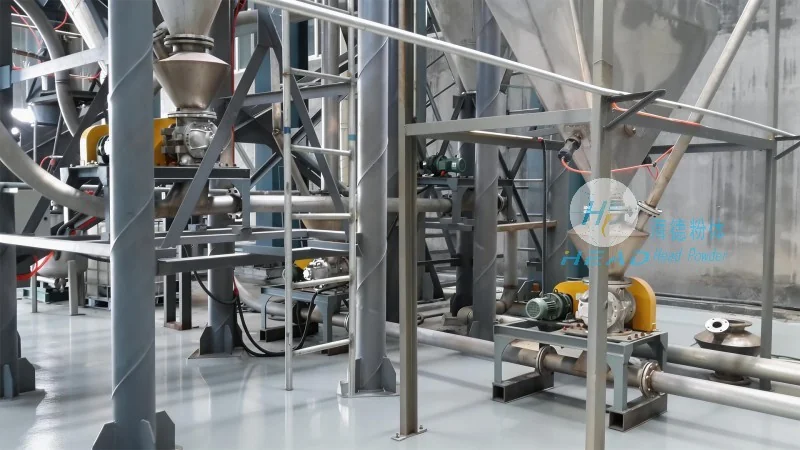
Working Principle of the System
The pulse dust removal material conveying system operates on the principle of combining material transport with dust filtration. The core components include a material conveyor, a dust filter system, and a pulse control unit. The material is transported through a sealed pipeline, which prevents dust from escaping into the environment. The dust filter, typically consisting of fabric filter bags, captures fine particles from the air stream. The pulse cleaning mechanism periodically cleans the filter bags, ensuring that the filtration efficiency remains high throughout the operation.
Key Technical Features
HeadPowder's pulse dust removal material conveying system is equipped with several advanced features that enhance its performance and reliability. These include:
- Efficient Dust Removal: The pulse cleaning cycle ensures that dust accumulation on the filter bags is minimized, maintaining high filtration efficiency and preventing system downtime.
- Continuous Operation: The system is designed for continuous operation, with the pulse cleaning process occurring without interrupting the material conveying, which is crucial for maintaining production throughput.
- Adjustable Parameters: The control system allows for adjustment of the pulse frequency, conveyor speed, and air pressure, enabling customization to suit different material types and application requirements.
- Sealed Design: The sealed pipeline and filtration system prevent dust emissions, ensuring compliance with environmental regulations and providing a safer working environment.
Application and Benefits
This system is widely used in various industries, including cement, mining, and chemical processing, where bulk materials need to be transported while maintaining air quality standards. The benefits of using the pulse dust removal material conveying system include reduced dust emissions, lower maintenance costs due to efficient cleaning, and increased operational efficiency. By integrating dust removal directly into the material conveying process, the system eliminates the need for separate dust collection equipment, simplifying the overall process and reducing capital and operational expenses.




