

What is a White Ash Powder Conveyor? And What Are Its Design Principles?
White ash powder conveyors are specialized industrial equipment designed to transport bulk white ash powder efficiently and safely. As a key component in many industrial processes, these conveyors play a crucial role in material handling, ensuring that white ash is moved from storage to processing or disposal areas with minimal loss and maximum efficiency. Understanding the design principles behind these systems is essential for anyone involved in the handling of white ash, as it directly impacts operational performance, safety, and cost-effectiveness.
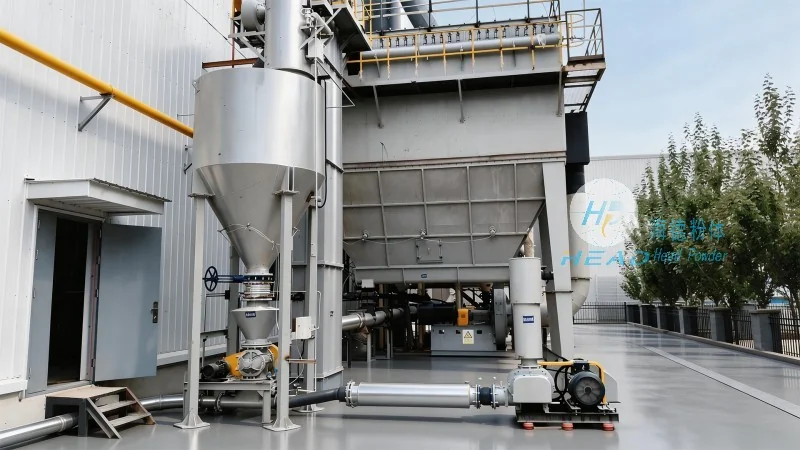
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling equipment, specializes in the design, manufacturing, and supply of white ash powder conveyors. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring reliable and efficient powder transport solutions. HeadPowder's expertise lies in creating customized conveyor systems that meet the specific needs of clients, ensuring optimal performance in diverse operational environments.
What is a White Ash Powder Conveyor?
A white ash powder conveyor is a mechanical system engineered to move white ash powder from one location to another. This equipment is particularly important in industries such as power generation, where white ash is a byproduct of coal combustion. The primary function of these conveyors is to transport the fine, powdery material in a controlled manner, preventing dust dispersion and ensuring that the material reaches its destination without degradation or loss. The design of these conveyors is tailored to handle the unique properties of white ash, including its fine particle size, potential moisture content, and the need for dust control.
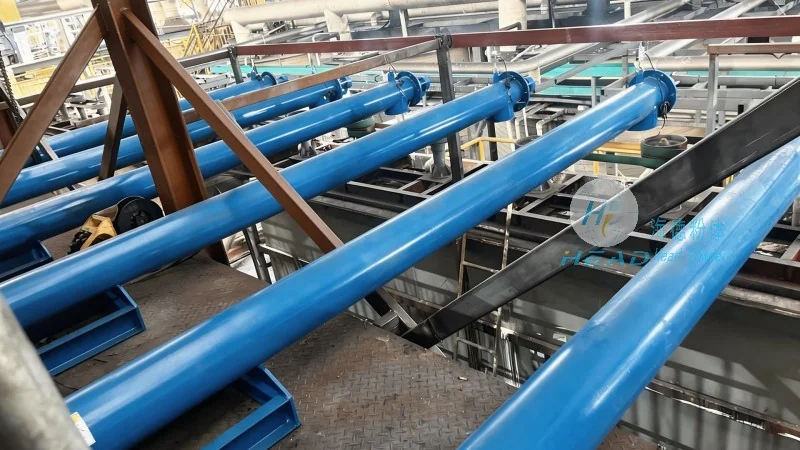
Key Design Principles of White Ash Powder Conveyors
The design of a white ash powder conveyor is based on several critical principles that ensure its effectiveness and reliability. First, the system must provide excellent dust containment and sealing to prevent the release of fine particles into the environment. This is achieved through the use of airtight enclosures, flexible seals, and positive pressure or negative pressure systems that maintain a controlled atmosphere within the conveyor. Second, the conveyor must be capable of handling the abrasive and potentially corrosive nature of white ash. Materials such as stainless steel, high-grade alloys, and wear-resistant coatings are often used to protect the internal components from wear and damage. Third, the system must be designed for efficient power transmission and minimal energy consumption. This involves the use of high-efficiency motors, variable speed drives, and optimized belt or screw designs that reduce friction and energy loss. Fourth, the conveyor must be easy to maintain and service. Modular designs, accessible components, and user-friendly control systems are incorporated to minimize downtime and maintenance costs.
Components and Mechanisms of White Ash Powder Conveyors
White ash powder conveyors typically consist of several key components that work together to achieve efficient material transport. The main components include a feeding hopper, a conveying mechanism (such as a screw, belt, or pneumatic system), a drive system, and a discharge outlet. The feeding hopper is designed to collect and store the white ash powder, ensuring a consistent flow into the conveyor. The conveying mechanism is the core of the system, responsible for moving the material along the path of the conveyor. Screw conveyors are commonly used for white ash due to their ability to handle fine powders and maintain a controlled flow. Belt conveyors may also be used, especially for longer distances or when the material needs to be elevated. The drive system provides the necessary power to operate the conveying mechanism, often using electric motors with variable speed drives to adjust the speed based on the material load. The discharge outlet is designed to release the white ash powder at the desired location, ensuring a smooth and controlled discharge process.
Advantages of Using White Ash Powder Conveyors
Implementing white ash powder conveyors offers several advantages for industrial operations. First, these systems improve operational efficiency by reducing the time and labor required for manual handling of white ash. This leads to increased productivity and reduced labor costs. Second, the use of enclosed and sealed conveyors minimizes dust exposure, improving workplace safety and compliance with environmental regulations. Third, the efficient design of these systems reduces energy consumption, leading to lower operational costs and a smaller environmental footprint. Fourth, the durability and reliability of modern white ash powder conveyors result in lower maintenance and replacement costs over the long term. Finally, the ability to customize these systems to specific requirements allows industries to optimize their material handling processes, ensuring that the conveyor meets the unique demands of their operations.
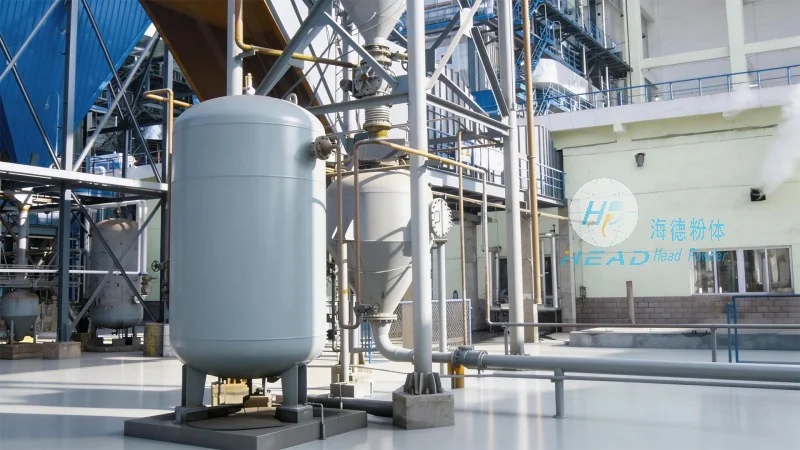
Applications of White Ash Powder Conveyors
White ash powder conveyors are widely used in various industrial applications, particularly in the power generation industry. In power plants, these conveyors are used to transport white ash from the boiler to storage silos or disposal sites. They are also used in other industries where white ash is a byproduct, such as in cement production or metal processing. The versatility of these conveyors allows them to be adapted for different applications, including the transport of other fine powders like fly ash, cement, or chemical powders. The design principles and components of white ash powder conveyors are often adaptable to handle these other materials, making them a valuable asset in diverse industrial settings.
Conclusion: The Importance of White Ash Powder Conveyors
In conclusion, white ash powder conveyors are essential equipment for industries dealing with white ash powder. Their design principles, which focus on dust control, material handling efficiency, and durability, make them a reliable solution for transporting white ash safely and effectively. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing these systems, ensuring that industries can meet their operational needs while maintaining high standards of safety and environmental responsibility. As technology continues to advance, the design and performance of white ash powder conveyors are likely to improve, further enhancing their role in industrial material handling.