Mobile powder pneumatic conveying equipment has become an essential solution in various industrial sectors, offering efficient and flexible methods for transporting bulk powders. This equipment is designed to handle a wide range of powder materials, from fine powders to bulk materials, with minimal dust generation and high transfer efficiency. The following article explores the fundamental principles behind this technology and highlights key application scenarios where such equipment excels.
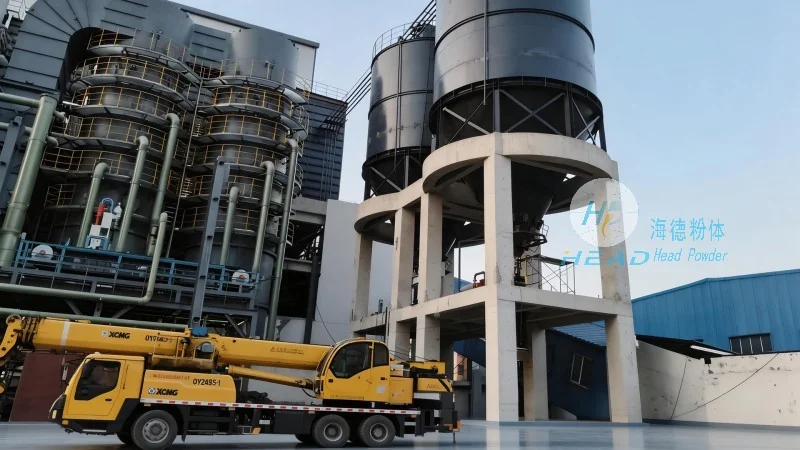
Introduction to Mobile Powder Pneumatic Conveying Systems
Mobile powder pneumatic conveying systems utilize air as the primary medium to transport powder materials through a network of pipes and components. Unlike traditional mechanical conveying methods, which rely on belts or screws, pneumatic systems offer advantages such as reduced maintenance, lower energy consumption, and the ability to handle materials that are sensitive to moisture or contamination. The core of these systems lies in the interaction between the powder and the air flow, which can be categorized into two main types: dilute phase and dense phase conveying.
Principle of Operation: How Mobile Pneumatic Conveying Works
The operation of mobile powder pneumatic conveying equipment is based on the principle of fluidization. In dilute phase systems, air is introduced at a high velocity, creating a suspension of powder particles in the air stream. This allows the powder to be transported over long distances with minimal pressure drops. In contrast, dense phase systems use lower air velocities and higher pressure to move the powder in a more compact form, reducing the risk of particle degradation and ensuring more precise control over the material flow. The mobile nature of these systems, often equipped with wheels or skids, enables them to be easily repositioned for different operational needs, making them highly adaptable for dynamic industrial environments.
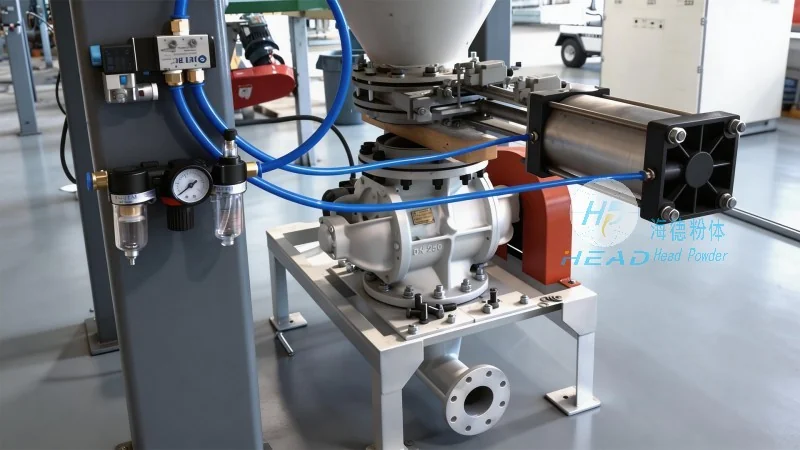
Key Components and Their Functions
Mobile powder pneumatic conveying systems consist of several critical components that work in tandem to ensure efficient operation. These include the material feed hopper, which holds the powder and controls the flow rate; the air compressor, which generates the necessary air pressure; the conveying line, which transports the powder; and the discharge unit, which releases the material at the destination. Additionally, filters and cyclones are used to separate the powder from the air, preventing dust contamination and ensuring compliance with environmental regulations. The integration of these components in a mobile design allows for rapid setup and deployment, reducing downtime and increasing overall productivity.
Application Scenarios: Where Mobile Pneumatic Conveying Excels
Mobile powder pneumatic conveying equipment is widely used across multiple industries due to its versatility and efficiency. In the chemical industry, it is employed to transport raw materials and finished products, such as powders used in pharmaceuticals or specialty chemicals. The food and beverage sector utilizes these systems for handling ingredients like flour, sugar, and spices, ensuring hygienic and dust-free transfer. The construction industry benefits from mobile pneumatic conveyors for transporting cement, sand, and other bulk materials to job sites, reducing the need for manual handling and improving safety. Additionally, in the agricultural sector, these systems are used to move grain and other agricultural products from storage to processing facilities. The adaptability of mobile systems allows them to be deployed in various settings, from large-scale industrial plants to smaller, mobile processing units.
Advantages of Mobile Powder Pneumatic Conveying Equipment
Compared to traditional conveying methods, mobile powder pneumatic conveying offers several advantages that make it a preferred choice for many industries. One of the primary benefits is the reduction in dust and contamination, which is crucial for materials sensitive to moisture or air exposure. The systems also provide better control over the material flow, allowing for precise dosing and minimizing waste. Furthermore, the mobile design enables easy relocation, making it suitable for temporary or changing operational needs. The lower maintenance requirements and energy efficiency of pneumatic systems contribute to long-term cost savings, making them a sustainable choice for industrial applications.
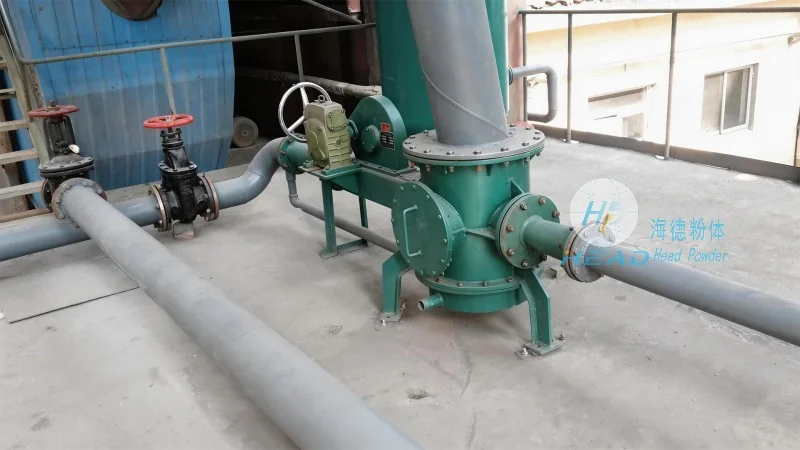
Conclusion: The Role of Mobile Powder Pneumatic Conveying in Modern Industry
Mobile powder pneumatic conveying equipment plays a vital role in enhancing operational efficiency and safety in various industrial applications. By leveraging the principles of fluidization and air-based transport, these systems offer a reliable and flexible solution for handling bulk powders. The adaptability and efficiency of mobile pneumatic conveying make it an indispensable tool for industries ranging from chemicals and food processing to construction and agriculture. As industrial demands continue to evolve, the continued development and application of such technology will remain critical in optimizing material handling processes and ensuring sustainable industrial practices.
For more information on mobile powder pneumatic conveying systems, please contact Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced material handling solutions based in Shandong, China.




