Refined sugar material pneumatic conveying equipment is a specialized system engineered to transport granular or powdered materials such as refined sugar efficiently and safely. This equipment is integral to the sugar processing industry, facilitating seamless material handling from storage to processing units. The technology underpinning these systems merges principles of fluid dynamics and mechanical engineering to achieve reliable, low-maintenance material transport.
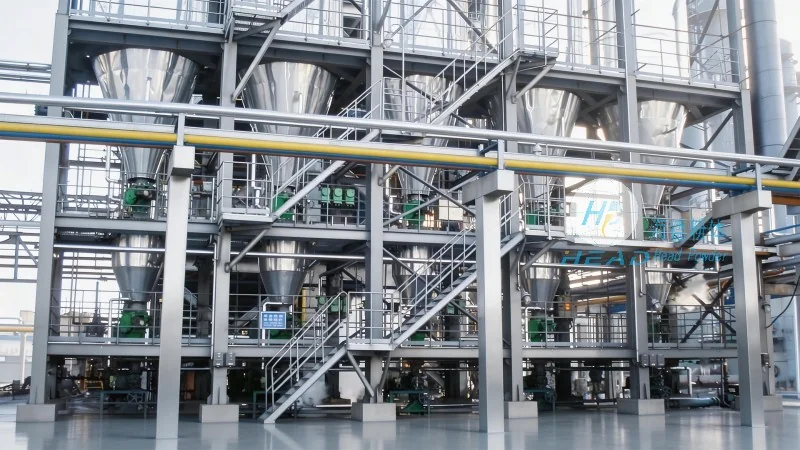
Principle of Refined Sugar Material Pneumatic Conveying Equipment
The core principle of pneumatic conveying for refined sugar involves utilizing compressed air or other gases to move the material through a pipeline network. This method, known as pneumatic transport, leverages pressure differentials created by air flow to lift and propel sugar particles. The equipment typically comprises a hopper for material storage, a blower or compressor to generate air flow, and a pipeline system directing the material to its destination. The process is based on creating a "slurry" of sugar and air, where the air acts as the medium to carry the material. This approach eliminates mechanical components like belts or buckets, reducing friction and wear on both the material and equipment.
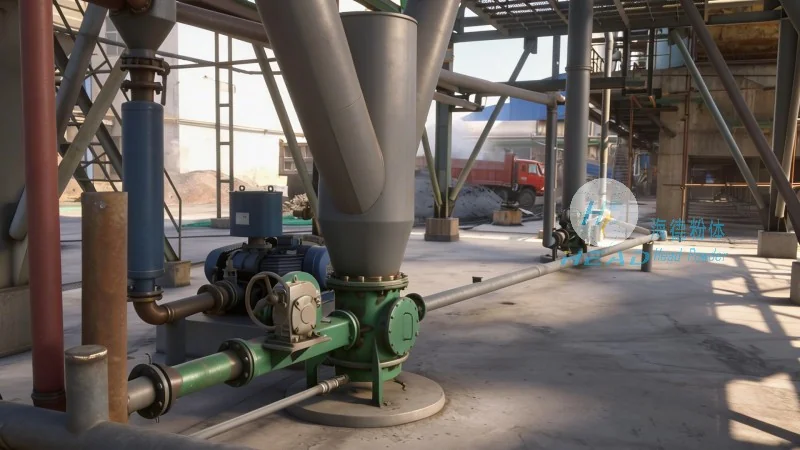
Working Scene Characteristics of Refined Sugar Material Pneumatic Conveying Equipment
The working scene characteristics of refined sugar pneumatic conveying systems are tailored to the specific demands of sugar processing facilities. These systems operate in closed environments, prioritizing hygiene, dust control, and material purity—critical for maintaining the quality of refined sugar. The closed system minimizes exposure to external contaminants and prevents product degradation, ensuring the crystalline structure and flavor of the sugar remain intact. Working scenes may include connections to storage silos, processing lines, or packaging areas, enabling seamless integration into production workflows. The systems are designed to handle varying flow rates, from low to high capacity, adapting to different production scales. Additionally, the equipment is constructed with materials like stainless steel and specialized coatings to withstand the corrosive and abrasive nature of sugar particles, ensuring durability and longevity.
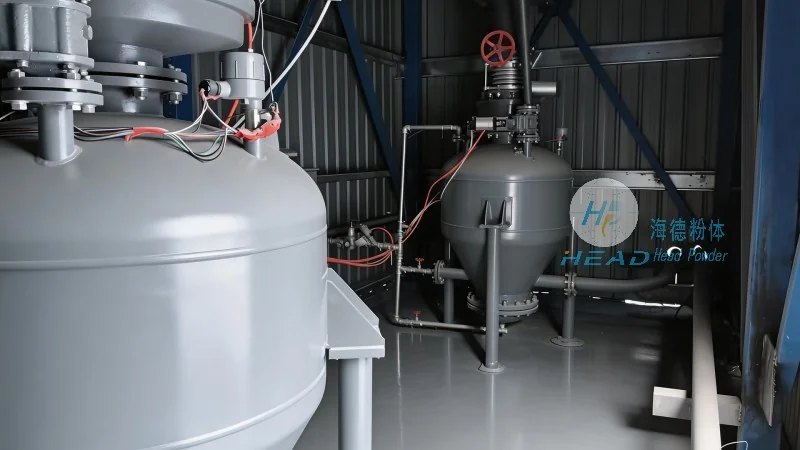
Application Advantages and Technical Features
Refined sugar material pneumatic conveying equipment offers distinct advantages over traditional mechanical transport methods. A primary benefit is the ability to transport materials in a dust-free environment, enhancing workplace safety and product quality. The closed system also reduces material loss and contamination risks, vital in food processing industries. Another key advantage is energy efficiency, as pneumatic systems often consume less power than mechanical conveyors, especially for long-distance transport. Technical features include adjustable air pressure controls for optimizing conveying speed and material flow. The equipment incorporates safety elements such as pressure relief valves and material flow sensors to prevent blockages and ensure smooth operation. Furthermore, the modular design allows for easy installation and maintenance, reducing downtime and operational costs.
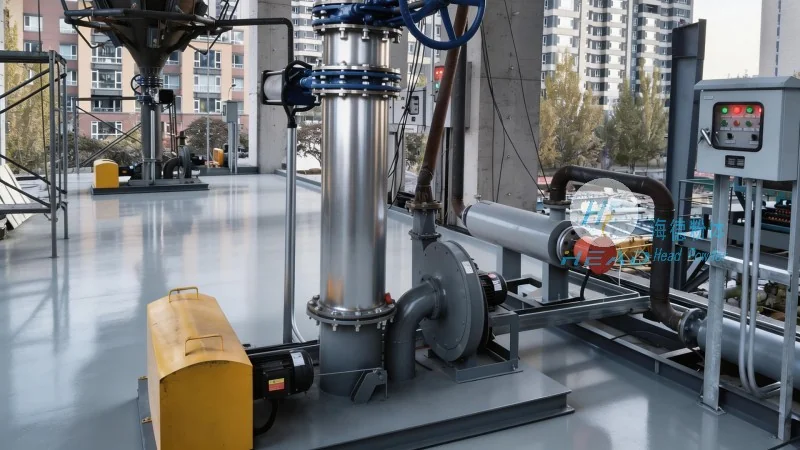
Company Information and Service Scope
HeadPowder, a leading manufacturer of industrial conveying equipment, specializes in designing and producing refined sugar material pneumatic conveying systems. With deep expertise in the sugar processing industry, HeadPowder has developed customized solutions to meet unique client requirements. The company is headquartered in Shandong, China, and leverages advanced engineering and manufacturing capabilities to deliver high-quality equipment. HeadPowder's products are recognized for reliability, efficiency, and compliance with industry standards, ensuring enhanced production processes for clients. The company's service scope includes equipment supply, technical support, installation, and maintenance, providing comprehensive solutions. By partnering with HeadPowder, sugar processing facilities benefit from advanced technology and professional support to optimize material handling operations.




