Principle and Working Scene Characteristics of Multi-Hopper Pneumatic Powder Conveying Systems
Release time:2026-09-19 16:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Multi-hopper pneumatic powder conveying systems represent a sophisticated technology designed to efficiently transport bulk powders over long distances or across complex layouts. At the core of this system is the multi-hopper pump, which serves as the central control unit for managing the material flow. The system operates by using compressed air to create a pressure differential that propels the powder particles through a network of pipes. Each hopper is equipped with an individual valve mechanism, allowing for precise control over the discharge of different powder types or batches. This modular design enables the system to handle multiple materials simultaneously, enhancing operational flexibility and efficiency.
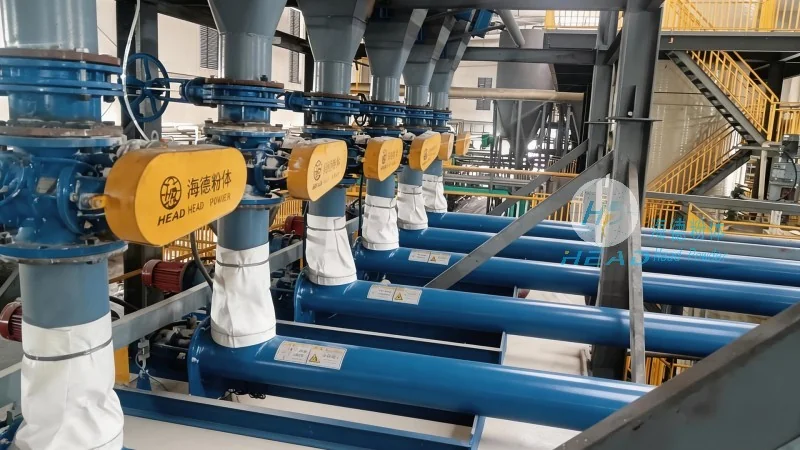
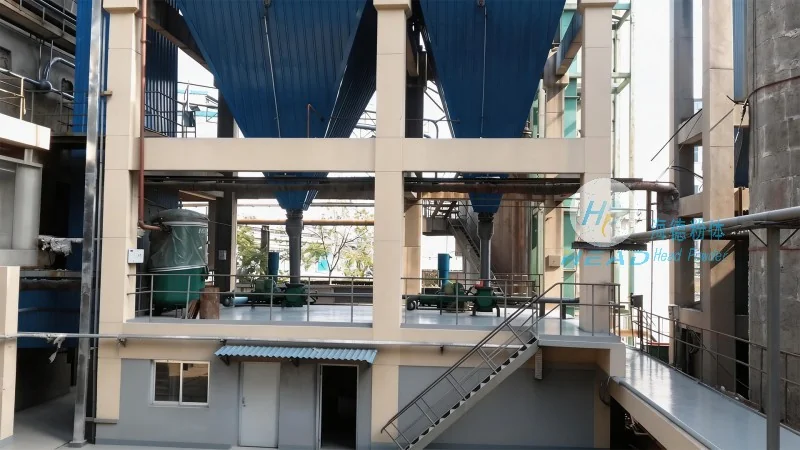
Working Principle of Multi-Hopper Pneumatic Conveying Systems
The fundamental principle of multi-hopper pneumatic powder conveying systems is based on the use of compressed air to transport dry powders in a closed pipeline system. The process begins with the loading of powders into each hopper. When a specific hopper is selected for operation, its valve opens, and the compressed air is introduced into the hopper, creating a pressure that forces the powder into the conveying line. The air and powder mixture then travels through the pipeline to the discharge point, where the air is separated from the powder, typically through a cyclone or filter. The separated powder is collected in a receiving hopper or container, while the air is either recirculated or vented to the atmosphere. This closed-loop operation minimizes material loss and ensures a clean, dust-free transfer process.
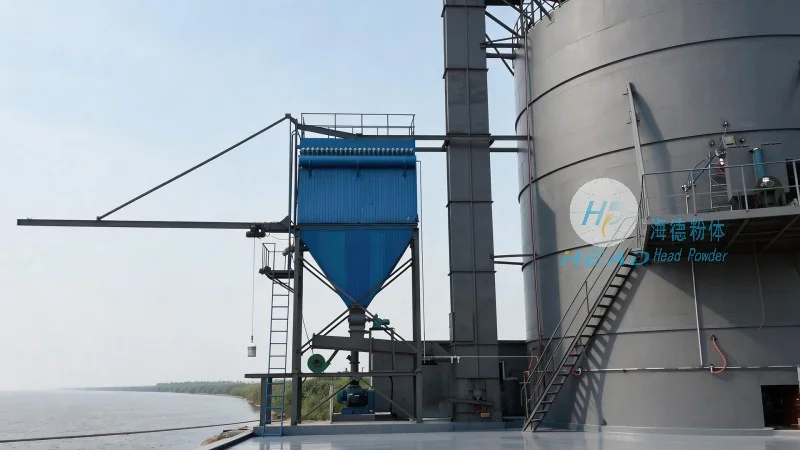
Key Working Scene Characteristics
Multi-hopper pneumatic powder conveying systems are particularly well-suited for industrial applications that require the handling of various bulk powders with different properties. The key characteristics that define their working scenes include: 1. **Modular and Scalable Design**: The system can be expanded or reconfigured to accommodate changes in production volume or material types, making it adaptable to evolving operational needs. 2. **Simultaneous Material Handling**: By utilizing multiple hoppers, the system can transport different powders concurrently, reducing downtime and increasing overall throughput. 3. **Low Maintenance Requirements**: The design minimizes moving parts in the conveying line, leading to lower maintenance costs and longer equipment lifespan. 4. **Environmental Friendliness**: The closed system prevents dust emissions, aligning with environmental regulations and promoting a safer working environment. 5. **Versatility in Application**: These systems are commonly used in industries such as food processing, pharmaceuticals, chemicals, and mining, where the transport of sensitive or hazardous powders is critical.
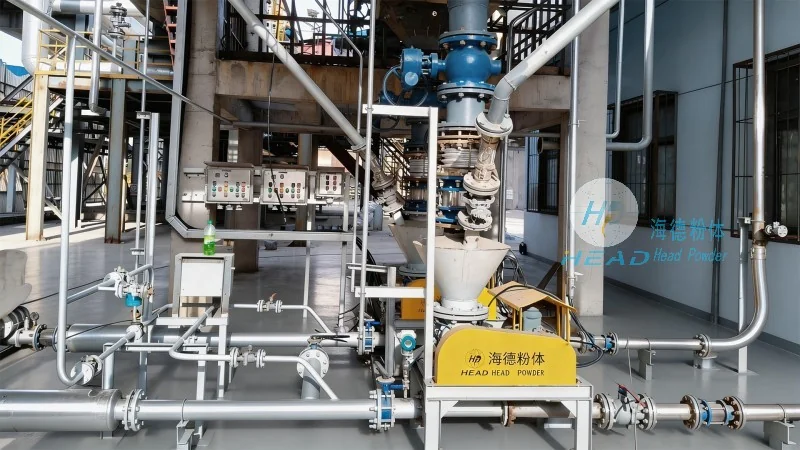
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of pneumatic conveying technology, specializes in the design, manufacturing, and installation of multi-hopper powder conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking efficient and reliable powder handling solutions. HeadPowder's products are engineered to meet the highest industry standards, ensuring durability, performance, and compliance with international safety and environmental regulations. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing capabilities and a team of experienced engineers to deliver tailored solutions for diverse industrial applications.




