Straw ash material pneumatic conveying equipment plays a crucial role in modern material handling and processing industries. This technology efficiently transports fine or bulk materials like straw ash through a pressurized or vacuum system, offering a dust-free, flexible, and energy-efficient solution compared to traditional methods such as belt conveyors or bucket elevators. The equipment is widely used in agricultural, environmental, and industrial sectors where the handling of lightweight, low-density materials is required.
Working Principle of Pneumatic Conveying Systems
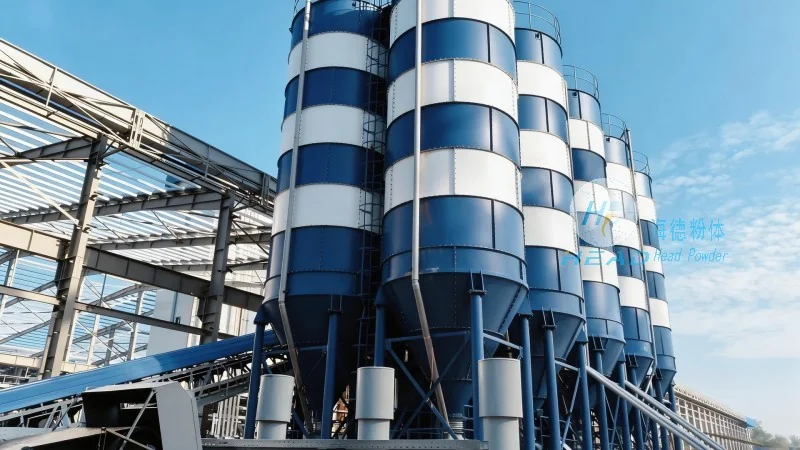
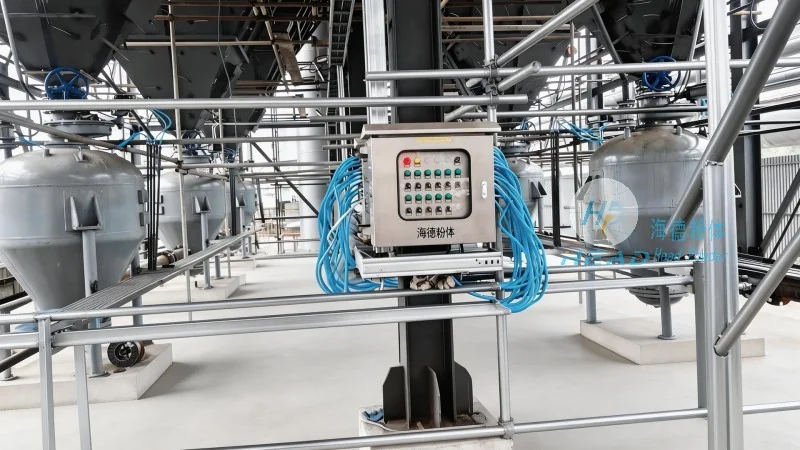
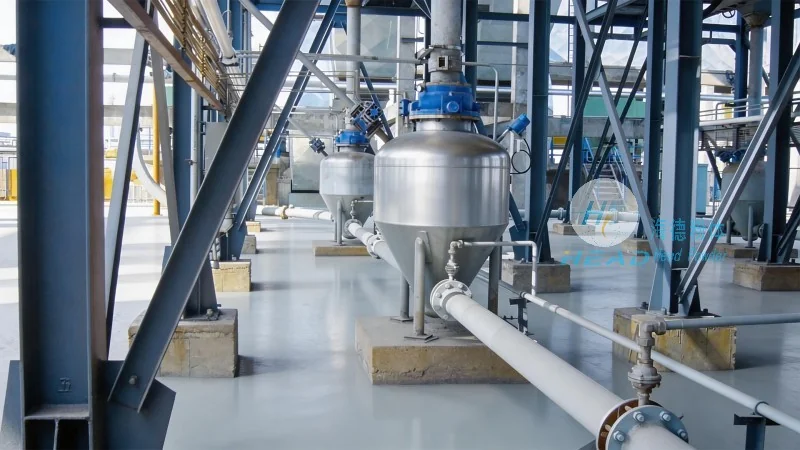
The core principle of pneumatic conveying involves the use of air or gas to move material particles through a pipeline. In a typical system, a blower or compressor generates airflow that draws or pushes the material from the source to the destination. The system can operate under positive pressure (where air pushes the material) or negative pressure (where air pulls the material). For straw ash, which is often fine and lightweight, a positive pressure system is commonly employed to ensure reliable transport without clogging. The equipment typically includes components such as a hopper for material storage, a feeder to control the flow rate, a pipeline network, and a receiver to collect the material at the end point. The design of the system is tailored to the specific properties of straw ash, including its particle size, moisture content, and flowability, to optimize performance and minimize operational issues.
Key Features and Application Scenarios
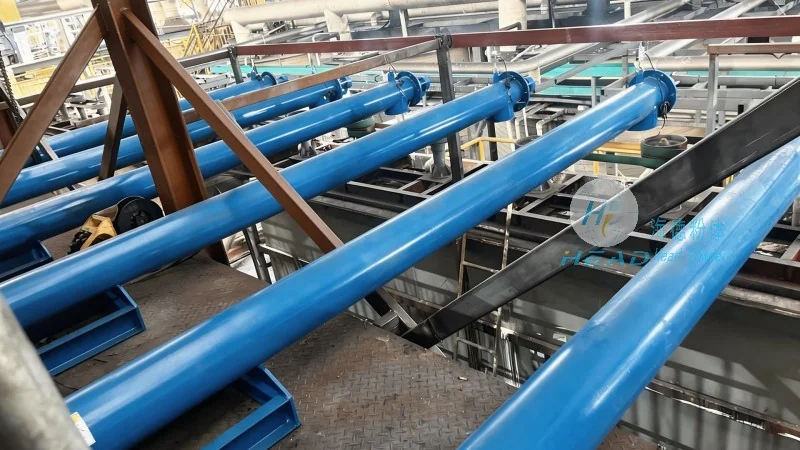
Straw ash material pneumatic conveying equipment offers several advantages that make it suitable for diverse working environments. One of the primary features is its ability to handle fine materials without generating excessive dust, which is critical for maintaining air quality and worker safety in agricultural and environmental applications. The system's flexibility allows for easy integration into existing production lines or facility layouts, as the pipeline can be installed in various configurations to accommodate different spatial constraints. Additionally, the equipment is capable of transporting materials over long distances with minimal energy consumption, making it an economical choice for large-scale operations. Typical application scenarios include the transportation of straw ash from storage silos to processing facilities, the delivery of ash to waste management sites, and the integration into biomass energy production systems where straw ash is used as a fuel or feedstock. The equipment's design also ensures low maintenance requirements, with components like the feeder and blower being easily accessible for routine checks and repairs.
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the name suggests, specializes in engineering solutions for material handling and processing. With a focus on innovative and efficient equipment design, the company has established itself as a leading provider of pneumatic conveying systems and related technologies. HeadPowder's products are tailored to meet the specific needs of clients in the agricultural, environmental, and industrial sectors, ensuring optimal performance and reliability. The company is headquartered in Shandong, China, and leverages local manufacturing expertise and global market insights to deliver high-quality solutions. By combining advanced engineering principles with practical application knowledge, HeadPowder continues to enhance the efficiency and sustainability of material handling processes for its clients worldwide.




