Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field, specializes in the design and implementation of industrial alkali powder conveying systems. These systems are crucial for efficiently transporting alkaline powders in various industrial applications, ensuring safety, reliability, and optimal performance. The company’s expertise lies in understanding the unique challenges associated with handling such materials and developing tailored solutions that meet specific operational requirements.
The Core Principles of Alkali Powder Conveying Systems
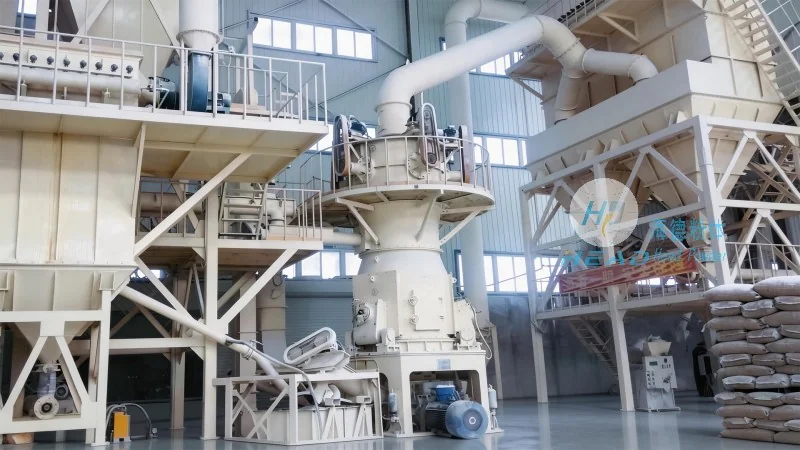
Industrial alkali powder conveying systems operate on fundamental principles that ensure the safe and efficient movement of powders. The primary components typically include feeders, conveyors, and control systems, each playing a critical role in the overall process. Feeders are responsible for accurately metering the powder, while conveyors transport it through pipelines or other pathways. Control systems monitor and regulate the flow, maintaining consistent pressure and preventing blockages. The design of these systems must account for the physical properties of the alkali powders, such as their particle size, moisture content, and flow characteristics, to ensure smooth operation and minimize material degradation.
Key Working Scene Characteristics of Industrial Alkali Powder Conveying Systems
Industrial alkali powder conveying systems are deployed in diverse working environments, each with distinct characteristics that influence system design and performance. For instance, in chemical manufacturing plants, these systems must handle high volumes of alkali powders while maintaining strict safety protocols to prevent dust explosions and contamination. In food processing facilities, the systems need to be hygienic and meet stringent sanitary standards to ensure product quality and compliance with regulatory requirements. Additionally, in mining and mineral processing operations, the systems may need to handle abrasive or corrosive powders, requiring robust materials and advanced sealing technologies. The versatility of these systems allows them to adapt to various industrial settings, from small-scale production lines to large-scale processing facilities.
Application Scenarios in Chemical and Pharmaceutical Industries
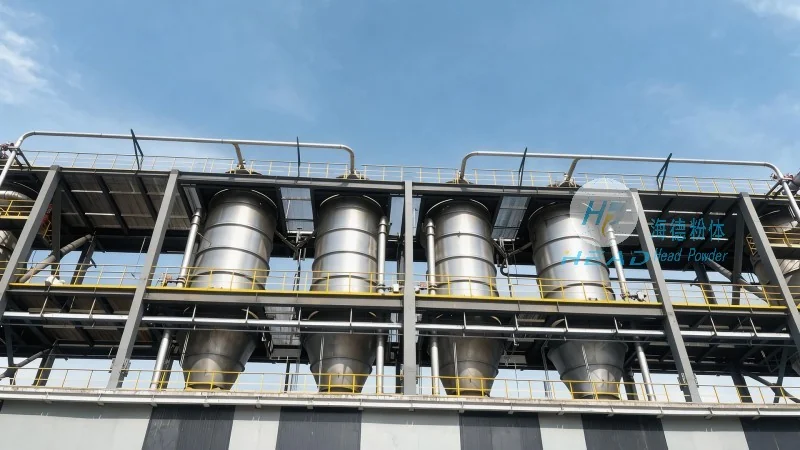
In the chemical and pharmaceutical industries, industrial alkali powder conveying systems are essential for transporting materials like sodium hydroxide, calcium hydroxide, and other alkaline compounds. These systems must be designed to handle the reactive nature of these materials and prevent any contamination that could affect product purity. The company’s solutions often incorporate specialized equipment such as rotary valves, pneumatic conveyors, and vacuum systems to ensure precise and controlled delivery. For example, in a chemical plant producing cleaning agents, the system may need to transport sodium hydroxide from storage silos to reaction tanks, requiring high-precision metering to maintain the correct chemical ratios. The reliability of the conveying system directly impacts production efficiency and product quality, making it a critical component in the overall process.
Application Scenarios in Food and Beverage Processing
Food and beverage processing facilities rely on industrial alkali powder conveying systems for handling ingredients like baking soda, calcium carbonate, and other alkaline additives. The systems must adhere to strict hygiene standards and be constructed from food-grade materials to prevent any cross-contamination. The design often includes features such as easy-to-clean surfaces, sealed components, and minimal dead zones to maintain sanitary conditions. In a bakery, for instance, the system may transport baking soda from bulk storage to mixing equipment, ensuring consistent dosing for optimal product texture. The efficiency of the conveying system helps maintain production line speed and reduces downtime, which is crucial in fast-paced food processing environments.
Application Scenarios in Mining and Mineral Processing
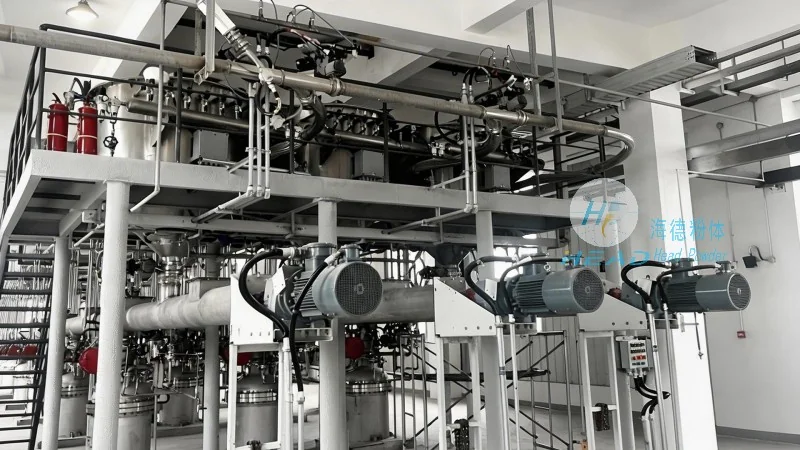
Mining and mineral processing operations use industrial alkali powder conveying systems to transport alkaline reagents and fluxes used in ore processing. These systems must be capable of handling abrasive and corrosive materials, often requiring heavy-duty components and advanced wear-resistant materials. The design may include high-capacity conveyors and robust feeding mechanisms to handle large volumes of material. For example, in a copper mining operation, the system may transport calcium hydroxide to leaching tanks, where it reacts with the ore to extract valuable metals. The reliability of the conveying system is vital for maintaining the flow of reagents and ensuring consistent extraction rates, which directly impacts the overall profitability of the mining operation.
Advantages of Industrial Alkali Powder Conveying Systems
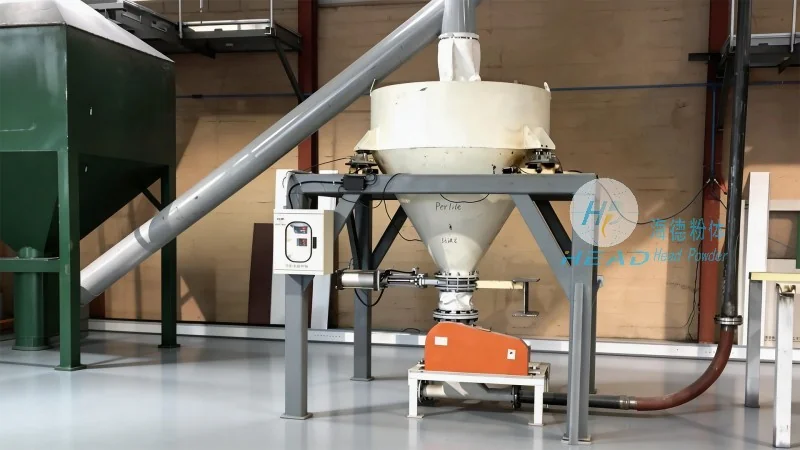
Industrial alkali powder conveying systems offer several advantages that make them indispensable in various industrial applications. One key advantage is their ability to handle high volumes of material with minimal labor, reducing operational costs and increasing productivity. The systems are also designed for durability and long-term reliability, with components that can withstand the harsh conditions associated with alkali powders. Additionally, the systems provide precise control over the flow rate, ensuring consistent delivery and preventing over or under-dosing. This precision is critical in processes where the exact amount of alkali powder is essential for product quality and safety. The company’s solutions often incorporate advanced monitoring and diagnostic features, allowing for real-time system performance tracking and proactive maintenance, which further enhances operational efficiency and reduces downtime.
Conclusion: Tailored Solutions for Industrial Alkali Powder Conveying
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in industrial alkali powder conveying systems to provide customized solutions that meet the unique needs of each client. By understanding the specific requirements of different industries and applications, the company designs and implements systems that optimize performance, safety, and cost-effectiveness. Whether for chemical manufacturing, food processing, or mining operations, the company’s systems are engineered to deliver reliable and efficient powder handling. With a focus on innovation and quality, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner in the development of advanced industrial conveying solutions, ensuring that clients can achieve their operational goals with confidence.




