Bulk material handling systems are integral to modern industrial operations, enabling the efficient storage, transfer, and processing of bulk materials like powders, granules, and other granular substances. These systems are designed to streamline material flow from storage silos to processing equipment or transportation vehicles, minimizing downtime and maximizing productivity. The core purpose of a bulk material handling system is to ensure that materials are moved safely, consistently, and in compliance with operational requirements, thereby supporting the overall efficiency of industrial processes.
Key Components and Their Roles
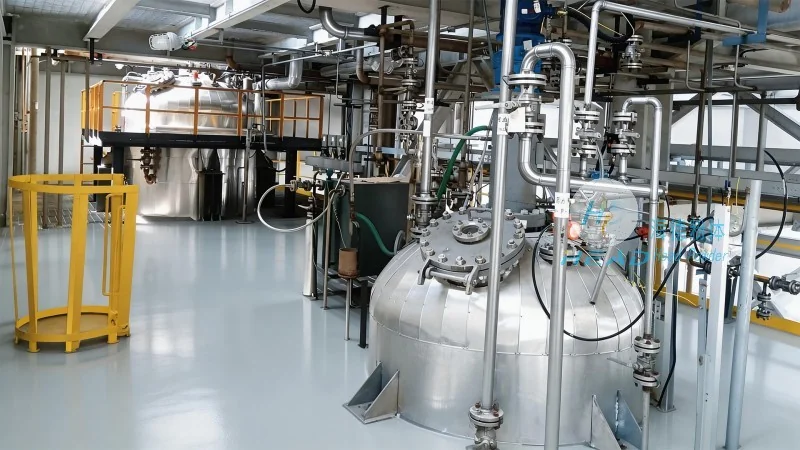
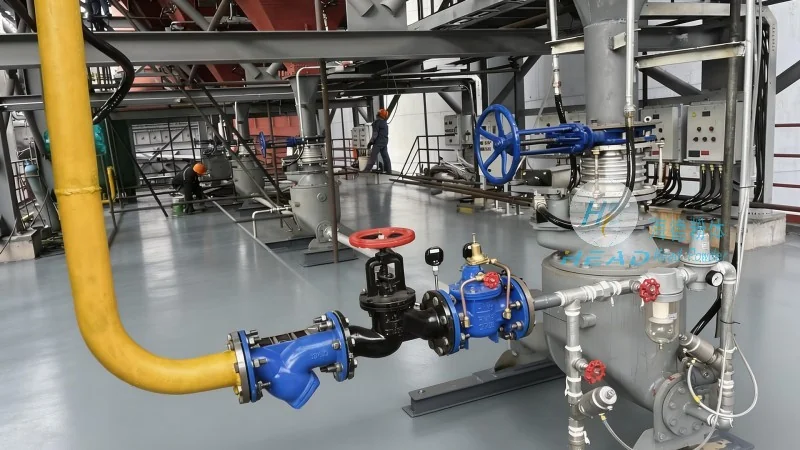
A typical bulk material handling system comprises several interrelated components, each with a specific function in the material flow process. The storage silo, often constructed from steel or reinforced concrete, serves as the primary container for bulk materials, providing a stable and secure storage solution. Silos are designed to accommodate large volumes of material, with features such as a conical or hopper bottom to facilitate controlled discharge. Conveyor belts, including belt conveyors and screw conveyors, are used to transport materials horizontally or vertically, depending on the layout and operational needs. Belt conveyors are ideal for long-distance horizontal transport, while screw conveyors are effective for vertical or inclined transport, especially for powders and granules. Feeders, such as rotary valves, vibratory feeders, or gate valves, regulate the flow rate of materials from the silo to downstream equipment, ensuring consistent and controlled discharge. This control is critical to prevent issues like bridging, rat-holing, or excessive pressure buildup, which can lead to blockages or equipment failure. Control systems, integrated with sensors and automation technology, monitor and adjust the system's performance in real-time. These systems may include level sensors to detect silo fill levels, flow meters to measure material throughput, and alarm systems to alert operators of any anomalies, ensuring proactive maintenance and operational safety.
Design Principles for Optimal Performance
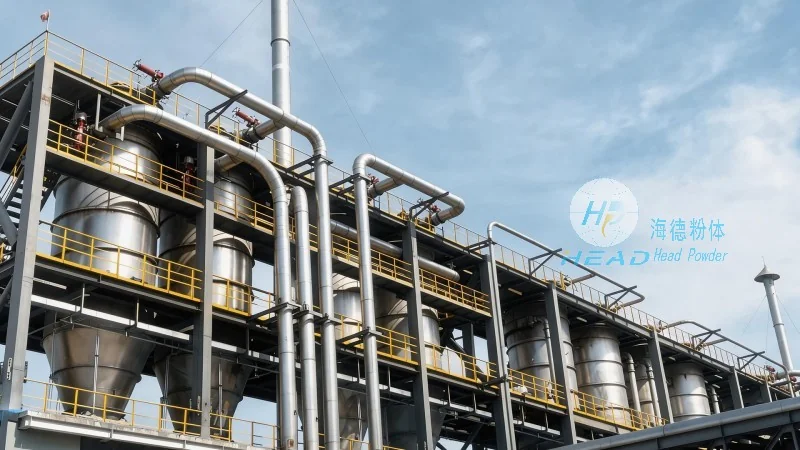
The design of a bulk material handling system is guided by several key principles to ensure reliability, efficiency, and longevity. Material compatibility is a primary consideration, as the system must be constructed from materials that can withstand the chemical and physical properties of the bulk material being handled. For instance, corrosive materials may require stainless steel components, while abrasive materials might necessitate reinforced structures to prevent wear and tear. Structural integrity is another critical factor, as the system must support the weight of the stored material and withstand external forces such as wind, seismic activity, or operational vibrations. Engineers employ load-bearing calculations, stress analysis, and structural testing to ensure the silo and conveyor structures are robust enough for long-term operation. Flow control is essential to maintain consistent material flow and prevent issues like bridging or rat-holing. Advanced feeder designs, such as variable-speed rotary valves or vibratory feeders, and flow aids like air cannons or vibrators are incorporated to address these challenges. Additionally, the system's layout and integration with other equipment are carefully planned to minimize material handling time and energy consumption, optimizing overall operational efficiency.
HeadPowder's Customized Solutions
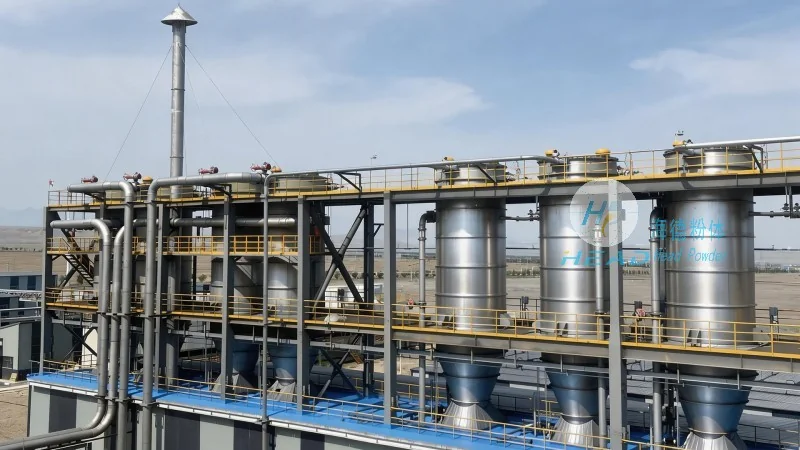
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of bulk material handling systems, offering tailored solutions that meet the unique needs of industrial clients. The company's expertise lies in designing and manufacturing comprehensive material handling systems that combine advanced technology with proven engineering principles. HeadPowder's team of experienced engineers works closely with clients to understand their specific requirements, including material characteristics, production capacity, space constraints, and operational goals. By leveraging decades of industry experience, HeadPowder ensures that each system is optimized for maximum efficiency, minimal maintenance, and long-term durability. The company's bulk material handling systems are built to withstand the demands of continuous operation, providing a reliable foundation for smooth material flow and operational success. Whether for industrial manufacturing, food processing, chemical production, or other sectors, HeadPowder's solutions are designed to enhance productivity, reduce downtime, and improve overall operational performance. The company's commitment to quality and customer satisfaction is reflected in its rigorous testing, quality control, and after-sales support, ensuring that clients receive systems that meet and exceed their expectations.




