High-pressure dense phase material handling systems represent a sophisticated approach to transporting bulk materials, particularly in industrial applications where efficiency, safety, and material integrity are paramount. These systems are designed to move powders, granules, and other particulate materials through pipelines under high pressure, creating a dense, slurry-like flow that minimizes particle separation and ensures consistent transport. Understanding the core components and design principles of such systems is crucial for optimizing material handling processes in various industries, including chemical, pharmaceutical, food processing, and mining.
Key Components of High-Pressure Dense Phase Material Handling Systems
The functionality of a high-pressure dense phase material handling system relies on several critical components that work in tandem to achieve efficient material transport. The primary elements include a high-pressure pump, which generates the necessary pressure to force the material through the pipeline; a feed hopper or feeder, which controls the material flow rate and ensures a consistent supply to the pump; and a pipeline system equipped with appropriate valves and fittings to direct and regulate the flow. Additionally, a pressure control system and a venting mechanism are essential to maintain system stability and prevent over-pressurization. The choice of materials for the pipeline and components is also critical, as they must withstand the high pressures and potential abrasive properties of the transported materials.
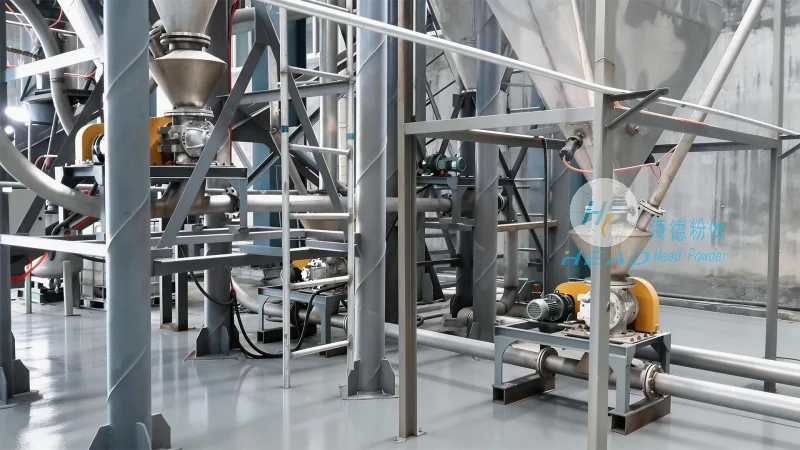
Design Principles for High-Pressure Dense Phase Material Handling
The design of high-pressure dense phase material handling systems is guided by several key principles aimed at maximizing efficiency and reliability. One of the fundamental principles is the creation of a "plug flow" or dense phase, where the material is forced to move as a cohesive mass rather than as individual particles. This is achieved by maintaining a high solids concentration and pressure within the pipeline, which reduces the risk of segregation and ensures uniform material distribution. Another critical principle is the optimization of pressure drop and flow rate, as excessive pressure loss can lead to system inefficiencies and increased energy consumption. Engineers must carefully calculate the required pressure and flow rates based on the material's properties, such as particle size, density, and flowability, as well as the pipeline length and diameter. Furthermore, the system design must incorporate safety features, such as pressure relief valves and monitoring systems, to prevent accidents and ensure compliance with industry regulations.
Applications and Benefits of High-Pressure Dense Phase Material Handling
High-pressure dense phase material handling systems are widely used in industries where the transportation of bulk materials requires precision and control. In the chemical industry, these systems are employed to transport reactive powders and granules, ensuring that the materials remain in a stable state during transport. In the pharmaceutical sector, they are used to handle sensitive ingredients, maintaining product purity and preventing contamination. The food processing industry also benefits from these systems, as they can transport powders like flour, sugar, and spices without compromising quality or safety. The primary benefits of high-pressure dense phase material handling include reduced material degradation, minimized segregation, improved process control, and enhanced safety compared to traditional pneumatic or gravity-based systems. Additionally, these systems can handle a wide range of materials, from fine powders to coarse granules, making them versatile for various industrial applications.
HeadPowder: A Leader in High-Pressure Dense Phase Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent manufacturer and supplier of high-pressure dense phase material handling systems. With headquarters in Shandong, China, HeadPowder specializes in designing and manufacturing customized solutions tailored to the specific needs of industrial clients. The company's expertise lies in integrating advanced engineering principles with practical application, ensuring that each system is optimized for efficiency, reliability, and safety. HeadPowder's product line includes high-pressure pumps, feeders, and pipeline components, all engineered to meet the demanding requirements of modern industrial processes. The company's commitment to quality and innovation has made it a trusted partner for businesses seeking to enhance their material handling capabilities. By leveraging their deep understanding of material properties and system design, HeadPowder provides solutions that help clients improve productivity, reduce operational costs, and maintain compliance with industry standards.




