Organic fertilizer powder conveying systems are critical components in modern agricultural and industrial applications, designed to efficiently transport bulk organic fertilizer powders from storage to processing or application points. These systems leverage advanced engineering principles to ensure reliable, low-loss, and safe material handling, addressing the unique challenges posed by organic fertilizer materials such as high moisture content, variable particle size, and potential caking or agglomeration. The core functionality of these systems revolves around the principles of pneumatic or mechanical conveying, tailored to the specific physical properties of organic fertilizers to optimize performance and operational efficiency.
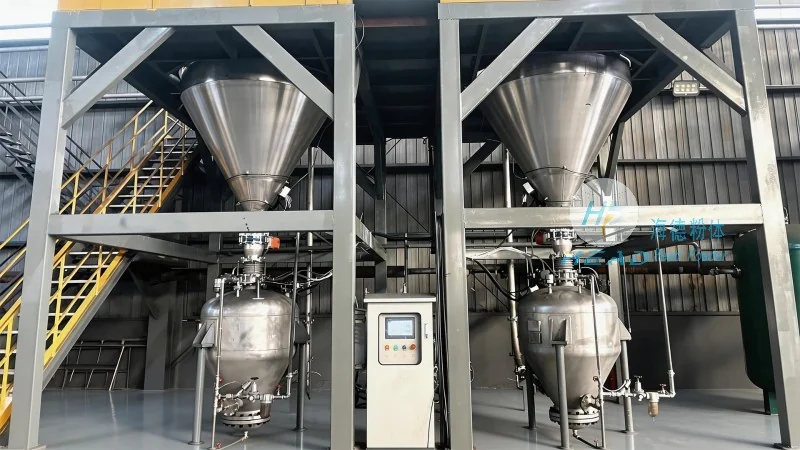
Core Principles of Powder Conveying Technology
The fundamental principles underlying organic fertilizer powder conveying systems include the use of air or mechanical forces to move particles through a pipeline or conveyor. Pneumatic conveying systems, for instance, utilize compressed air to create a flow that transports the powder, while mechanical systems employ screws, belts, or vibrating mechanisms to move material. For organic fertilizers, which often have cohesive properties, systems may incorporate features like agitators or air classifiers to maintain particle suspension and prevent blockages. The selection of conveying method depends on factors such as the fertilizer's moisture level, particle size distribution, and the required conveying distance, ensuring that the system matches the material's characteristics for optimal performance.
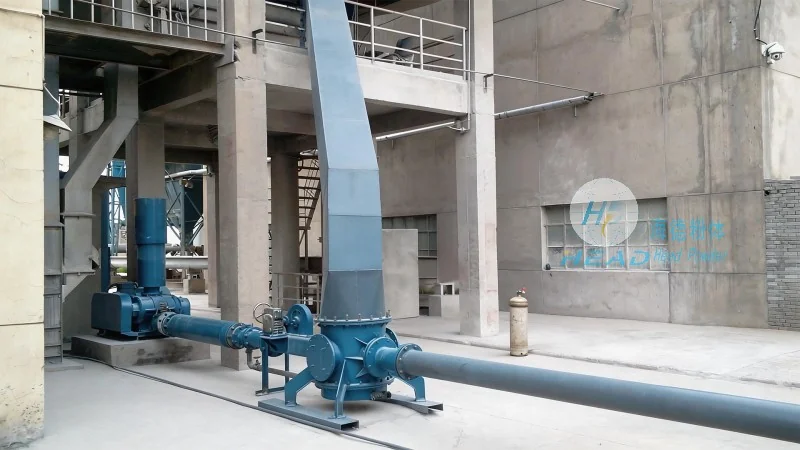
Working Scene Characteristics: Industrial and Agricultural Applications
Organic fertilizer powder conveying systems are deployed in diverse working scenes, each with distinct operational requirements. In industrial settings, such as large-scale fertilizer production facilities, these systems are integrated into automated production lines to transport raw organic materials from storage silos to mixing and granulation units. The systems must handle high volumes of material with minimal downtime, ensuring consistent feed rates to downstream processes. In agricultural applications, particularly on farms or in composting facilities, the systems are used to move organic waste or compost from collection points to spreading equipment. Here, the focus is on efficiency and adaptability to varying material conditions, such as seasonal changes in waste composition or moisture levels.
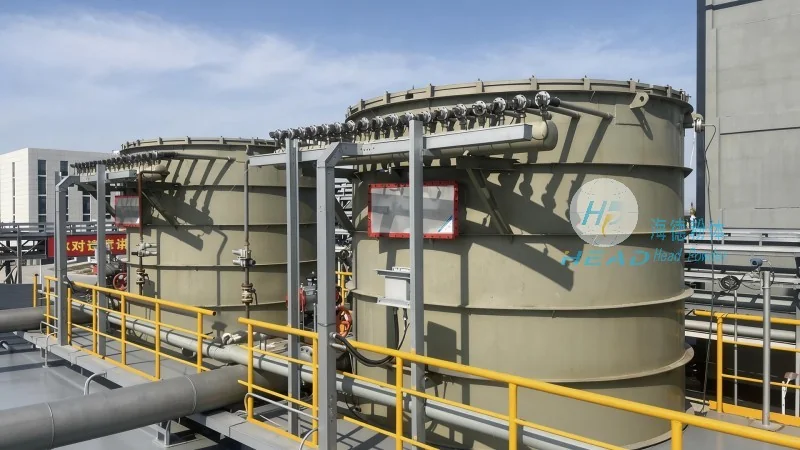
Key Features and Advantages in Real-World Scenarios
Real-world working scenes highlight several key features and advantages of organic fertilizer powder conveying systems. For example, in industrial composting plants, systems may incorporate dust control measures to comply with environmental regulations, as organic fertilizers can generate fine particles that pose air quality concerns. The systems are also designed for durability, with components like wear-resistant liners and robust motors to withstand the abrasive nature of organic materials. Additionally, many systems are equipped with monitoring and control technologies, allowing operators to adjust conveying parameters in real time based on material conditions, thereby optimizing energy consumption and reducing operational costs.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized conveying solutions, specializes in designing and manufacturing organic fertilizer powder conveying systems tailored to the needs of agricultural and industrial clients. With a focus on innovation and customer-centric engineering, the company has developed systems that address the unique challenges of organic fertilizer handling, ensuring reliability and efficiency in diverse working environments. HeadPowder's expertise lies in understanding the physical properties of organic materials and translating them into effective conveying solutions, supporting clients in optimizing their fertilizer processing and application workflows.
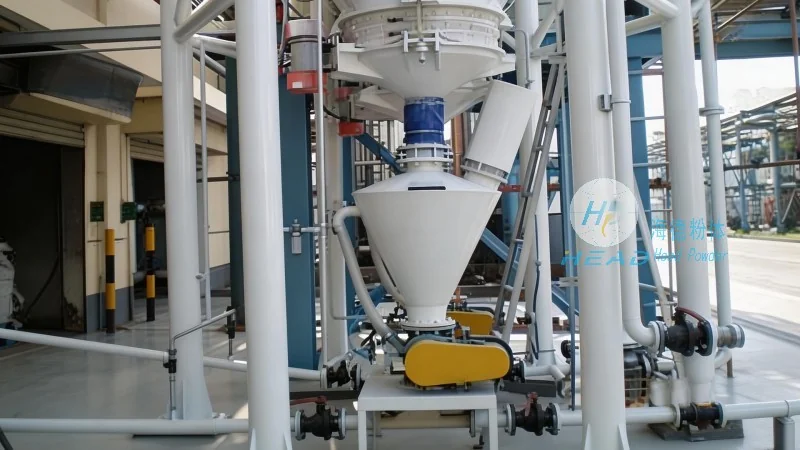
Conclusion: Enhancing Efficiency in Organic Fertilizer Handling
Organic fertilizer powder conveying systems play a vital role in modern fertilizer management, enabling efficient and sustainable handling of organic materials. By leveraging advanced principles and tailored designs, these systems address the specific challenges of organic fertilizers, from storage to application. As the demand for organic fertilizers grows, the importance of reliable conveying systems becomes increasingly evident, with companies like Shandong HeadPowder Engineering Co., Ltd. continuing to innovate and provide solutions that enhance operational efficiency and support sustainable agricultural practices.




