Multi-hopper pneumatic conveying systems represent a sophisticated approach to material handling, particularly in industries that require efficient, flexible, and reliable transport of bulk materials. At the core of this technology is the multi-hopper pump, a device engineered to handle various types of powders and granules with precision. This article delves into the concept of multi-hopper material conveying and explores the underlying design principles that make such systems effective and versatile.
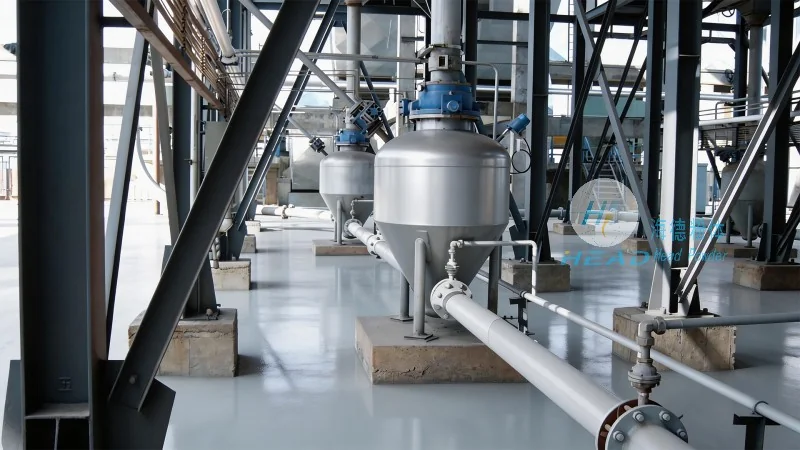
Understanding Multi-Hopper Material Conveying
Multi-hopper material conveying, often referred to as multi-hopper pneumatic conveying, is a method of transporting bulk materials through a pipeline using compressed air or other gas as the conveying medium. Unlike traditional single-hopper systems, multi-hopper configurations allow for the simultaneous or sequential loading of multiple material hoppers into a single conveying line. This capability enhances operational flexibility, enabling the system to handle different materials or product batches without the need for extensive downtime or system reconfiguration.
The system typically consists of several hoppers, each dedicated to a specific material or product. These hoppers are connected to a common pipeline, with a control system that manages the flow of material from each hopper into the conveying line. The compressed air or gas is introduced at the discharge end of the pipeline, creating a pressure differential that propels the material forward. This design allows for the efficient transport of materials over long distances, even with varying particle sizes and densities.
Key Design Principles of Multi-Hopper Systems
The effectiveness of a multi-hopper material conveying system is largely determined by its design principles, which are tailored to meet the specific requirements of the materials being handled and the operational needs of the facility. Several critical design elements contribute to the system's performance:
1. Hopper Design and Material Compatibility The hoppers in a multi-hopper system are designed to accommodate the physical and chemical properties of the materials. Factors such as particle size, moisture content, and flowability are considered to ensure that the material can be reliably loaded and conveyed without bridging, caking, or segregation. The hoppers may be equipped with agitators, vibrators, or other devices to promote material flow and prevent blockages.
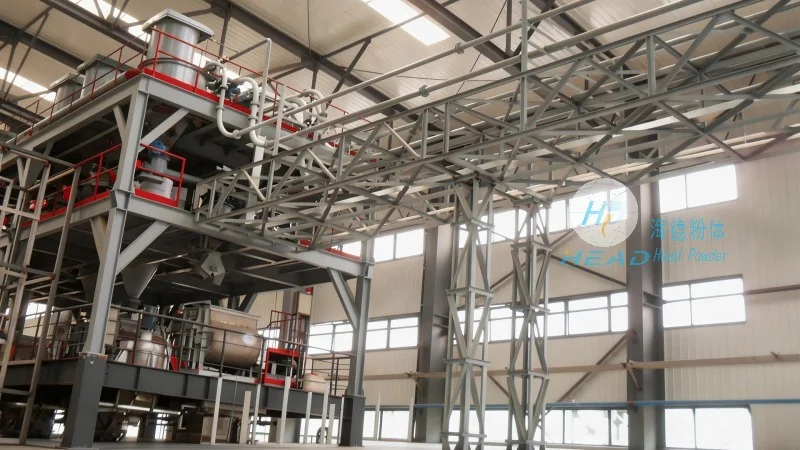
2. Conveying Line and Pressure Management The pipeline system is engineered to maintain the appropriate pressure and flow rates necessary for efficient material transport. The design of the pipeline, including the selection of pipe diameter, material, and the placement of elbows, tees, and other fittings, is crucial for minimizing pressure losses and ensuring consistent material velocity. Pressure sensors and control valves are integrated into the system to regulate the air or gas flow, maintaining optimal conveying conditions.
3. Control System and Automation Modern multi-hopper systems are equipped with advanced control systems that manage the operation of the hoppers, conveying line, and air supply. These systems use sensors to monitor material levels, pressure, and flow rates, and adjust the system parameters in real-time to maintain optimal performance. Automation reduces the need for manual intervention, enhances safety, and improves overall system efficiency.
4. Material Separation and Diverter Valves In multi-hopper configurations, it is often necessary to separate materials or direct them to different destinations. Diverter valves and separation chambers are incorporated into the system to route materials from the conveying line to the appropriate storage or processing areas. These components ensure that the correct material is delivered to the right location, preventing cross-contamination and optimizing the production process.
Applications and Benefits of Multi-Hopper Material Conveying
Multi-hopper material conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and mining. The primary benefits of these systems include:
Efficiency and Flexibility The ability to handle multiple materials or product batches simultaneously or sequentially provides significant operational flexibility. This allows facilities to adapt to changing production demands or product lines without the need for extensive system modifications.
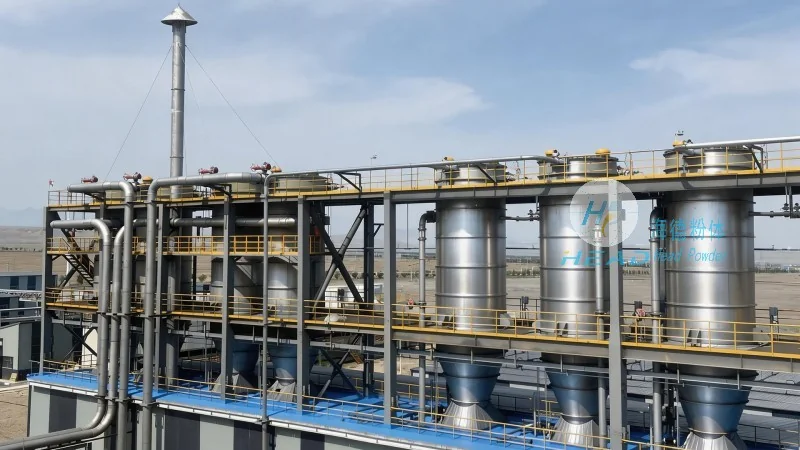
Reduced Downtime By eliminating the need to switch out hoppers or reconfigure the system for different materials, multi-hopper systems minimize downtime and improve overall productivity.
Improved Material Handling Safety Pneumatic conveying systems reduce the risk of dust explosions and material handling injuries compared to traditional methods like bucket elevators or belt conveyors. The enclosed pipeline design also prevents material loss and contamination.
Energy Efficiency Advanced control systems and optimized pipeline designs help reduce energy consumption, making multi-hopper systems more cost-effective and environmentally friendly.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of material handling equipment, including multi-hopper pneumatic conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's products are designed to meet the specific needs of various industries, ensuring reliable and efficient material transport solutions. The company's headquarters is located in Shandong, China, where it leverages its expertise and resources to develop cutting-edge technology and provide comprehensive support to its clients.




