HeadPowder, a leading enterprise in the field of material handling and processing, specializes in the development and application of pneumatic conveying systems tailored for bleaching earth. This article provides an in-depth exploration of the fundamental principles underlying pneumatic conveying technology, its practical applications in industrial settings, and the emerging trends that are shaping the future of this critical process. By understanding these aspects, industry professionals can better appreciate the efficiency, reliability, and versatility of pneumatic conveying as a solution for handling bleaching earth, a key component in various industrial processes.
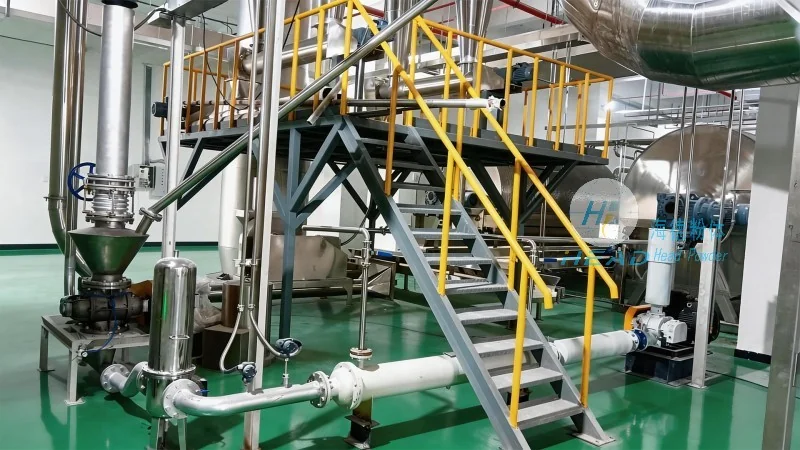
At the core of pneumatic conveying technology is the method of transporting bulk materials through a pipeline using a gas stream, typically air or other gases. The fundamental principle involves creating a pressure differential within the system, which propels the material from the source to the destination. There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at higher velocities, with particles suspended in the gas stream, while dense-phase systems use lower velocities and higher gas-to-solid ratios to move material in a more compact form. For bleaching earth, which is often a fine, powdery substance, dilute-phase systems are commonly employed due to their ability to handle fine powders efficiently and maintain low pressure differentials, reducing the risk of blockages and system wear.
The application of pneumatic conveying technology in the bleaching earth industry is widespread across various sectors. In the chemical and pharmaceutical industries, bleaching earth is used as an adsorbent to remove impurities from oils and other liquids. Pneumatic conveying enables the seamless transfer of bleaching earth from storage silos to processing units, ensuring a continuous and controlled supply. In the paper and pulp industry, bleaching earth is utilized in the deodorization and decolorization of paper stock, where the technology facilitates the precise dosing and distribution of the material. Additionally, in the food and beverage industry, bleaching earth is employed as a clarifying agent in wine and beer production, and pneumatic conveying ensures hygienic and efficient handling of the material, maintaining product quality and safety standards.
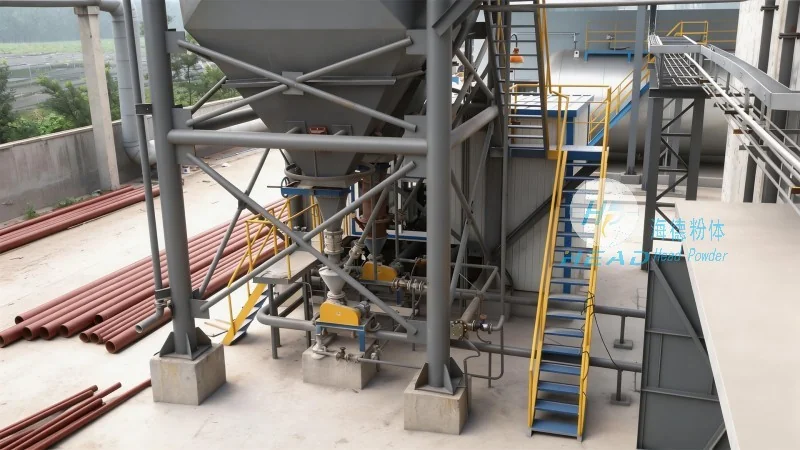
Another significant application lies in the petrochemical industry, where bleaching earth is used to refine crude oils and improve the quality of lubricating oils. The ability of pneumatic conveying systems to handle high volumes of material at a consistent rate makes them ideal for large-scale refining operations. Furthermore, in the environmental and waste management sectors, bleaching earth is used for soil remediation and water treatment, and the technology allows for the efficient transport of the material to treatment sites. The versatility of pneumatic conveying systems makes them adaptable to a wide range of industrial needs, from small-scale laboratory applications to large-scale industrial production lines.
Recent advancements in pneumatic conveying technology have focused on enhancing efficiency, reducing energy consumption, and improving system reliability. One key development is the integration of advanced control systems that optimize the flow rate and pressure within the pipeline, ensuring consistent material transport. These systems often incorporate sensors and feedback mechanisms to adjust the gas flow in real-time, minimizing energy waste and preventing system overloads. Another trend is the use of more durable and corrosion-resistant materials for pipeline components, particularly in applications involving bleaching earth, which may contain acidic or corrosive components. This reduces maintenance costs and extends the operational life of the system.
Furthermore, the adoption of sustainable practices in pneumatic conveying has gained traction. Companies are increasingly focusing on reducing the environmental impact of material handling by optimizing energy usage and minimizing emissions. For instance, the use of energy-efficient blowers and the implementation of closed-loop systems that recycle exhaust air contribute to lower carbon footprints. Additionally, the development of compact and modular conveying systems allows for easier installation and maintenance, reducing downtime and operational costs. These advancements not only improve the economic viability of pneumatic conveying but also align with global sustainability goals.
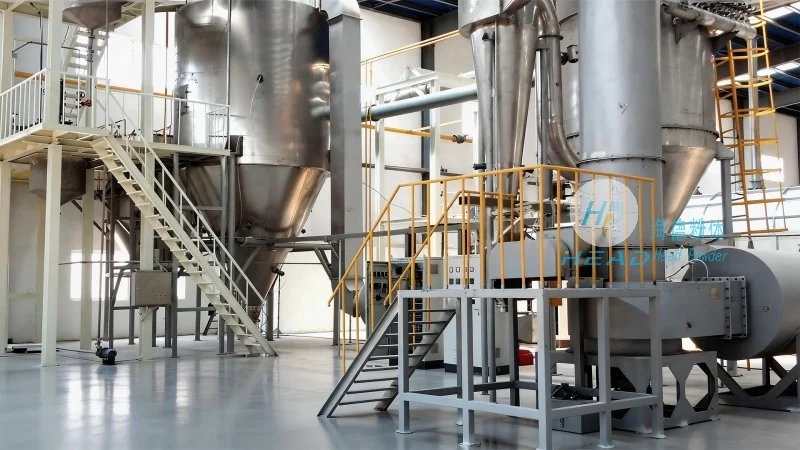
In conclusion, pneumatic conveying technology plays a vital role in the efficient and reliable handling of bleaching earth across various industries. By leveraging the fundamental principles of gas-solid flow, these systems offer a versatile and efficient solution for material transport. As technology continues to evolve, the integration of advanced control systems, durable materials, and sustainable practices will further enhance the performance and applicability of pneumatic conveying in the future. For industries relying on bleaching earth, adopting such advanced systems ensures optimal operational efficiency, product quality, and environmental responsibility.
Shandong HeadPowder Engineering Co., Ltd., with its expertise in pneumatic conveying technology, provides tailored solutions for the handling of bleaching earth. The company’s commitment to innovation and quality ensures that clients receive systems that meet their specific industrial requirements. With a focus on efficiency, reliability, and sustainability, HeadPowder continues to be a trusted partner in the material handling sector, supporting the growth and development of industries that rely on bleaching earth as a critical component.




