Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, specializes in the design and manufacturing of advanced dust collection and powder conveying systems. Our products are engineered to meet the stringent requirements of various industrial applications, ensuring efficient material handling and environmental compliance.
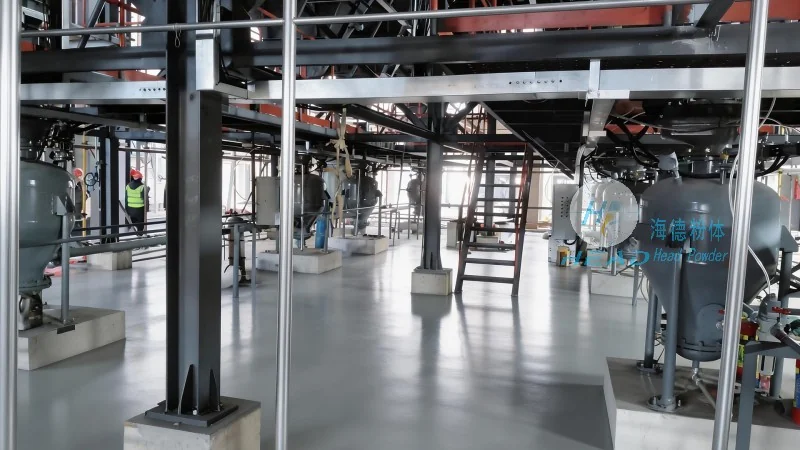
Overview of the Dust Collection Powder Conveying Line
The dust collection powder conveying line is a critical component in industrial processes that involve handling fine powders and dust. It integrates dust collection equipment with a conveying system to capture airborne particles and transport them to designated storage or processing locations. This system is essential for maintaining air quality, preventing dust pollution, and ensuring safe material handling in manufacturing facilities.
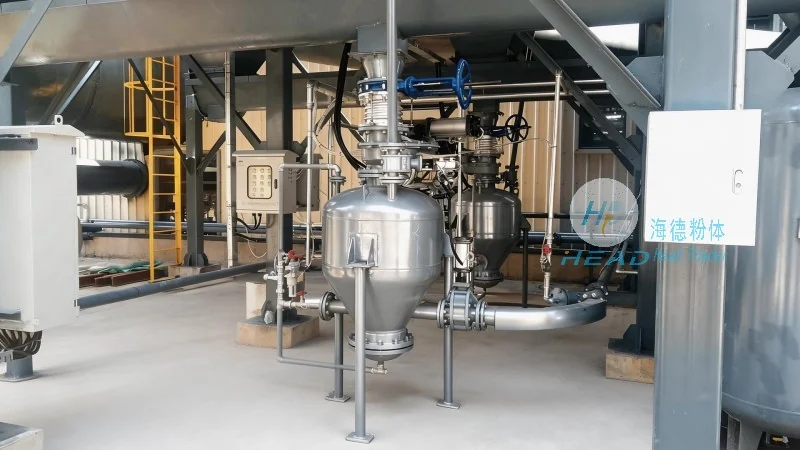
Key Components and Their Functions
The operation of the dust collection powder conveying line relies on several key components, each playing a vital role in the overall system performance. These components include dust collectors, conveyor systems (such as pneumatic or mechanical conveyors), storage tanks, and control units. The dust collector captures airborne particles, while the conveyor transports the collected powder to the storage or processing area. The control unit manages the system's operation, ensuring smooth and efficient material flow.
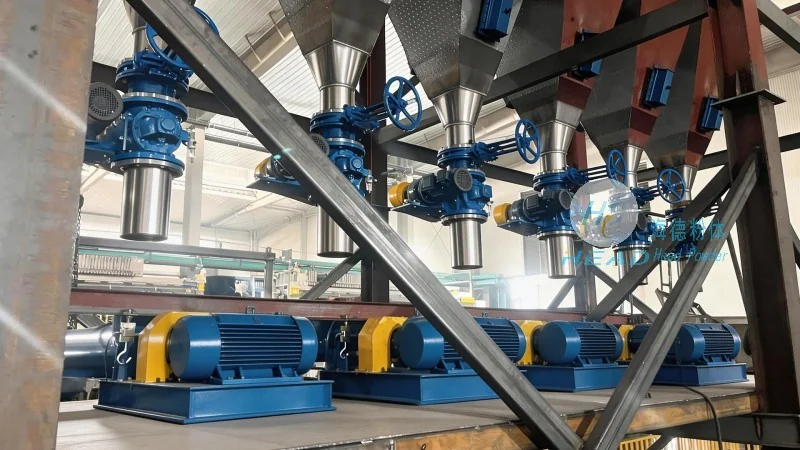
Working Principle of the Conveying Process
The working principle of the dust collection powder conveying line is based on the physical properties of powders and the principles of fluid dynamics. When material is processed, dust and fine particles are generated and become airborne. The dust collector uses mechanisms like cyclones, filters, or electrostatic precipitators to separate these particles from the air stream. The collected powder is then transferred to the conveyor system, which may use air pressure (pneumatic conveying) or mechanical force (mechanical conveying) to move the material. The system maintains a consistent pressure and flow rate to ensure reliable and continuous operation.
Operation Process: From Start to Stop
The operation process of the dust collection powder conveying line involves several sequential steps to ensure proper functioning. First, the system is started by activating the control unit, which initiates the dust collector and conveyor. The dust collector begins to capture airborne particles, and the conveyor starts moving the collected powder to the storage tank. During operation, the system continuously monitors pressure, flow rate, and other parameters to maintain optimal performance. If any issues arise, such as a blockage or pressure drop, the control unit triggers alarms or automatic shutdowns to prevent damage. The system is stopped by deactivating the control unit, which shuts down the dust collector and conveyor, allowing for maintenance or material discharge.
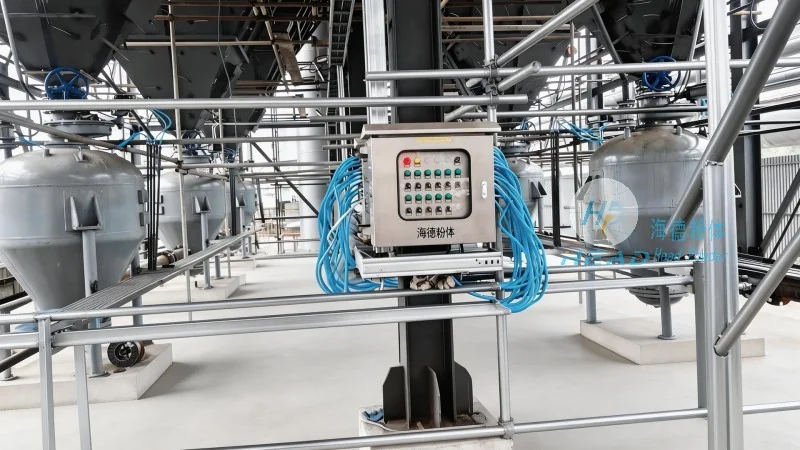
Benefits and Applications
The dust collection powder conveying line offers numerous benefits, including improved air quality, reduced dust-related health hazards, and efficient material handling. It is widely used in industries such as cement, chemical, food processing, and pharmaceuticals, where fine powders are commonly handled. The system's ability to capture and transport dust efficiently helps maintain a safe and clean working environment, while also complying with environmental regulations. By integrating dust collection with conveying, the system minimizes waste and maximizes material recovery, contributing to overall operational efficiency.




