Efficient material handling is a critical component in modern industrial operations, ensuring smooth workflow and enhanced productivity. Among the various technologies available, vacuum suction type material handling systems have emerged as a reliable solution for transporting bulk materials over short to medium distances. This article delves into the working principle and key features of such systems, providing insights into their functionality and advantages.
Introduction to Vacuum Suction Material Handling Systems
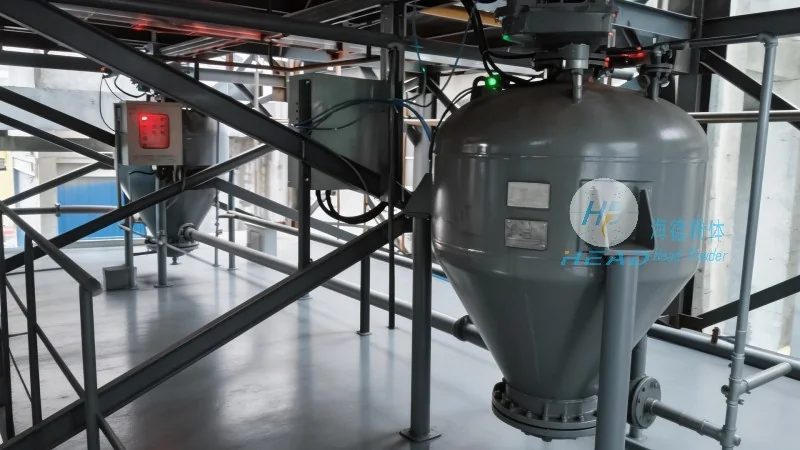
Vacuum suction material handling systems are designed to transport dry, loose materials like powders, granules, and small particles using a vacuum-generated airflow. Unlike traditional conveyor systems that rely on mechanical force, these systems utilize negative pressure to draw materials from a source to a destination. The technology is particularly suitable for applications where dust control, minimal material degradation, and flexible routing are essential. By understanding the core components and operational mechanics, users can appreciate how these systems optimize material movement in diverse industrial settings.
The Working Principle of Vacuum Suction Material Handling Systems
The operation of a vacuum suction material handling system is centered around the creation and maintenance of a negative pressure environment. The system typically consists of several key components: a vacuum pump, a network of flexible or rigid ducts, a material feed point (often equipped with a suction nozzle or hopper), and a discharge point. The vacuum pump is the heart of the system, generating the necessary suction force to pull material particles into the ductwork. As the pump operates, it reduces the pressure inside the system below atmospheric levels, creating a pressure differential that draws material from the source.
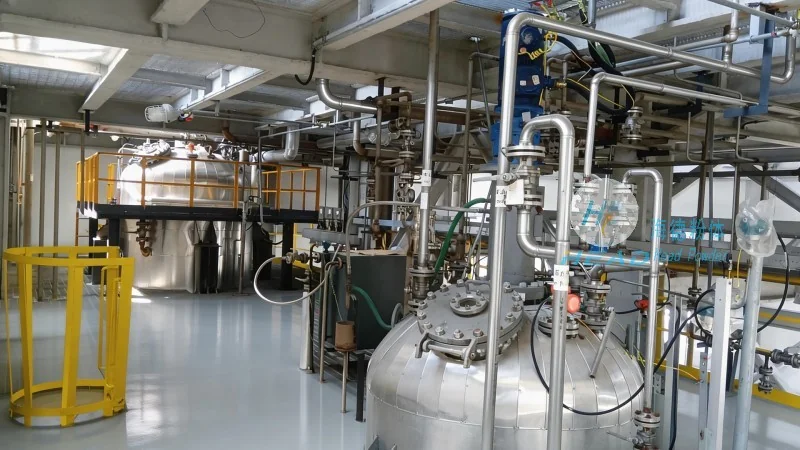
When the suction nozzle or hopper is positioned over the material to be transported, the vacuum creates an airflow that lifts the particles and pulls them into the duct. The material is then carried through the ducts to the discharge point, where the pressure is restored to atmospheric levels, allowing the material to fall out or be further processed. The system can be configured with multiple suction points and discharge points, enabling complex material routing and distribution. The control system, often integrated with the vacuum pump, allows for precise regulation of the suction pressure and flow rate, ensuring optimal performance and material handling efficiency.
Key Features and Advantages of Vacuum Suction Material Handling Systems
Vacuum suction material handling systems offer several distinct advantages that make them a preferred choice in many industries. One of the primary features is their ability to handle fine, dusty materials without generating excessive airborne particles. The enclosed ductwork and controlled airflow minimize dust dispersion, reducing health hazards and maintaining a cleaner working environment. This is particularly beneficial in applications involving hazardous or sensitive materials, where dust control is paramount.
Another notable feature is the system's flexibility in routing. The use of flexible hoses or modular ducts allows for easy reconfiguration of the material path, adapting to changes in production layouts or workflow requirements. This adaptability reduces downtime and installation costs, as the system can be repositioned without extensive modifications. Additionally, the systems are generally low in noise and vibration, contributing to a more comfortable and safer workplace.
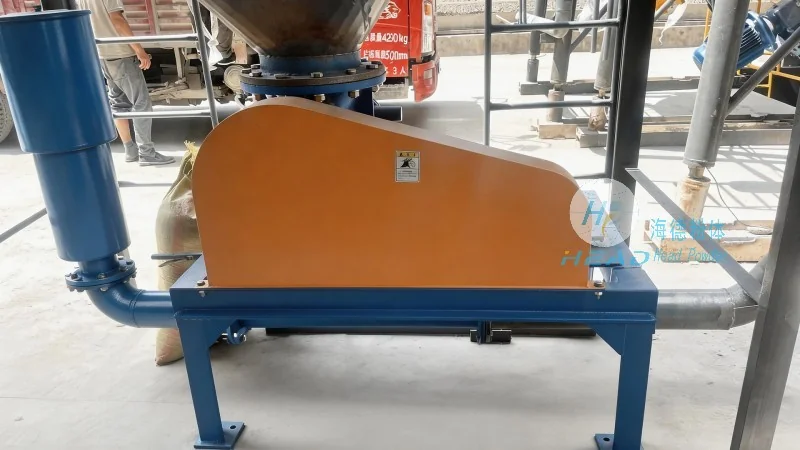
Efficiency is another key characteristic. By directly pulling material from the source, the system minimizes the need for manual handling and reduces the risk of material spillage or contamination. The consistent airflow and controlled pressure ensure a steady material flow rate, which can be adjusted to match production demands. This results in improved throughput and reduced operational costs over time. Furthermore, the vacuum suction technology is energy-efficient compared to some alternative methods, as it requires less power to operate and can be optimized for lower energy consumption.
Applications and Industries Utilizing Vacuum Suction Material Handling Systems
The versatility of vacuum suction material handling systems makes them suitable for a wide range of applications across various industries. In the pharmaceutical and food processing sectors, these systems are used to transport powders and granules while maintaining strict hygiene standards. The enclosed design and easy cleaning features ensure compliance with regulatory requirements. In the chemical industry, they handle bulk chemicals and additives, providing a safe and controlled method of material transfer.
In the agricultural sector, vacuum suction systems are employed to transport grain, seeds, and other agricultural products from storage silos to processing facilities. The gentle handling of the material minimizes breakage and ensures quality preservation. Similarly, in the construction industry, these systems are used to transport sand, cement, and other building materials to job sites, improving efficiency and reducing manual labor.
Conclusion and Company Overview
Vacuum suction material handling systems represent a sophisticated and efficient solution for material transport in modern industrial applications. Their ability to handle fine materials with minimal dust generation, combined with flexibility and energy efficiency, makes them a valuable asset for businesses seeking to optimize their operations. As the demand for reliable and sustainable material handling solutions grows, these systems continue to play a crucial role in enhancing productivity and safety across industries.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality vacuum suction material handling systems. With a focus on innovation and customer satisfaction, the company provides tailored solutions to meet the specific needs of various industries. HeadPowder's systems are engineered with precision, ensuring durability, reliability, and optimal performance. The company's commitment to quality and customer support has established it as a trusted partner for businesses seeking efficient material handling solutions. Located in Shandong, China, HeadPowder leverages advanced technology and expertise to deliver cutting-edge equipment that enhances operational efficiency and safety.




