When it comes to the efficient and reliable transportation of purified ash in industrial settings, air-pneumatic conveying equipment emerges as a critical solution. This technology, integral to modern powder handling systems, ensures the safe and effective movement of fine particulate materials like purified ash from one location to another. Understanding the structural principles behind such equipment is essential for optimizing performance and maintaining operational efficiency.
Introduction to Air-Pneumatic Conveying Systems
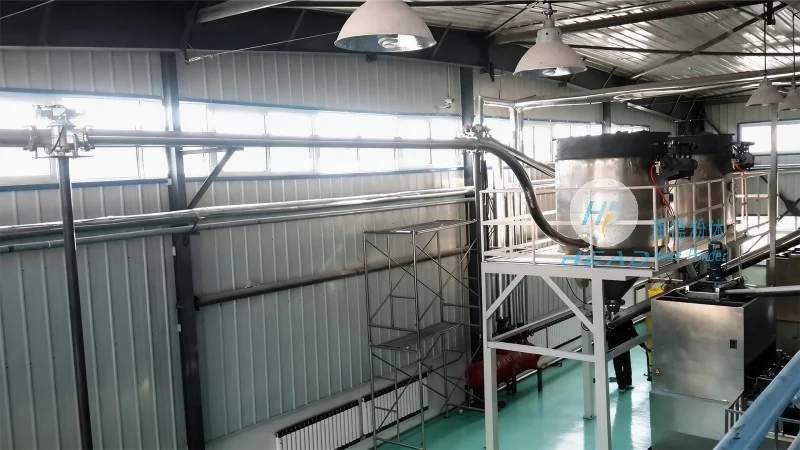
At the core of air-pneumatic conveying equipment is the principle of transporting bulk materials through a pressurized or vacuumed air stream. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and enhancing safety. The system typically consists of several key components that work in tandem to achieve efficient material transfer. These components include a feeding device, conveying pipelines, a separation system, and a discharge mechanism. Each component plays a vital role in the overall functionality of the equipment.
Structural Components and Their Functions
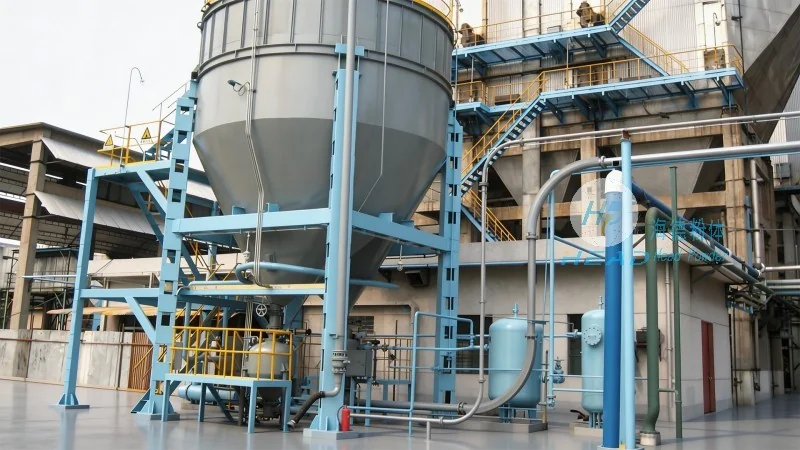
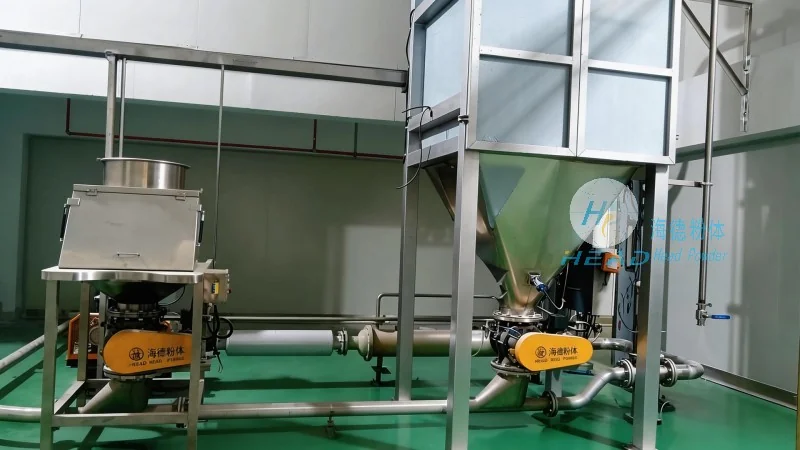
The feeding device is the entry point for the purified ash, ensuring a consistent and controlled flow of material into the conveying system. This component may include a hopper or a rotary valve to regulate the feed rate and prevent blockages. The conveying pipelines are designed to withstand the pressure and temperature conditions of the air stream and the material being transported. They are often made of materials like stainless steel or plastic to ensure durability and resistance to corrosion. The separation system is crucial for separating the air from the ash particles at the end of the conveying process. This can be achieved through cyclones, filters, or other separation technologies, ensuring that the ash is collected efficiently and the air is discharged without contamination.
HeadPowder Engineering Co., Ltd.: A Leading Provider of Powder Handling Solutions
HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of advanced air-pneumatic conveying equipment for various industrial applications. With years of experience in the field, the company has developed a comprehensive range of solutions tailored to the unique needs of clients handling purified ash and other fine powders. The company's commitment to quality and innovation has earned it a reputation as a trusted partner in the industry.
Applications and Benefits of Air-Pneumatic Conveying for Purified Ash
The use of air-pneumatic conveying equipment for purified ash offers numerous benefits, including improved safety, reduced labor costs, and enhanced process control. By eliminating the need for manual handling of ash, the system minimizes the risk of dust exposure and related health hazards. Additionally, the automated nature of the equipment allows for consistent and reliable material transfer, reducing downtime and increasing overall productivity. The compact design of the equipment also makes it suitable for installation in confined spaces, making it a versatile solution for various industrial settings.
Conclusion: The Importance of Structural Principles in Air-Pneumatic Conveying
In conclusion, air-pneumatic conveying equipment for purified ash is a sophisticated system that relies on a well-designed structure to achieve optimal performance. The integration of key components such as the feeding device, conveying pipelines, and separation system ensures efficient and safe material transfer. As a leading provider in the industry, HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality solutions that meet the evolving needs of clients. By understanding and applying the structural principles of air-pneumatic conveying, industries can enhance their operational efficiency and ensure the safe handling of purified ash.




