Understanding the mechanics and applications of synthetic rubber pneumatic conveying systems is crucial for industries dealing with bulk powders. This article provides a comprehensive overview of how these systems operate, focusing on the core principles and components that enable efficient material transport.
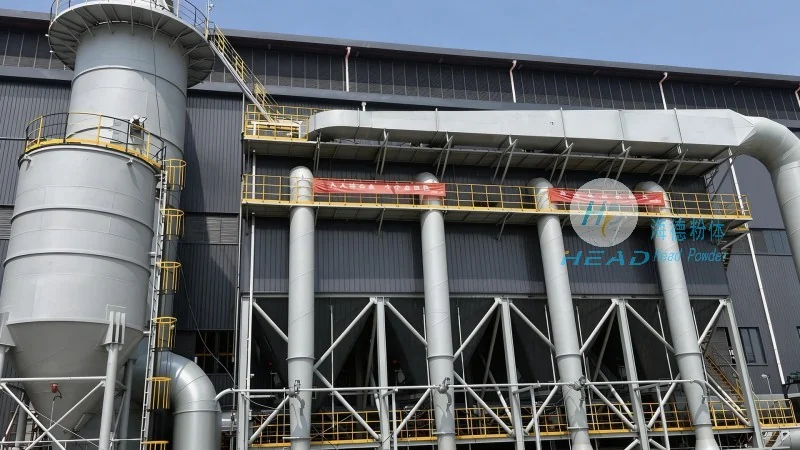
Introduction to Synthetic Rubber Pneumatic Conveying
HeadPowder, a leading provider of advanced powder handling solutions, specializes in systems that utilize synthetic rubber components for pneumatic conveying. Based in Shandong, China, the company leverages decades of expertise to design and manufacture equipment tailored to diverse industrial needs. The synthetic rubber materials used in these systems are engineered for durability, flexibility, and resistance to wear and tear, ensuring reliable performance in demanding environments.
The Working Principle of Pneumatic Conveying Systems
Pneumatic conveying systems operate by transporting bulk materials through a pipeline using air or other gases. In the case of synthetic rubber pneumatic conveying, the system integrates specialized components such as rubber hoses, fittings, and valves that facilitate smooth material movement. The process typically involves creating a pressure differential between the inlet and outlet of the system, where air is introduced to draw the powder particles into the pipeline. Synthetic rubber components are chosen for their ability to withstand the dynamic pressures and abrasion associated with powder handling, making them ideal for long-term, high-efficiency operations.
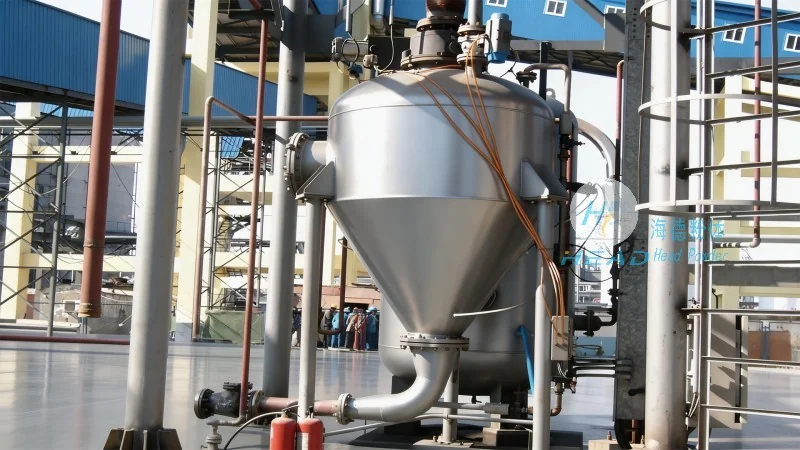
Key Components and Their Roles
Several critical components work in tandem to ensure the efficient operation of synthetic rubber pneumatic conveying systems. The primary components include the conveying line (often made of flexible synthetic rubber hoses), the air supply system (which generates the necessary pressure), and the material feed and discharge mechanisms. Rubber hoses are preferred for their flexibility and resistance to cracking or degradation under continuous use. Fittings and valves are designed to control the flow of both air and material, allowing for precise regulation of the conveying process. Additionally, the system may incorporate filters and cyclones to separate the conveyed material from the air stream, ensuring clean and efficient material recovery.
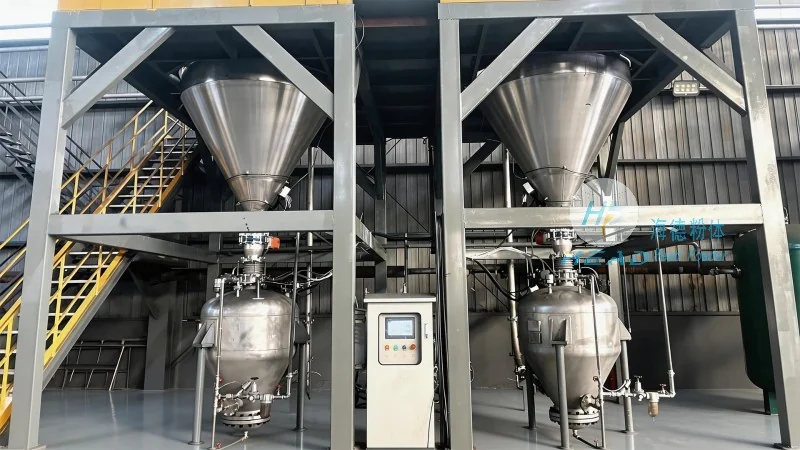
Advantages of Synthetic Rubber Pneumatic Conveying
Implementing synthetic rubber pneumatic conveying systems offers numerous benefits for industrial applications. The primary advantage is the ability to transport bulk materials over long distances with minimal maintenance. Synthetic rubber components are highly durable and resistant to abrasion, reducing the need for frequent replacements and lowering operational costs. Furthermore, these systems are compact and can be easily integrated into existing production lines, making them suitable for space-constrained environments. The flexibility of synthetic rubber hoses allows for easy routing around obstacles, enhancing the adaptability of the system to various facility layouts. Another key benefit is the reduced risk of material contamination, as the synthetic rubber components do not absorb or react with the conveyed powders, maintaining product purity.
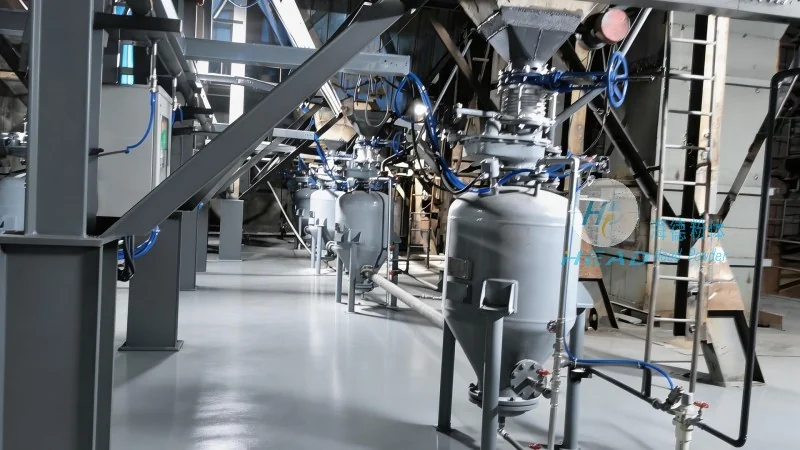
Applications in Industrial Settings
Synthetic rubber pneumatic conveying systems are widely used across various industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, these systems are essential for transporting sensitive powders while maintaining strict hygiene standards. The synthetic rubber components are non-porous and easy to clean, ensuring compliance with regulatory requirements. In food processing, the systems are used to handle ingredients such as flour, sugar, and spices, where product purity and safety are paramount. The chemical industry benefits from the system's ability to handle abrasive and corrosive powders, as the synthetic rubber materials are resistant to chemical attack. Mining operations utilize these systems to transport ore and other bulk materials from processing plants to storage facilities, leveraging the durability and efficiency of synthetic rubber components.
Conclusion and Company Expertise
Synthetic rubber pneumatic conveying systems represent a sophisticated solution for efficient bulk material transport, combining advanced materials with proven engineering principles. HeadPowder, with its headquarters in Shandong, China, continues to innovate in the field of powder handling, offering customized solutions that meet the specific needs of industrial clients. By leveraging synthetic rubber components, these systems provide reliable, low-maintenance operation and enhance overall productivity in various applications. For industries seeking to optimize their material handling processes, synthetic rubber pneumatic conveying systems from HeadPowder offer a robust and efficient solution.




