HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design, production, and supply of high-quality pneumatic conveying systems tailored for sodium dithionite applications. This equipment is engineered to ensure efficient and reliable material transport, addressing the unique handling requirements of this chemical. The following overview details the key components, structural design, and operational principles of the system, providing a comprehensive understanding of its functionality and benefits.
Company Profile and Core Capabilities
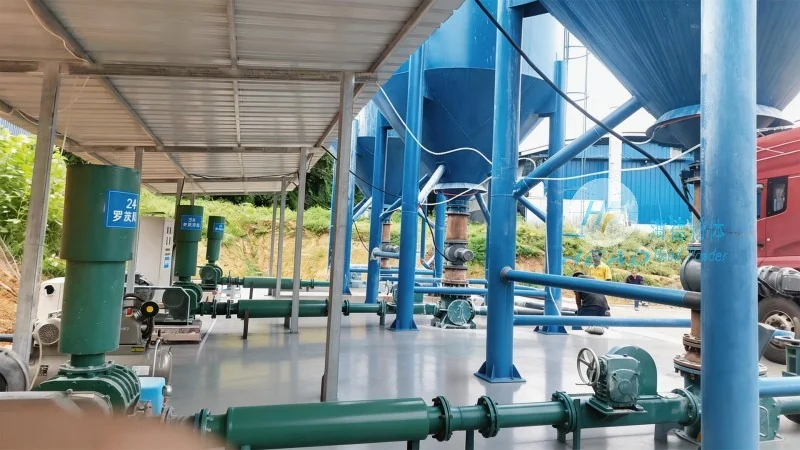
HeadPowder Engineering Co., Ltd. is a leading enterprise in the chemical processing equipment sector, with a strong focus on innovative solutions for material handling. The company is headquartered in Shandong, China, and has built a reputation for delivering robust, efficient, and cost-effective pneumatic conveying systems. Our expertise lies in customizing equipment to meet the specific needs of clients, ensuring optimal performance in diverse industrial applications. By leveraging advanced engineering and quality control measures, HeadPowder provides reliable solutions that enhance operational efficiency and safety in material transport processes.
Introduction to the Pneumatic Conveying System for Sodium Dithionite
The pneumatic conveying system designed for sodium dithionite is a specialized piece of equipment engineered to handle the material's properties, such as its granular or powdered form, and the need for controlled, dust-free transport. This system is essential for industries that rely on sodium dithionite, including the textile, paper, and chemical manufacturing sectors. The equipment is designed to minimize material degradation, prevent contamination, and ensure consistent flow rates, which are critical for maintaining product quality and process stability.
Key Structural Components and Design Features
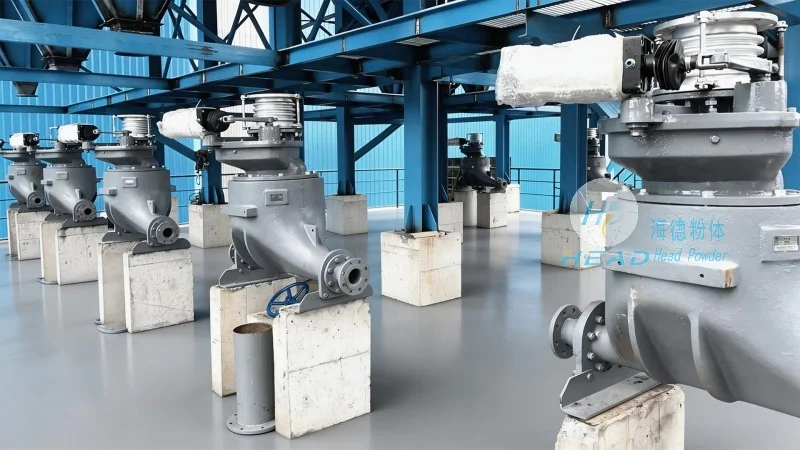
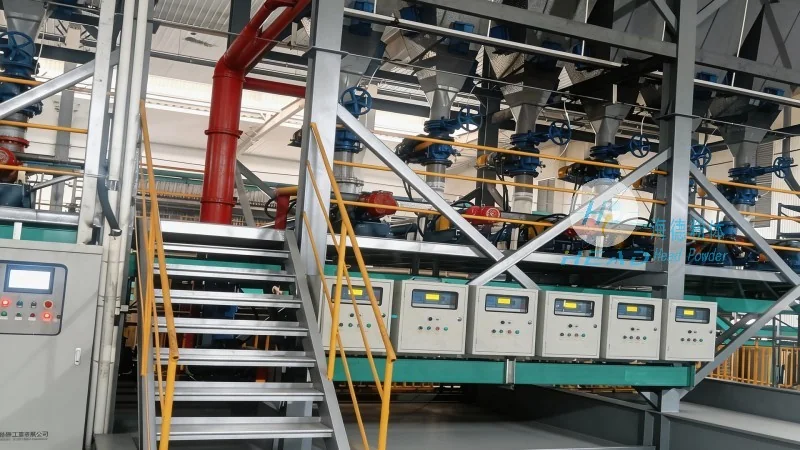
The pneumatic conveying system comprises several critical components, each playing a vital role in the overall operation. The main parts include the material feed hopper, the conveying line (typically made of stainless steel or other corrosion-resistant materials), the air compressor or blower unit, and the control system. The feed hopper is designed to store and meter the sodium dithionite, ensuring a steady supply to the conveying line. The conveying line is constructed to withstand the chemical's properties, preventing corrosion and ensuring durability. The air compressor or blower provides the necessary air pressure to move the material through the system, while the control system monitors and regulates the flow, pressure, and other operational parameters to maintain optimal performance.
Operational Principle and Working Mechanism
The system operates on the principle of pneumatic transport, where the material is suspended and transported by a stream of air. The process begins with the material being fed from the hopper into the conveying line. Simultaneously, the air compressor generates a high-pressure air stream that flows through the line, carrying the sodium dithionite particles. The air and material mixture travels through the pipeline to the discharge point, where the material is separated from the air and collected. The control system continuously monitors the pressure, flow rate, and other parameters to ensure the system operates within safe and efficient limits. This mechanism allows for a continuous, dust-free, and energy-efficient transport of sodium dithionite, reducing handling time and improving overall process efficiency.
Advantages and Benefits of the System
The pneumatic conveying system for sodium dithionite offers several advantages that make it a preferred choice for industrial applications. Firstly, it provides a dust-free and hygienic transport method, which is crucial for maintaining product quality and meeting regulatory standards. Secondly, the system minimizes material degradation and loss, as the material is handled gently and efficiently. Thirdly, it enhances operational efficiency by enabling continuous and automated material transport, reducing labor costs and improving throughput. Additionally, the system is designed for easy maintenance and cleaning, ensuring long-term reliability and low operational costs. These benefits collectively contribute to improved productivity and cost-effectiveness in the handling of sodium dithionite.
Application and Industry Relevance
The pneumatic conveying system is widely used in industries that utilize sodium dithionite as a key chemical. In the textile industry, it is used for processing and dyeing applications, where consistent material supply is essential. In the paper industry, it aids in the treatment of pulp and paper products, ensuring uniform chemical application. In the chemical manufacturing sector, it facilitates the transport of sodium dithionite in production lines, supporting efficient chemical processing. The system's adaptability and reliability make it suitable for various industrial settings, where precise and controlled material transport is required.
Quality Assurance and Technical Specifications
HeadPowder adheres to strict quality control standards to ensure the pneumatic conveying system meets the highest performance and safety requirements. The equipment is manufactured using high-quality materials, such as stainless steel, which are resistant to corrosion and chemical exposure. The system is designed to operate under specific pressure and flow rate conditions, tailored to the properties of sodium dithionite. Technical specifications include the maximum conveying capacity, air pressure requirements, and material handling capabilities. Regular maintenance and inspection are recommended to ensure the system operates at peak performance and longevity. By following these guidelines, users can maximize the system's efficiency and lifespan, ensuring reliable operation in their industrial processes.
Conclusion and Future Outlook
The pneumatic conveying system for sodium dithionite, as offered by HeadPowder Engineering Co., Ltd., represents a reliable and efficient solution for material transport in various industrial applications. By combining advanced engineering, robust design, and precise control, the system ensures optimal performance, safety, and cost-effectiveness. As industries continue to demand higher efficiency and quality in material handling, such specialized equipment plays a crucial role in meeting these requirements. HeadPowder remains committed to providing innovative solutions that enhance operational performance and support the growth of its clients in the chemical processing sector.




