Understanding the fundamentals of fertilizer pneumatic conveying is crucial for industries involved in the handling and transportation of bulk powders. This article provides a comprehensive overview of the technology, explaining how it operates and its key components. The system is designed to efficiently move granular or powdered materials like fertilizers through a pipeline using a gas stream, typically air or a combination of air and other gases.
What is Pneumatic Conveying?
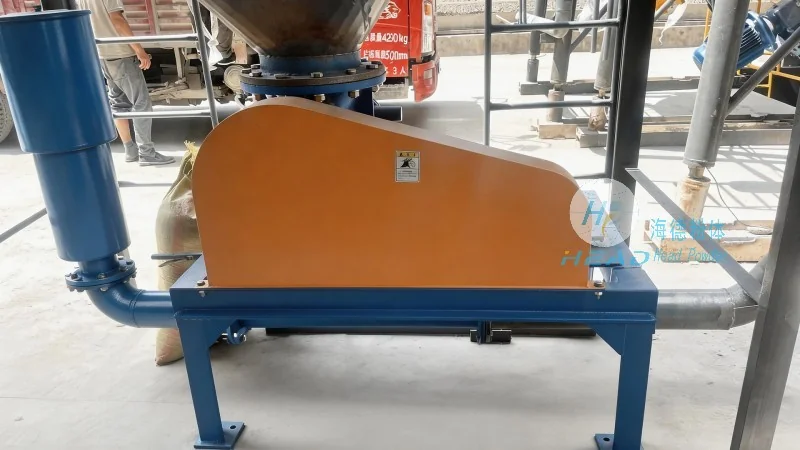
Pneumatic conveying, also known as powder handling systems, is a method of transporting bulk materials through a pipeline by utilizing a moving gas stream. In the context of fertilizer handling, this technology is widely used due to its ability to handle abrasive and dusty materials with minimal wear and tear on equipment. The process involves creating a pressure differential within the system, which propels the material from the source to the destination.
The Working Principle of Fertilizer Pneumatic Conveying Systems
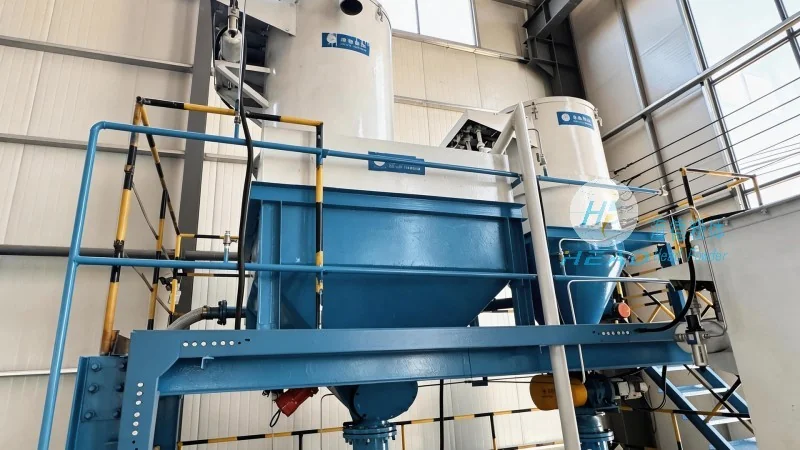
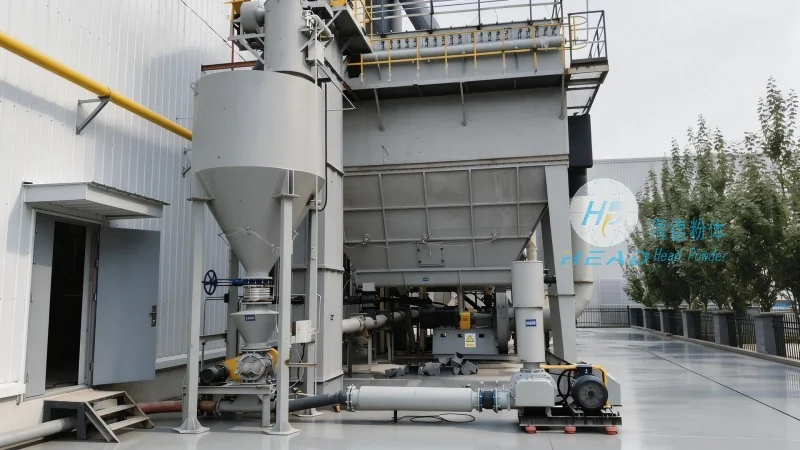
The core of a fertilizer pneumatic conveying system lies in its ability to combine the material with a gas stream, forming a dense or dilute phase flow. The system typically consists of several key components, including a material feeder, a conveying pipeline, a separation unit, and a gas source. The material feeder, often a rotary valve or a star feeder, ensures a consistent flow of fertilizer into the system. The conveying pipeline, made of materials resistant to corrosion and abrasion, transports the material and gas mixture. The separation unit, such as a cyclone or a bag filter, separates the material from the gas stream, allowing the gas to be recycled or vented. The gas source, usually a blower or a compressor, provides the necessary pressure and flow rate to move the material through the system.
Types of Pneumatic Conveying Systems
There are two main types of pneumatic conveying systems used in fertilizer handling: dilute phase and dense phase. Dilute phase systems operate at low material concentrations, typically 1-10% by volume, and are suitable for long-distance transportation and high-speed applications. Dense phase systems, on the other hand, operate at higher material concentrations, around 10-30% by volume, and are ideal for short-distance transportation and applications requiring gentle handling of the material. The choice between these systems depends on factors such as the distance between the source and destination, the material characteristics, and the required flow rate.
Advantages of Fertilizer Pneumatic Conveying
Implementing a pneumatic conveying system for fertilizer transportation offers several advantages. Firstly, it provides a closed system, which helps in controlling dust emissions and maintaining a clean working environment. This is particularly important in industries where dust can be a health hazard or cause environmental issues. Secondly, the system is highly efficient in terms of energy consumption and material handling, as it eliminates the need for manual labor and reduces the risk of material spillage. Thirdly, the technology is versatile and can handle a wide range of fertilizer types, including granular, powdered, and even wet materials. This flexibility makes it suitable for various applications in the agricultural and chemical industries.
Applications in the Fertilizer Industry
Fertilizer pneumatic conveying systems are widely used in various stages of the fertilizer production and distribution process. In the manufacturing plant, the system can be used to transport raw materials from storage silos to processing units. During the packaging stage, it helps in moving finished fertilizer products from the production line to storage or loading areas. Additionally, the system is used in bulk handling facilities to transport large quantities of fertilizer from the plant to distribution centers or directly to farms. The ability to handle high volumes of material efficiently makes it an essential component in modern fertilizer handling operations.
HeadPowder Engineering Co., Ltd. and Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of powder handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems for the fertilizer industry. With years of experience in the field, the company has developed advanced technologies and equipment that meet the specific needs of fertilizer manufacturers. HeadPowder's systems are engineered to ensure high efficiency, low maintenance, and long service life, providing reliable performance in demanding industrial environments. The company's expertise in material handling and process engineering enables it to offer tailored solutions that optimize the entire fertilizer handling process, from raw material intake to final product delivery.
Conclusion
Fertilizer pneumatic conveying is a sophisticated and efficient method of transporting bulk materials, offering numerous benefits over traditional handling methods. By understanding the working principles and components of such systems, industries can make informed decisions about implementing this technology to improve their operational efficiency and product quality. As a trusted partner in the field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide cutting-edge solutions that meet the evolving needs of the fertilizer industry.




