HeadPowder, a leading provider of industrial conveying solutions, specializes in the design and manufacturing of cement gray pneumatic conveying systems. This article provides a comprehensive overview of the system's structure and operational principles, highlighting its efficiency and reliability in handling cement gray materials.
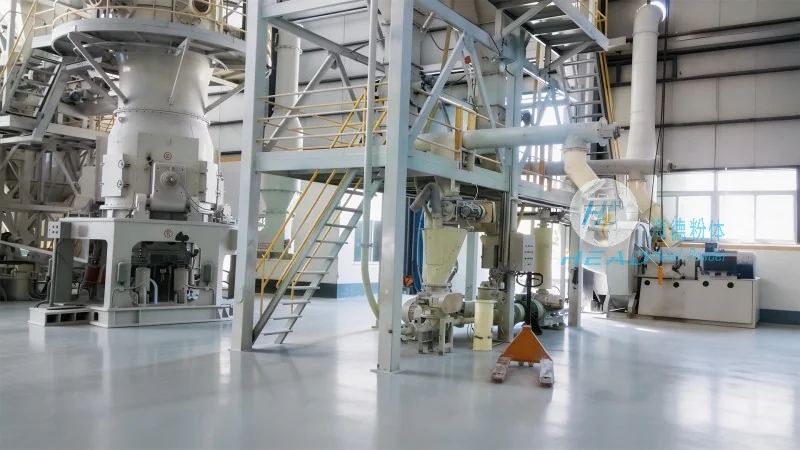
Overview of the Cement Gray Pneumatic Conveying System
The cement gray pneumatic conveying system is engineered to transport bulk materials like cement gray efficiently and safely. HeadPowder's system integrates advanced components that ensure smooth material flow, minimal downtime, and optimal performance. The system is tailored to meet the specific demands of cement gray handling, offering a cost-effective solution for various industrial applications.
Key Structural Components and Their Functions
The cement gray pneumatic conveying system consists of several critical components, each playing a vital role in the overall operation. These components include the material feeding unit, conveying pipeline, air supply system, separation and collection unit, and control panel. Each part is designed to work in harmony to ensure consistent and reliable material transport.
Material Feeding Unit
The material feeding unit is responsible for introducing the cement gray into the system. It typically includes a hopper or feeder that can handle bulk quantities of material. The design ensures that the material is fed uniformly into the conveying pipeline, preventing blockages and ensuring consistent flow rates. The feeding unit is equipped with adjustable valves and sensors to control the material input rate, adapting to varying production needs.
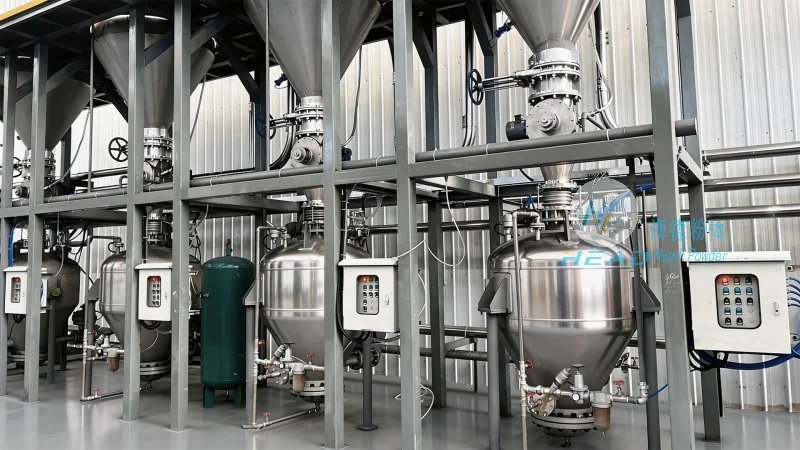
Conveying Pipeline
The conveying pipeline is the core of the system, responsible for transporting the cement gray from the feeding unit to the destination. The pipeline is made of durable materials, such as stainless steel or high-density polyethylene, to withstand the abrasive nature of cement gray. The design includes bends and elbows that are carefully engineered to minimize pressure loss and maintain efficient material flow. The pipeline is also equipped with pressure sensors and flow meters to monitor the system's performance in real-time.
Air Supply System
The air supply system provides the necessary pressure and volume of air to move the cement gray through the pipeline. It typically consists of a blower or compressor, air filters, and a control valve. The system is designed to deliver a consistent airflow, ensuring that the material is conveyed at the desired speed. The air supply unit is equipped with safety features, such as pressure relief valves, to prevent over-pressurization and ensure safe operation.
Separation and Collection Unit
The separation and collection unit is responsible for separating the cement gray from the air and collecting it at the destination. It typically includes a cyclone separator or a baghouse filter. The cyclone separator uses centrifugal force to separate the material from the air, while the baghouse filter captures fine particles. The collected material is then discharged into a storage bin or silo. The unit is equipped with dust collection systems to ensure compliance with environmental regulations and maintain a clean working environment.
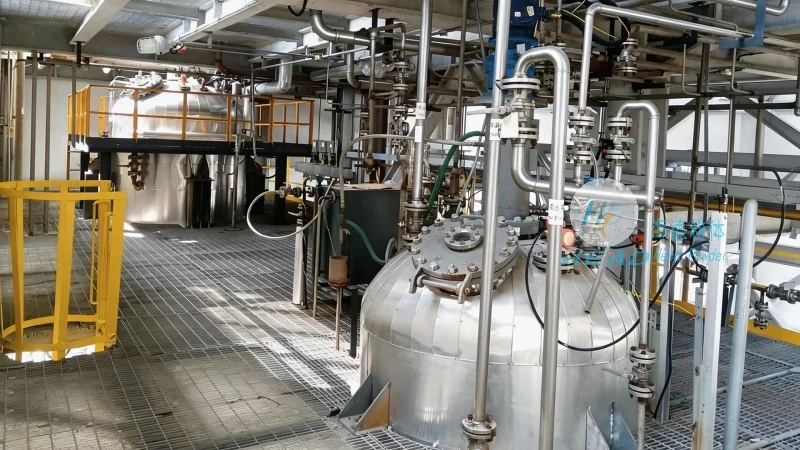
Control Panel and Automation
The control panel is the brain of the system, responsible for monitoring and controlling all components. It includes sensors, indicators, and control buttons that allow operators to adjust the system's parameters. The system can be equipped with automation features, such as PLC (Programmable Logic Controller) control, to enhance efficiency and reduce human intervention. The control panel provides real-time data on system performance, including pressure, flow rate, and material level, enabling operators to make informed decisions and optimize the system's operation.
Working Principle of the Cement Gray Pneumatic Conveying System
The working principle of the cement gray pneumatic conveying system involves the use of air to transport the material. The system operates by creating a pressure difference between the feeding unit and the destination. The air is supplied at a high pressure, which forces the cement gray into the pipeline. The material is then carried by the air flow, moving through the pipeline to the collection unit. The air and material are separated at the destination, and the air is either recycled or released into the atmosphere. The system's efficiency depends on the proper balance of air pressure, material feed rate, and pipeline design.
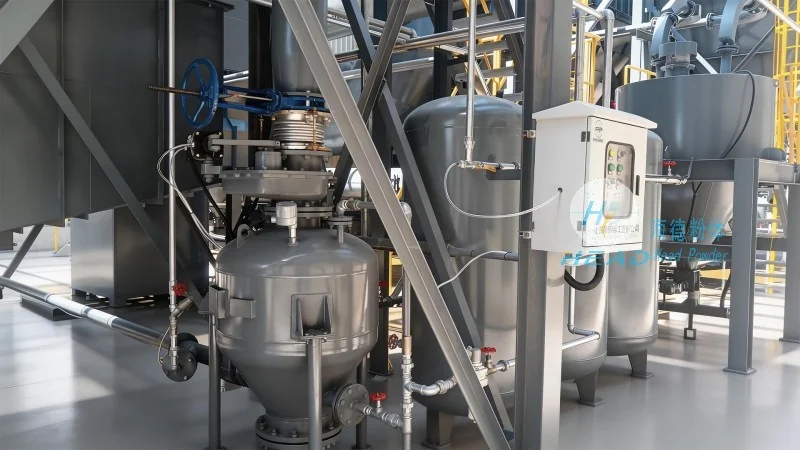
Advantages of Using a Cement Gray Pneumatic Conveying System
HeadPowder's cement gray pneumatic conveying system offers several advantages over traditional conveying methods. The system is highly efficient, as it can transport large quantities of material over long distances with minimal energy consumption. It is also flexible, as it can be easily adjusted to handle different material types and flow rates. The system is also safe and reliable, as it eliminates the need for manual handling of bulk materials, reducing the risk of accidents and injuries. Additionally, the system is compact and requires less space compared to traditional methods, making it suitable for various industrial settings.
Applications of the Cement Gray Pneumatic Conveying System
The cement gray pneumatic conveying system is widely used in various industries, including cement production, construction, and chemical processing. It is particularly suitable for applications where the material needs to be transported from a storage silo to a processing unit or from one production line to another. The system is also used in applications where the material needs to be conveyed over long distances or through complex layouts. HeadPowder's system has been successfully implemented in numerous industrial projects, providing reliable and efficient material transport solutions.
Conclusion
HeadPowder's cement gray pneumatic conveying system is a reliable and efficient solution for handling bulk cement gray materials. The system's advanced design and components ensure optimal performance, minimal downtime, and cost-effective operation. With its flexibility and adaptability, the system can be tailored to meet the specific needs of various industrial applications. HeadPowder, with its expertise in industrial conveying solutions, continues to provide high-quality systems that meet the evolving demands of the industry.




