HeadPowder, a leading enterprise in the field of chemical processing equipment, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems. This article provides a detailed overview of the operation process and working principle of the sodium hexafluorophosphate pneumatic conveying system equipment, highlighting its key components, operational workflow, and technical advantages.
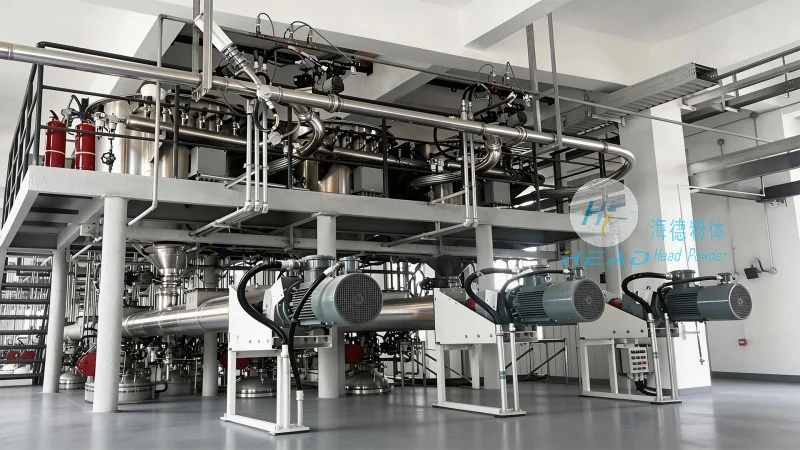
Overview of the Sodium Hexafluorophosphate Pneumatic Conveying System
The sodium hexafluorophosphate pneumatic conveying system is a sophisticated piece of industrial equipment engineered to efficiently transport sodium hexafluorophosphate—a critical chemical compound used in various applications such as lithium-ion battery production, pharmaceuticals, and specialty chemicals—through a closed pipeline system using air or other gas as the conveying medium. This system is designed to ensure safe, reliable, and low-dust operation, minimizing material loss and environmental impact.
Key Components of the Pneumatic Conveying System
The system consists of several core components that work in tandem to achieve effective material transport. These include a hopper for material storage, a feeder to control the flow of sodium hexafluorophosphate into the system, a venturi or airlock for creating the necessary pressure differential, a pipeline network for conveying the material, and a receiver or silo for depositing the material at the destination. Each component plays a crucial role in maintaining the system's efficiency and safety.
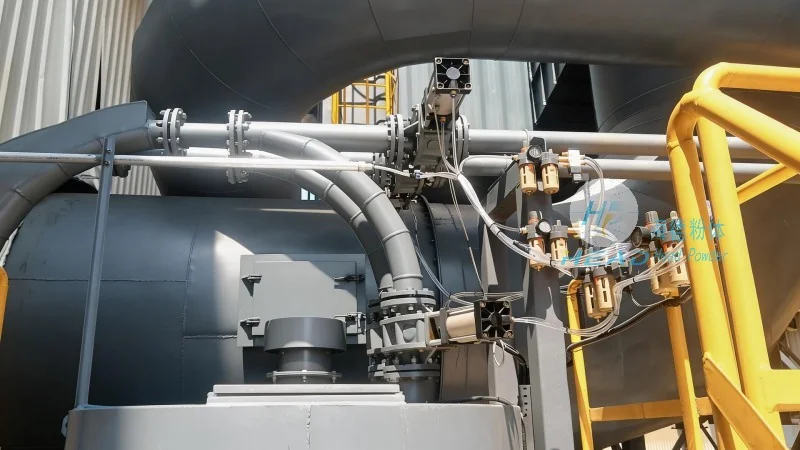
Working Principle of the Pneumatic Conveying System
The operation of the sodium hexafluorophosphate pneumatic conveying system is based on the principle of pneumatic transport, where the material is suspended and carried by a high-velocity air stream. The process typically begins with the material being fed from the hopper into the feeder. The feeder regulates the flow rate, ensuring a consistent supply of sodium hexafluorophosphate into the system. Simultaneously, the air compressor or blower generates a high-pressure air flow that enters the venturi or airlock. This creates a pressure differential that draws the material from the feeder into the pipeline. The air stream then carries the material through the pipeline network, maintaining the material in a suspended state to prevent clogging or blockages. At the receiving end, the air stream slows down, allowing the material to settle into the receiver or silo. The air is then filtered and recycled back into the system, completing the cycle.
Operation Process of the System
The operation process of the sodium hexafluorophosphate pneumatic conveying system involves several sequential steps. First, the system is prepared by ensuring that all components are properly connected and the air compressor is operational. Next, the material is loaded into the hopper. The feeder is then activated to start the material flow into the system. The air compressor is turned on, generating the necessary air pressure to initiate the conveying process. As the material is fed into the pipeline, it is carried by the air stream to the receiving location. The system continues to operate until the material is fully transferred. Finally, the system is shut down, and the air is filtered and recycled. This process is designed to be automated, with controls that monitor pressure, flow rate, and material level to ensure optimal performance and safety.
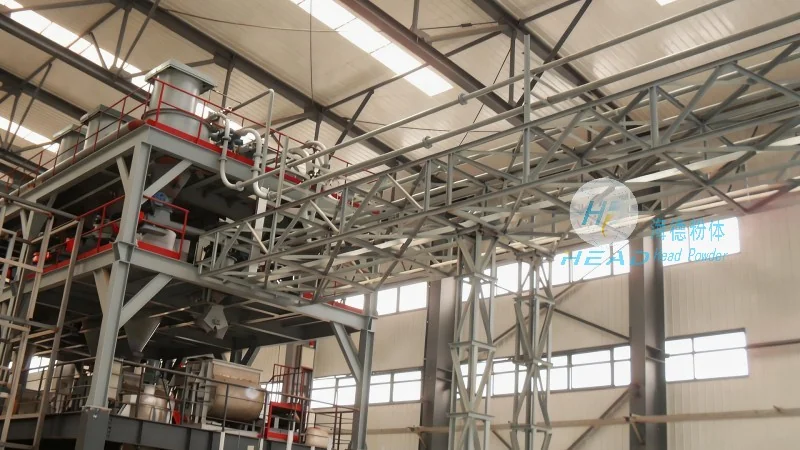
Technical Advantages and Benefits
The sodium hexafluorophosphate pneumatic conveying system offers several technical advantages that make it an ideal choice for industrial applications. These include high efficiency in material transport, with minimal material loss and low dust generation, which enhances safety and environmental compliance. The system also provides flexibility in terms of material handling, allowing for the transport of various particle sizes and moisture content. Additionally, the closed pipeline system reduces the risk of contamination and exposure to hazardous materials, ensuring a safe working environment. The system's compact design and low maintenance requirements also contribute to its cost-effectiveness and reliability.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a professional manufacturer and supplier of chemical processing equipment. With years of experience in the industry, the company specializes in the design and production of pneumatic conveying systems, as well as other related equipment such as mixers, dryers, and reactors. HeadPowder is committed to providing high-quality, reliable equipment that meets the diverse needs of its clients. The company adheres to strict quality control standards and offers comprehensive after-sales support to ensure customer satisfaction.




