For industrial facilities dealing with ash and dust removal, the pneumatic ash handling system is a critical component in maintaining operational efficiency and environmental compliance. This system, also known as a pneumatic conveying system for ash, is designed to transport ash from its source to disposal or treatment locations using air pressure. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of such systems, ensuring reliable and efficient ash management solutions.
Purpose and Importance of Pneumatic Ash Handling Systems
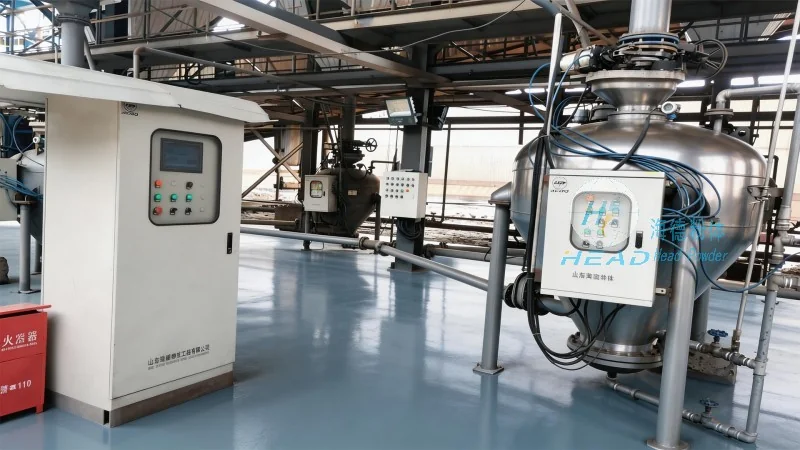
In industrial processes such as power generation, cement production, and waste incineration, large volumes of ash are generated. Traditional methods of ash handling, like bucket elevators or belt conveyors, often face challenges related to maintenance, material buildup, and limited flexibility. Pneumatic ash handling systems address these issues by offering a flexible, low-maintenance solution that can handle various ash types and transport them over long distances with minimal disruption to the main process. The system's ability to maintain a closed loop, preventing dust emissions, is also a significant advantage, aligning with environmental regulations and improving workplace safety.
Core Components and Structure of the Pneumatic Ash Handling System
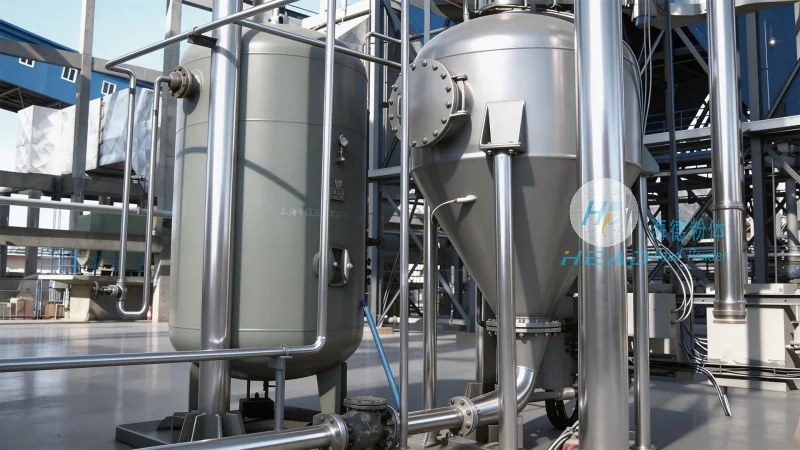
The pneumatic ash handling system consists of several key components that work in tandem to achieve efficient ash transport. The primary components include the ash feeder, which feeds ash into the system; the conveying pipeline, which transports the ash; the air compressor or blower, which provides the necessary air pressure; and the control system, which regulates the operation of the entire system. The ash feeder is typically a rotary valve or a screw feeder that ensures a consistent flow of ash into the pipeline. The conveying pipeline is made of materials resistant to ash abrasion and corrosion, such as stainless steel or special alloys. The air compressor or blower generates the air pressure required to move the ash particles through the pipeline. The control system monitors and adjusts the air pressure, flow rate, and ash feed rate to maintain optimal performance. Additionally, the system may include dust collectors and filters to capture any fine particles that escape the pipeline, ensuring that the environment is not contaminated.
Working Principle of the Pneumatic Ash Handling System
The operation of the pneumatic ash handling system is based on the principle of pneumatic conveying, where ash particles are suspended in a stream of air and transported through the pipeline. The process begins with the ash feeder delivering ash into the pipeline. The air compressor then generates a high-pressure air stream that flows through the pipeline, carrying the ash particles along with it. As the air and ash mixture moves through the pipeline, the ash particles are kept in suspension by the air flow. The system may use different conveying modes, such as dilute phase or dense phase, depending on the ash characteristics and distance to be covered. In dilute phase conveying, the ash is mixed with a large volume of air, allowing for high-speed transport over long distances. In dense phase conveying, the ash is conveyed in a more concentrated form, which is suitable for shorter distances or when higher pressure is required. The system's control system continuously monitors the pressure and flow rates to ensure that the ash is transported efficiently and without blockages. At the receiving end, the ash is separated from the air stream using a separator or cyclone, and the ash is collected in a hopper or storage bin. The air, now free of ash particles, is then filtered and returned to the system or released into the atmosphere.
Advantages of Using Pneumatic Ash Handling Systems
Compared to traditional ash handling methods, pneumatic ash handling systems offer several advantages. First, they provide a flexible and compact solution that can be easily integrated into existing industrial facilities. The system's components are modular, allowing for easy expansion or modification as the facility's needs change. Second, the system is low-maintenance, as there are fewer moving parts compared to traditional conveyors. The air compressor and feeder are the main components that require regular maintenance, and the system's design minimizes the risk of material buildup and blockages. Third, the system is highly efficient in terms of energy consumption, as it uses less energy to transport ash compared to other methods. The air pressure required is relatively low, and the system's operation is continuous, reducing the need for frequent stops and starts. Fourth, the system is environmentally friendly, as it maintains a closed loop and prevents dust emissions. The dust collectors and filters ensure that the air released into the atmosphere is clean, and the system's design minimizes the risk of environmental contamination. Finally, the system is safe to operate, as it eliminates the need for manual handling of ash, reducing the risk of accidents and injuries.
Applications and Industries Using Pneumatic Ash Handling Systems
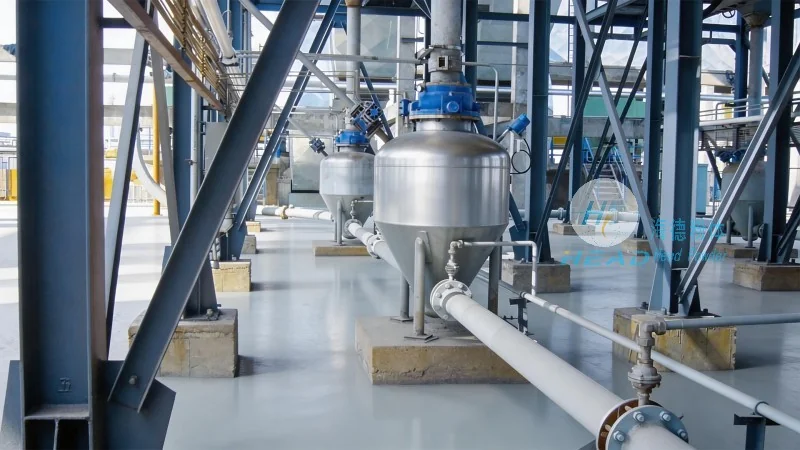
Pneumatic ash handling systems are used in a wide range of industries, including power generation, cement production, waste incineration, and chemical processing. In power generation, the system is used to transport ash from coal-fired power plants to disposal sites or to re-use it as a raw material in cement production. In cement production, the system is used to transport ash from the kiln to the clinker storage or to the cement grinding plant. In waste incineration, the system is used to transport ash from the incinerator to the disposal site or to the recycling facility. In chemical processing, the system is used to transport ash from the reactors to the storage or treatment facilities. The system's flexibility and efficiency make it suitable for various applications, and its ability to handle different ash types and transport them over long distances makes it a preferred choice for many industrial facilities.
Conclusion and Company Overview
Pneumatic ash handling systems are an essential component in modern industrial facilities, providing efficient and reliable ash management solutions. The system's ability to transport ash over long distances, maintain a closed loop, and prevent dust emissions makes it a preferred choice for many industries. Shandong HeadPowder Engineering Co., Ltd. is a leading provider of such systems, with years of experience in designing, manufacturing, and installing high-quality pneumatic ash handling systems. The company's commitment to quality and customer satisfaction has made it a trusted partner for many industrial facilities. With its advanced technology and professional team, Shandong HeadPowder Engineering Co., Ltd. continues to provide innovative solutions for ash handling, helping industrial facilities improve their operational efficiency and environmental performance.




