Pharmaceutical pneumatic conveying systems represent a critical technology in the manufacturing and handling of drug products. These systems are designed to transport powders and granules efficiently and hygienically, meeting the stringent requirements of the pharmaceutical industry. Understanding the structural principles and operational mechanisms of such systems is essential for optimizing production processes and ensuring product quality. This article provides an overview of pharmaceutical pneumatic conveying, focusing on its structural components, working principles, and the expertise of Shandong HeadPowder Engineering Co., Ltd. in delivering tailored solutions.
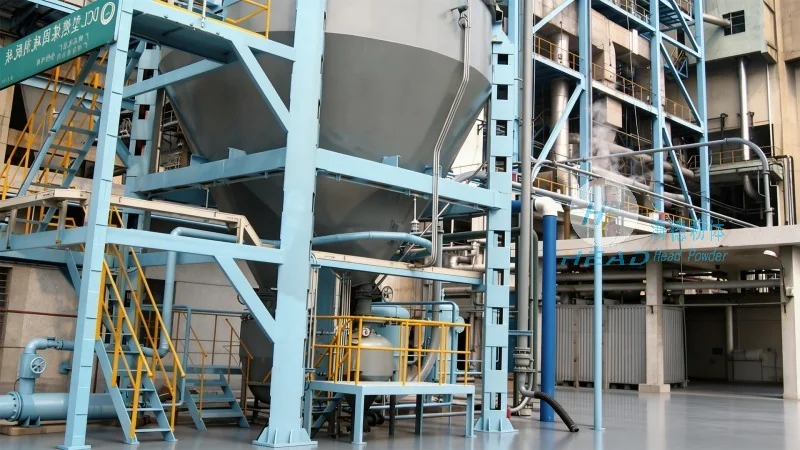
Structural Components and Working Principles of Pneumatic Conveying Systems
Pneumatic conveying systems in pharmaceutical applications typically consist of several key components that work in concert to move materials. The primary components include a material feed device, a conveying line (usually made of stainless steel to ensure hygiene), a separation unit, and a dust collection system. The feed device, often a rotary valve or a venturi feeder, introduces the powder into the system under controlled conditions. The conveying line may operate under either positive pressure (where air is forced through the line) or negative pressure (where air is drawn out), depending on the system design and the material being transported. The separation unit, such as a cyclone or a bag filter, separates the conveyed material from the air stream, ensuring that the product remains clean and free from contamination. The dust collection system then captures any residual particles, maintaining a safe and compliant environment.
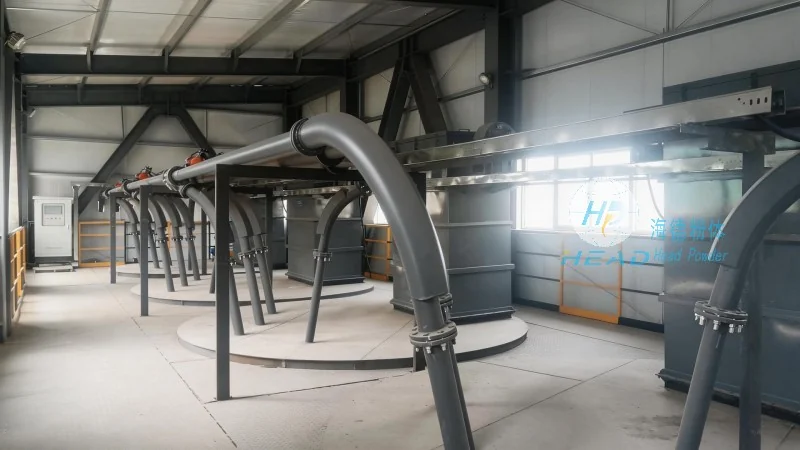
The working principle of a pneumatic conveying system involves the creation of a flow of air that propels the material through the conveying line. In positive pressure systems, a blower or compressor generates the necessary air pressure, which is introduced at the feed point. The material is then entrained by the air and carried along the pipeline. In negative pressure systems, a vacuum pump creates a low-pressure environment at the discharge end, drawing the material and air through the line. Both systems rely on the balance of air velocity and material density to achieve effective transport. The design of the system, including the size of the conveying line, the type of feed device, and the separation equipment, is critical to ensuring efficient and reliable operation.
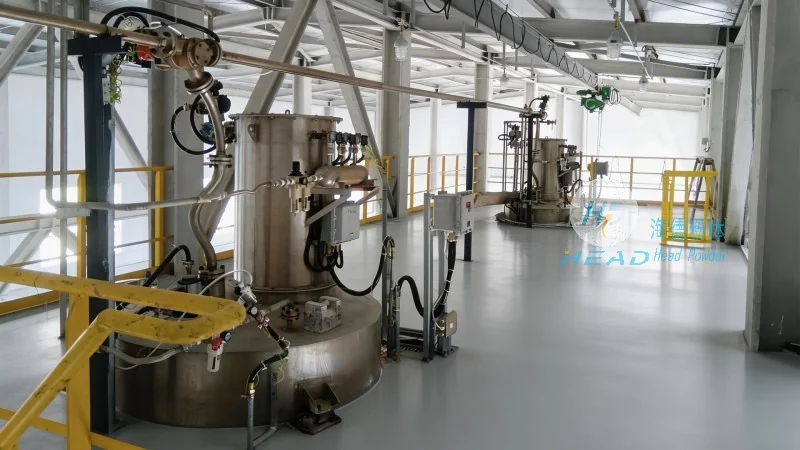
HeadPowder Engineering Co., Ltd.: Expertise in Pharmaceutical Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of engineering solutions for the pharmaceutical industry. With its headquarters in Shandong, China, the company specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the unique needs of pharmaceutical manufacturers. HeadPowder's expertise lies in understanding the specific challenges of drug product handling, such as maintaining sterility, preventing cross-contamination, and ensuring compliance with regulatory standards like GMP (Good Manufacturing Practice). The company's team of engineers and technicians work closely with clients to develop customized solutions that address their production requirements, whether it involves bulk material handling, powder transfer between processing units, or integration with existing manufacturing lines.
HeadPowder's commitment to quality and innovation is reflected in its use of advanced materials and technologies in system construction. The company employs high-quality stainless steel for all components, ensuring durability and ease of cleaning. Its pneumatic conveying systems are designed with features that enhance operational efficiency, such as adjustable air flow controls, automated feed mechanisms, and integrated monitoring systems. These features help to minimize downtime, reduce material waste, and improve overall productivity in pharmaceutical manufacturing. Additionally, HeadPowder provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that its systems continue to operate at optimal levels throughout their service life.
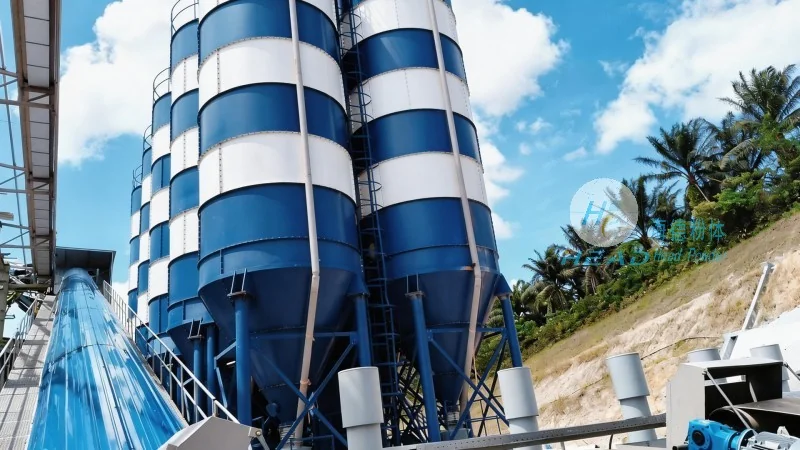
By leveraging its deep understanding of pharmaceutical processes and its expertise in pneumatic conveying technology, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient material handling solutions. The company's solutions are not only designed to meet current industry standards but also to adapt to future technological advancements, ensuring that clients can maintain a competitive edge in the pharmaceutical market. With a focus on customer satisfaction and product excellence, HeadPowder continues to be a key player in the provision of pharmaceutical pneumatic conveying systems.




