Soil air-driven conveying systems represent a sophisticated solution for transporting bulk materials, particularly in environments where traditional mechanical conveyors may face challenges. These systems utilize compressed air to move materials through a pipeline network, offering a flexible and efficient method for handling soil and other granular substances. The core principle involves creating a pressure differential that propels the material along the pipeline, often with the assistance of specialized equipment such as airlocks and cyclones to control flow and separation.
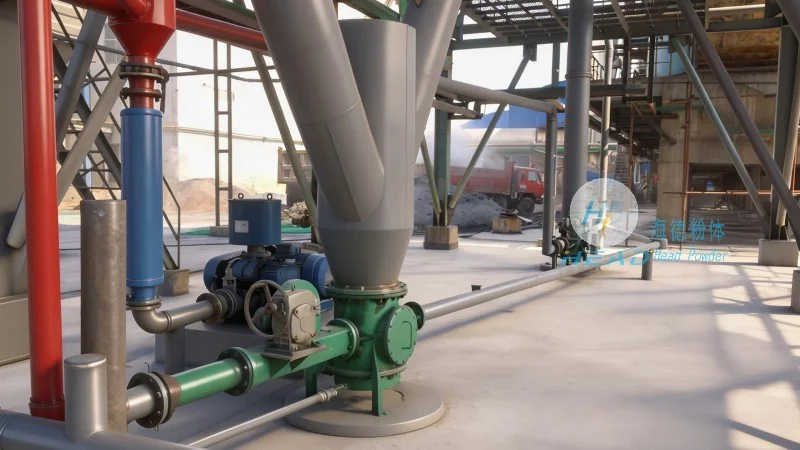
Key Working Principles of Soil Air-Driven Conveying Systems
The operation of soil air-driven conveying systems is based on the fundamental physics of fluid dynamics and material transport. At its essence, the system consists of a series of components that work in tandem to move soil from a source point to a destination. The primary mechanism involves injecting compressed air into the pipeline, which creates a low-pressure zone that draws the soil particles into the flow. This process, known as pneumatic conveying, relies on the interaction between the air and the material to achieve movement. The system typically includes a hopper or feeder to introduce the soil into the pipeline, a blower or compressor to supply the air, and a receiver or discharge point to collect the material at the end of the line. The design of the pipeline, including its diameter and length, is critical to ensuring efficient operation, as it directly impacts the pressure drop and the ability to maintain a consistent flow rate.
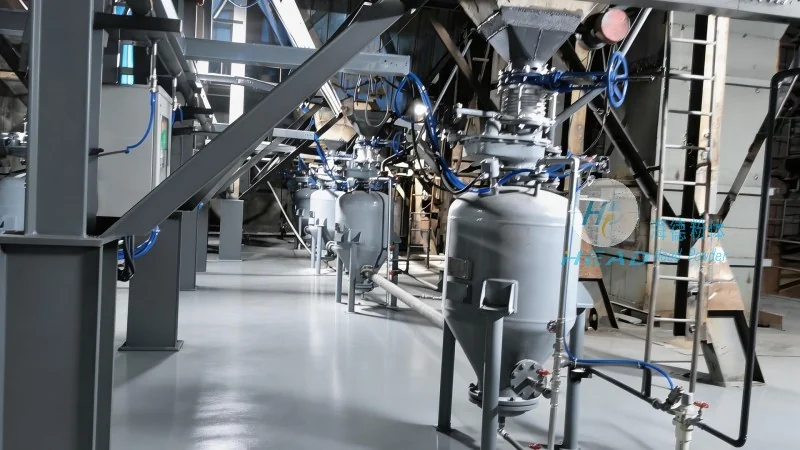
Common Working Scenes and Applications
Soil air-driven conveying systems are widely employed in various industrial and construction settings where the transportation of soil and similar materials is required. Common applications include mining operations, where soil and ore are moved between processing stages; construction sites, where earth is transported from excavation areas to disposal or reuse locations; and agricultural settings, where soil is transferred for composting or land preparation. In mining, these systems are particularly valuable for handling large volumes of material over long distances without the need for extensive infrastructure, such as conveyor belts or trucks. Construction sites benefit from the flexibility of pneumatic conveying, as it can navigate around obstacles and provide a dust-free method of material transport, enhancing safety and reducing environmental impact. Agricultural applications often involve the movement of soil from fields to processing facilities or storage areas, where the system's ability to handle fine particles and maintain consistent flow is advantageous.
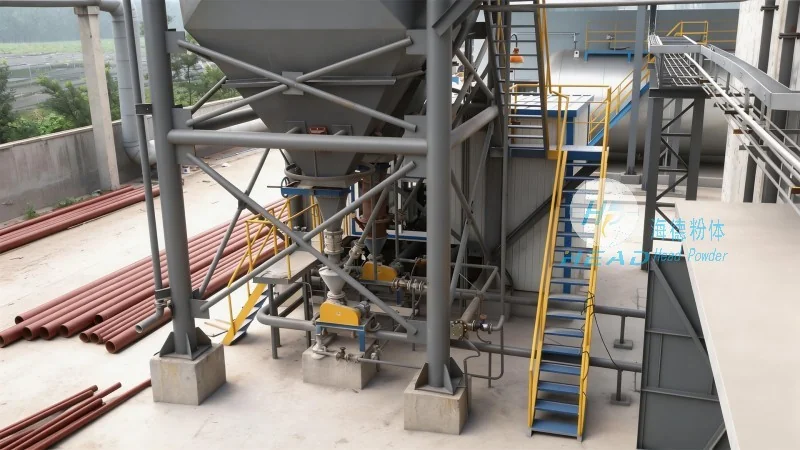
Features and Advantages of Soil Air-Driven Conveying Systems
Compared to traditional mechanical conveyors, soil air-driven conveying systems offer several distinct advantages that make them a preferred choice in many industries. One of the most significant benefits is the ability to transport materials over long distances with minimal maintenance. The absence of moving parts in the pipeline itself reduces wear and tear, leading to lower operational costs and increased reliability. Additionally, these systems are highly flexible, as the pipeline can be easily reconfigured or extended to accommodate changes in the work environment. This adaptability is particularly valuable in construction and mining, where project layouts may evolve over time. Another key advantage is the reduced risk of material contamination and the ability to maintain a clean, dust-free operation. Unlike mechanical conveyors, which may generate dust and expose workers to particulate matter, pneumatic systems can be enclosed and filtered, ensuring a safer working environment. Furthermore, the systems are capable of handling a wide range of soil types, from fine sand to larger gravel particles, without the need for additional processing or separation equipment.
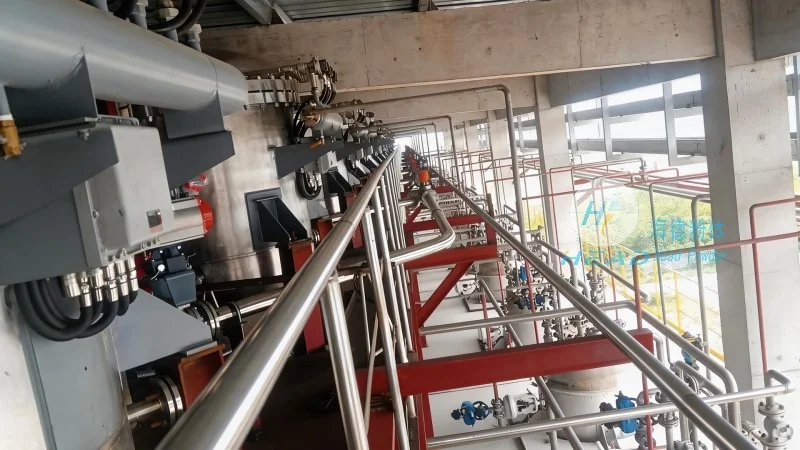
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of soil air-driven conveying systems and related equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing comprehensive solutions for material handling challenges. HeadPowder's products are designed to meet the specific needs of various applications, ensuring optimal performance and efficiency. The company's commitment to customer satisfaction and technical excellence has earned it a reputation for reliability and durability in the market. HeadPowder's headquarters and main operations are located in Shandong, China, where the company leverages its local expertise and resources to deliver high-quality products and services to clients worldwide.




