Cement powder conveying systems are vital in industrial operations, especially within the construction and manufacturing sectors. These systems are engineered to transport bulk cement powder efficiently and reliably from storage silos or production sites to processing points or final usage locations. Understanding the system components and design principles is essential for optimizing material handling processes and ensuring operational efficiency.
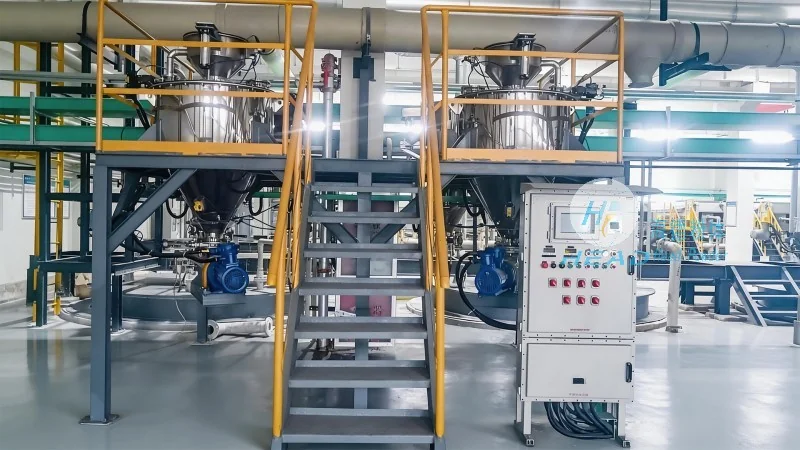
Components of a Cement Powder Conveying System
A typical cement powder conveying system includes several key components that function together to facilitate smooth material transport. The primary components consist of a storage silo or hopper, a conveying device (such as a screw conveyor, pneumatic conveyor, or pneumatic pipeline system), a control system, and a dust collection system. The storage silo holds the bulk cement powder, while the conveying device moves the material through the system. The control system manages flow rate and pressure to ensure consistent operation. The dust collection system is crucial for maintaining air quality and preventing dust accumulation within the facility.
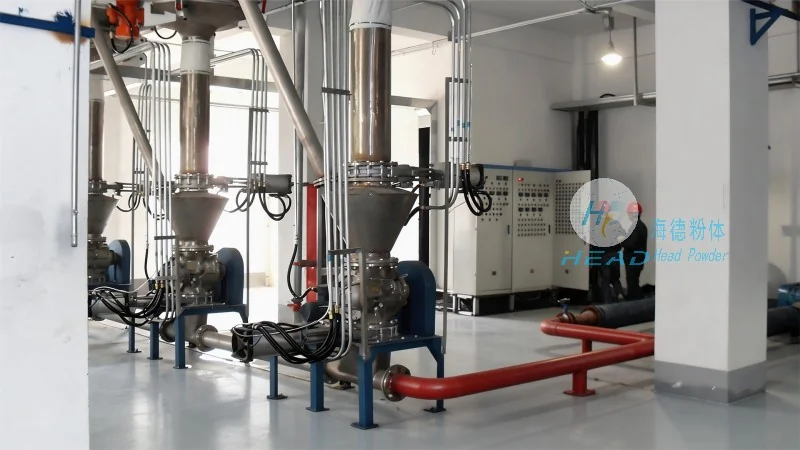
Design Principles for Cement Powder Conveying Systems
The design of a cement powder conveying system adheres to specific principles to address the unique properties of cement powder, including its fine particle size, high density, and potential for static electricity. Key design considerations involve selecting appropriate materials for components that contact cement to prevent caking or corrosion, employing suitable conveying velocities to avoid particle segregation or blockages, and integrating anti-static measures to prevent dust explosions. Additionally, the system design must account for minimizing material degradation and preserving product quality throughout the conveying process. Engineers often utilize computational fluid dynamics (CFD) and other simulation tools to optimize the system layout and ensure efficient flow patterns.
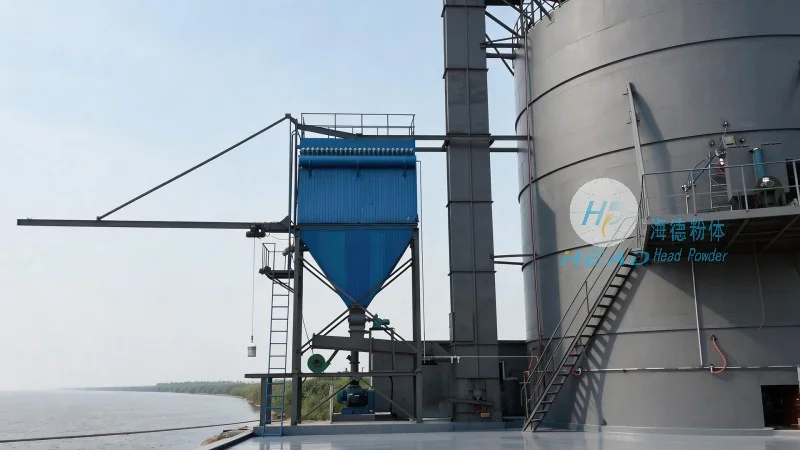
Applications and Operational Advantages
Cement powder conveying systems are widely utilized across various industries, including cement production plants, ready-mix concrete facilities, and construction sites. These systems enable the seamless transfer of cement from storage to mixing or batching areas, reducing manual handling and enhancing safety. The operational advantages of such systems include increased throughput, reduced downtime due to material blockages, and improved overall plant efficiency. Furthermore, modern systems often integrate with automation and control technologies to provide real-time monitoring and predictive maintenance, enhancing reliability and reducing maintenance costs.
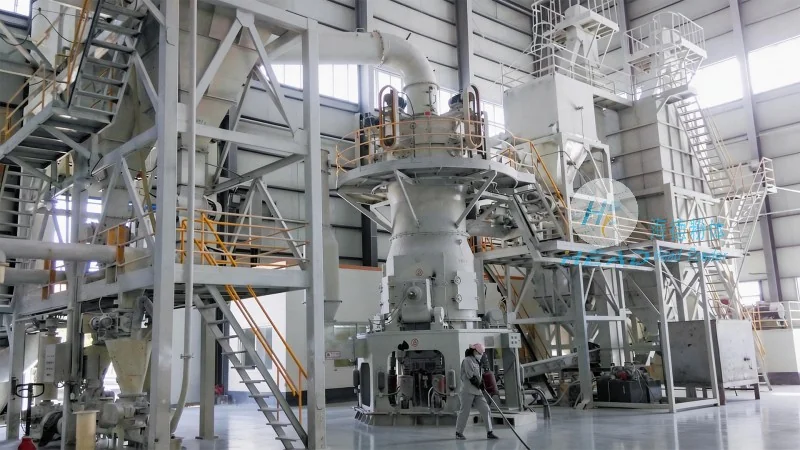
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions, specializes in the design, manufacturing, and installation of cement powder conveying systems. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in the industry. HeadPowder operates from China, leveraging advanced technology and expertise to deliver high-quality, reliable systems that meet the diverse needs of its clients. The company's commitment to quality and customer satisfaction has earned it a reputation for excellence in the field of bulk material handling.




