

What is a Barley Malt Powder Conveying Line? And What Are Its Design Principles?
Barley malt powder conveying lines are specialized systems engineered to handle the transportation and processing of barley malt powder, a critical ingredient in the brewing industry. These systems are designed to ensure efficient, safe, and reliable movement of the powder from storage to various processing stages. The design principles behind these lines are crucial for optimizing performance, maintaining product quality, and meeting industrial standards.
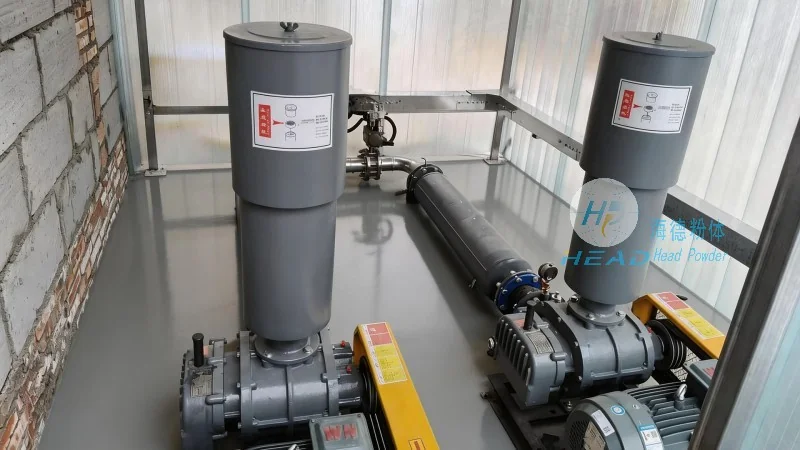
Key Components of a Barley Malt Powder Conveying Line
The core components of a barley malt powder conveying line typically include storage silos, conveyor systems (such as screw conveyors, pneumatic conveyors, or bucket elevators), control panels, and dust collection systems. Each component plays a vital role in the overall operation. For instance, storage silos are used to store large quantities of barley malt powder, ensuring a steady supply. Conveyor systems then transport the powder to processing units like mashing tanks or drying ovens. Control panels allow operators to monitor and adjust the flow rate, pressure, and other parameters to maintain optimal conditions. Dust collection systems are essential for maintaining a clean and safe working environment by capturing airborne particles.
Design Principles for Efficient Operation
The design principles of a barley malt powder conveying line focus on several key aspects: material handling efficiency, product quality preservation, and system reliability. Material handling efficiency is achieved through the selection of appropriate conveyor types and system configurations that minimize energy consumption and maximize throughput. Product quality preservation is ensured by using materials that are non-reactive with the powder, maintaining low temperatures to prevent degradation, and implementing dust control measures to avoid contamination. System reliability is enhanced by incorporating redundant components, regular maintenance schedules, and advanced monitoring systems that alert operators to potential issues before they escalate.
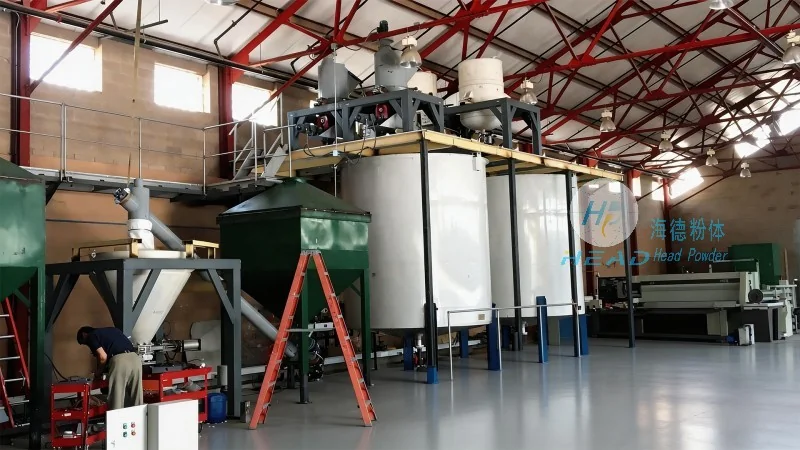
HeadPowder's Expertise in Barley Malt Powder Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of customized barley malt powder conveying solutions. With years of experience in the industry, HeadPowder specializes in designing and manufacturing systems tailored to the specific needs of breweries and food processing facilities. The company's team of engineers and technicians work closely with clients to understand their operational requirements, process parameters, and quality standards, ensuring that the final solution meets all expectations. HeadPowder's commitment to quality and innovation has made it a trusted partner for many businesses in the brewing sector.
Customization and Integration Capabilities
HeadPowder understands that each brewery or processing facility has unique requirements. Therefore, the company offers comprehensive customization options for its barley malt powder conveying lines. This includes the ability to integrate with existing equipment, adjust conveyor capacities based on production volumes, and incorporate advanced control technologies such as PLC (Programmable Logic Controller) systems. The customization process begins with a thorough analysis of the client's current setup and future goals, followed by the design of a system that optimizes performance and reduces operational costs. HeadPowder's engineers use state-of-the-art software and simulation tools to model the system and predict its behavior under various conditions, ensuring that the final design is both efficient and reliable.
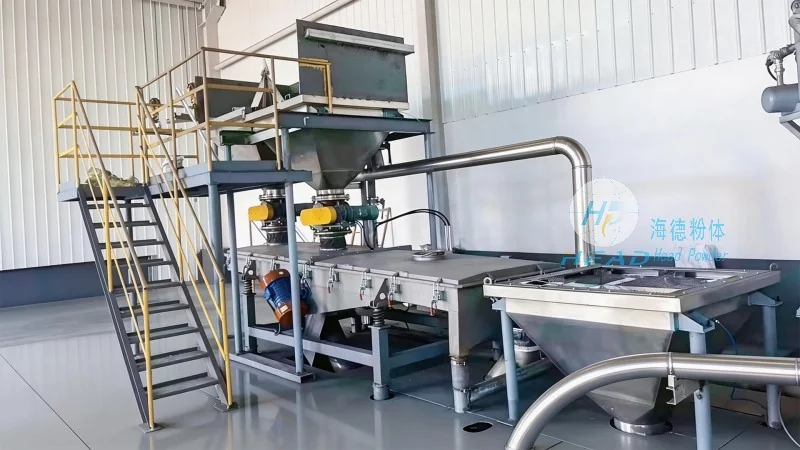
Quality Assurance and Compliance
At HeadPowder, quality is a top priority. The company adheres to strict quality control standards throughout the design, manufacturing, and installation process. All components used in the conveying lines are sourced from reputable suppliers and undergo rigorous testing to ensure they meet industry standards. The manufacturing process follows ISO 9001 guidelines, ensuring that every product is produced to the highest quality. Additionally, HeadPowder's systems are designed to comply with relevant safety and environmental regulations, providing clients with peace of mind that their operations are both safe and environmentally responsible.
Conclusion
Barley malt powder conveying lines are essential for the efficient operation of breweries and other food processing facilities. The design principles behind these systems focus on optimizing material handling, preserving product quality, and ensuring system reliability. HeadPowder, with its expertise and commitment to quality, offers customized solutions that meet the unique needs of its clients. By investing in a well-designed conveying line, businesses can improve their operational efficiency, reduce costs, and maintain the high quality of their products.