Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable enterprise based in Shandong, China, specializing in the design, manufacturing, and supply of advanced pneumatic conveying equipment. With a strong commitment to technological innovation and quality assurance, HeadPowder has established itself as a key player in the industry, delivering reliable solutions for the efficient handling of silicate materials. The company's expertise lies in understanding the unique characteristics of silicate products, such as their particle size, moisture content, and flow properties, enabling the development of tailored pneumatic conveying systems that meet the specific needs of clients across various sectors.
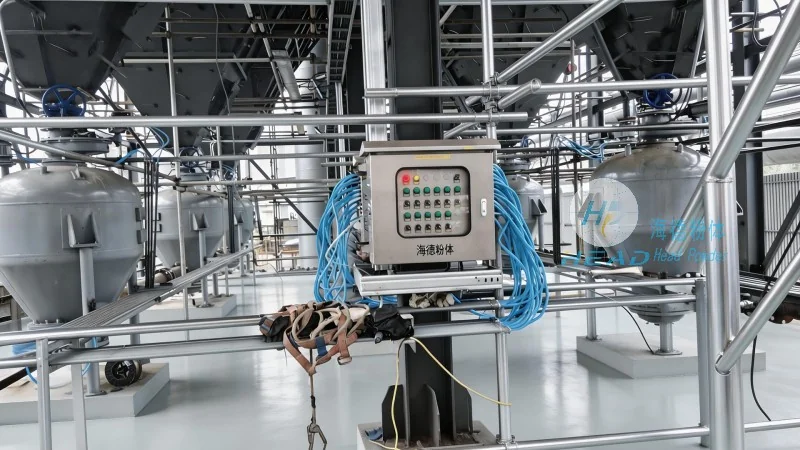
Overview of Silicate Pneumatic Conveying Equipment
Silicate pneumatic conveying equipment is a critical component in material handling processes, particularly for transporting silicate-based materials like silica, kaolin, and other mineral powders. These systems utilize air or gas as the conveying medium to move bulk materials from one location to another without the need for mechanical components like belts or buckets. The primary advantage of pneumatic conveying is its ability to handle materials that are difficult to transport using traditional methods, such as those with high moisture content or abrasive properties. HeadPowder's equipment is engineered to ensure efficient, safe, and cost-effective material transport, making it an essential solution for industries that rely on consistent and reliable material flow.
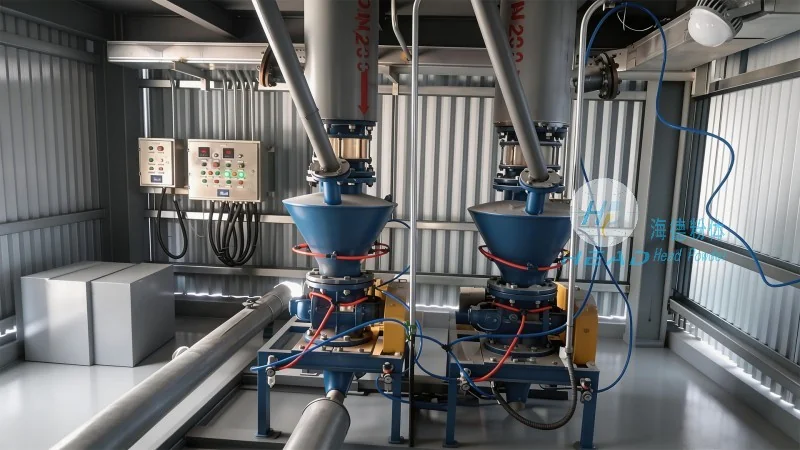
Structural Components and Working Principles
The core structure of silicate pneumatic conveying equipment typically includes several key components: a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with pressure vessels or ducts), and a receiver for the discharged material. The working principle revolves around the creation of a pressure differential between the hopper and the receiver. By introducing air or gas into the system, the material is lifted and transported through the conveying line. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at lower pressures, suitable for short distances and low to medium material loads, while dense-phase systems use higher pressures to achieve longer transport distances and handle larger volumes with higher efficiency. HeadPowder's equipment incorporates advanced control mechanisms to optimize the pressure and flow rates, ensuring stable and consistent material transport. The company's designs also emphasize safety features, such as pressure relief valves and material flow indicators, to prevent blockages and ensure operational safety.
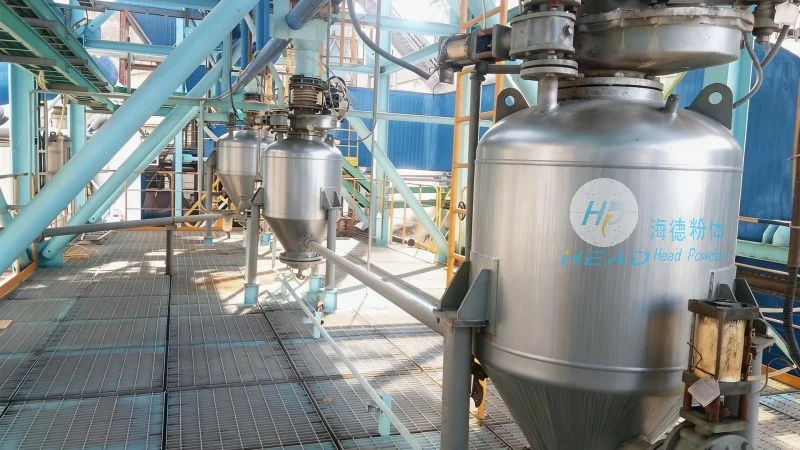
Key Features and Advantages of HeadPowder's Silicate Pneumatic Conveying Systems
HeadPowder's silicate pneumatic conveying equipment is distinguished by several key features that enhance performance and reliability. The systems are constructed from high-quality materials, such as stainless steel and corrosion-resistant alloys, to withstand the chemical and physical stresses associated with silicate materials. This ensures long service life and minimal maintenance requirements. The company's equipment is also equipped with intelligent control systems that allow for real-time monitoring and adjustment of conveying parameters, such as air pressure and flow rate. This automation capability not only improves operational efficiency but also reduces human error and operational costs. Additionally, HeadPowder's designs prioritize energy efficiency, utilizing optimized air flow and pressure management to minimize energy consumption while maintaining high transport capacity. The equipment is also designed for easy maintenance and cleaning, with features like removable components and self-cleaning mechanisms that help prevent material buildup and ensure consistent performance over time.
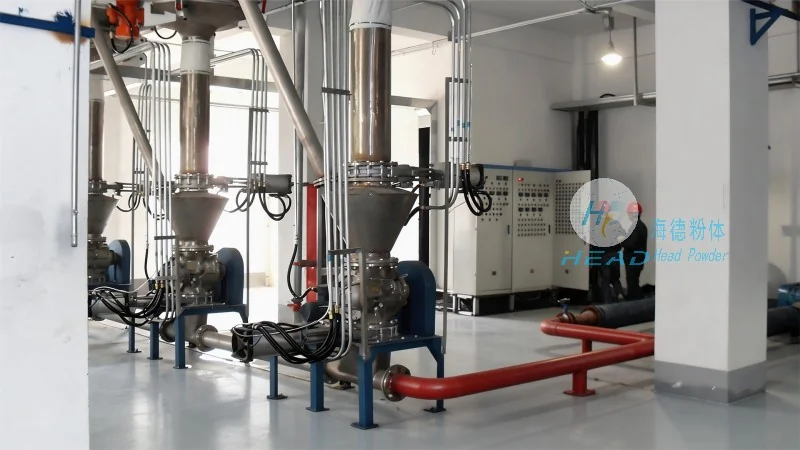
Applications and Industries Served
The versatility of silicate pneumatic conveying equipment makes it applicable across a wide range of industries. In the chemical industry, these systems are used for transporting raw materials like silica and kaolin for the production of ceramics, glass, and other chemical products. The food and pharmaceutical industries also benefit from the hygienic and dust-free nature of pneumatic conveying, which helps maintain product quality and compliance with regulatory standards. Additionally, the construction and mining sectors utilize these systems for transporting bulk materials like sand and gravel, contributing to improved operational efficiency and reduced labor costs. HeadPowder's equipment is tailored to meet the specific requirements of each industry, ensuring that clients receive solutions that are both effective and cost-efficient.




