For industrial facilities dealing with fly ash, efficient and reliable material handling is crucial. This article provides an overview of fly ash pneumatic conveying equipment, focusing on its structural design and operational principles. The equipment is engineered to handle the unique challenges associated with fly ash transportation, ensuring safe and effective material movement within processing plants.
Key Components and Structural Design
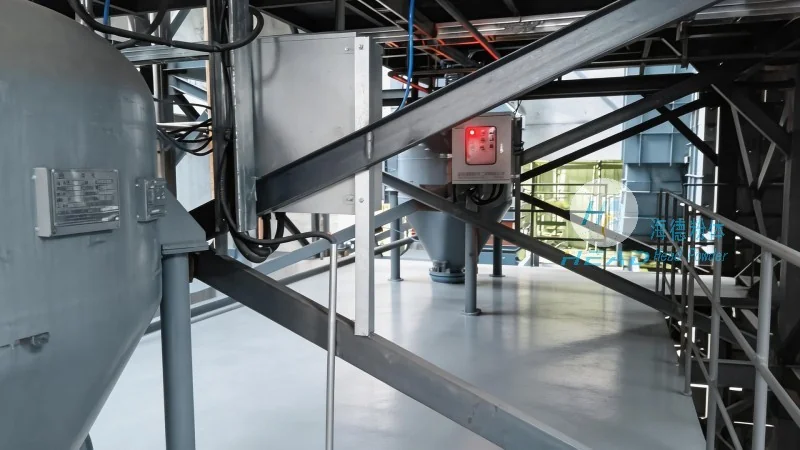
Fly ash pneumatic conveying systems typically consist of several core components that work in tandem to achieve efficient material transport. The primary components include the hopper, which serves as the material storage and feeding unit; the conveying line, which may be a flexible hose or rigid pipe; the air mover, such as a blower or fan, that generates the necessary airflow; and the control system, which regulates the pressure and flow rates. The hopper is designed with a sloped bottom to facilitate smooth material discharge, often equipped with a rotary valve or gate to control the flow rate. The conveying line is made from materials resistant to abrasion and corrosion, such as stainless steel or high-density polyethylene, to withstand the abrasive nature of fly ash. The air mover is selected based on the system's capacity and pressure requirements, ensuring sufficient air volume to maintain the material in suspension. The control system integrates sensors and valves to monitor and adjust the system's performance, optimizing the conveying process and preventing issues like blockages or pressure fluctuations.
Working Principles of Pneumatic Conveying
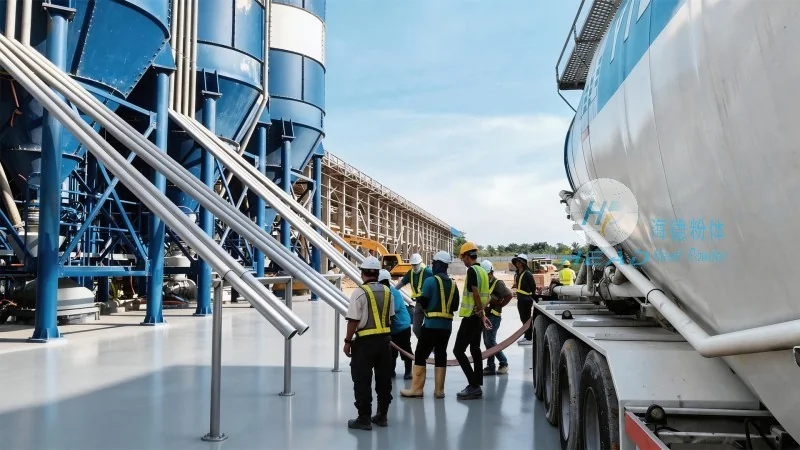
The operation of fly ash pneumatic conveying equipment is based on the principle of creating a low-pressure or high-pressure air stream that lifts and transports the fly ash particles through the conveying line. In a typical system, the air mover draws air from the environment and forces it through the conveying line, while the hopper feeds the fly ash into the line. As the air flows, it creates a negative pressure or positive pressure environment, depending on the system design, which lifts the fly ash particles into the air stream. The particles are then carried along the conveying line to the destination point, such as a storage silo or processing unit. The system may use a combination of positive and negative pressure zones to achieve efficient transport over longer distances. The control system continuously monitors the pressure and flow rates, adjusting the air volume as needed to maintain optimal conveying conditions. This dynamic adjustment ensures that the system operates efficiently, minimizing energy consumption and preventing material degradation or loss.
Advantages of Fly Ash Pneumatic Conveying Equipment
Compared to traditional mechanical conveying methods, fly ash pneumatic conveying equipment offers several advantages that make it a preferred choice for industrial applications. One of the key benefits is the ability to transport fly ash in a dust-free environment, reducing the risk of airborne particulate emissions and improving workplace safety. The system also eliminates the need for moving parts in the conveying line, reducing maintenance requirements and extending the equipment's service life. Additionally, pneumatic conveying allows for flexible routing of the conveying line, enabling the system to be adapted to different plant layouts and operational needs. The equipment is also capable of handling varying fly ash characteristics, such as different particle sizes and moisture content, without significant performance degradation. Furthermore, the system can be integrated with other processing equipment, such as filters or cyclones, to form a complete material handling solution. The energy efficiency of pneumatic conveying systems is another advantage, as they can operate with lower energy consumption compared to mechanical systems, especially for long-distance transport. Overall, the advantages of fly ash pneumatic conveying equipment make it a reliable and efficient solution for handling fly ash in industrial settings.
About Shandong HeadPowder Engineering Co., Ltd.
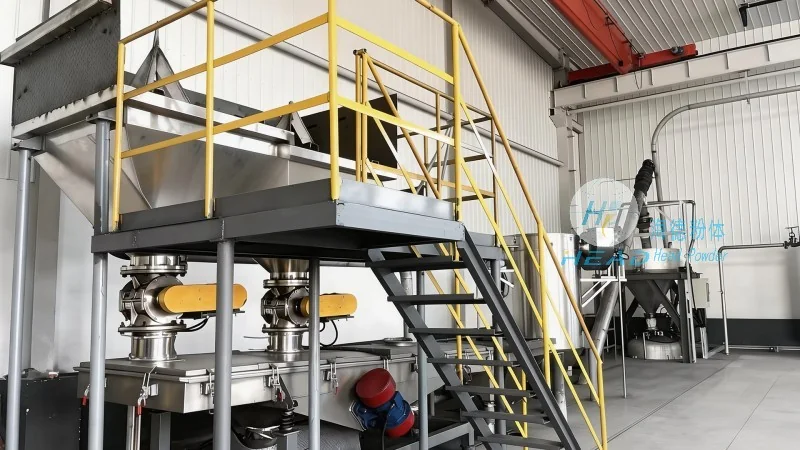
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of fly ash handling equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the industrial sector. HeadPowder's expertise lies in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. The company's products are engineered to meet the highest standards of performance, durability, and safety, ensuring reliable operation in demanding industrial environments. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, maintenance, and technical assistance. The company's facilities are equipped with advanced manufacturing technologies and quality control systems, ensuring that every product meets the strictest industry standards. HeadPowder serves a wide range of industries, including power generation, cement, and chemical processing, providing tailored solutions for their fly ash handling challenges. The company's dedication to excellence and customer service has earned it a reputation for reliability and professionalism in the market.




