Metering bin pumps are a critical component in modern material handling and processing industries, designed to efficiently transport bulk materials through pneumatic conveying systems. These devices play a vital role in ensuring consistent and controlled material flow, which is essential for maintaining production efficiency and product quality. The integration of precise metering capabilities with robust pneumatic conveying technology makes metering bin pumps an indispensable tool for various applications, including chemical processing, food processing, and mining operations.
Structural Components and Working Principles
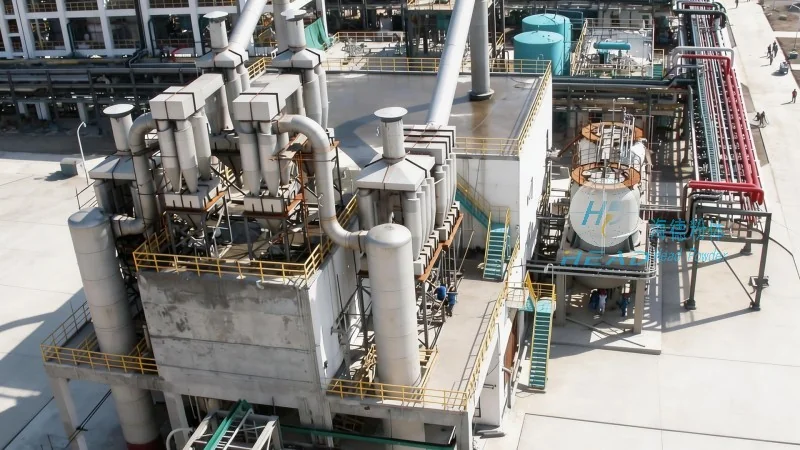
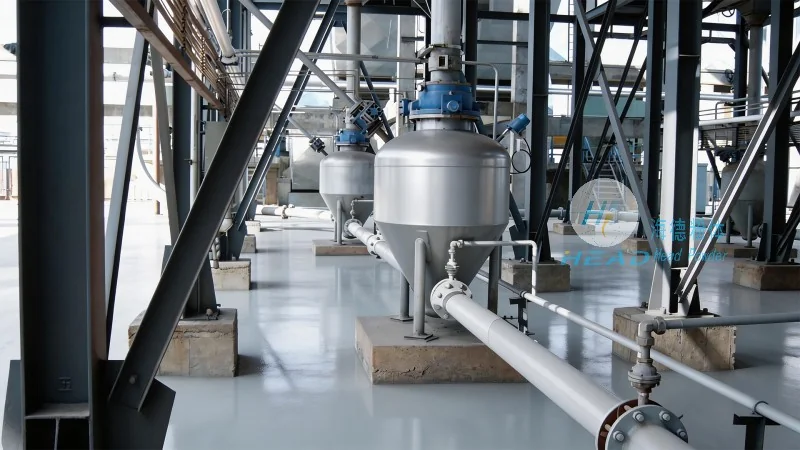
The core structure of a metering bin pump typically consists of several key components that work in harmony to achieve accurate material measurement and pneumatic transport. The main parts include a hopper for material storage, a metering chamber equipped with a rotating or oscillating valve mechanism, a pressure vessel or air receiver, and a pneumatic conveying line. The hopper is designed to hold the bulk material, ensuring a constant supply to the metering chamber. The metering chamber, often featuring a rotary valve or a slide valve, regulates the amount of material discharged into the pneumatic system. This controlled discharge is then mixed with compressed air, creating a slurry that is transported through the conveying line to the destination point.
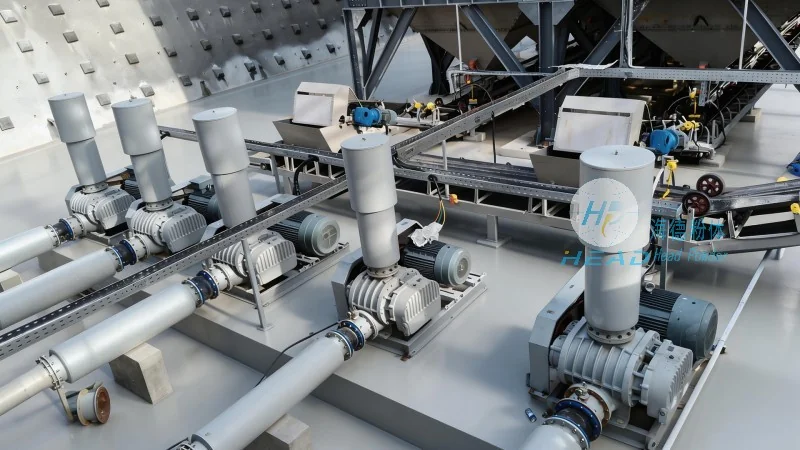
The working principle of a metering bin pump relies on the precise control of material flow and air pressure. The rotating or oscillating valve in the metering chamber opens and closes at a controlled rate, allowing a specific volume of material to be released into the air stream. The compressed air, supplied by a separate air compressor, creates the necessary pressure to propel the material through the pipeline. The combination of accurate material metering and effective air compression ensures that the conveying process is both efficient and reliable. This system is particularly effective for handling materials that are difficult to convey by other means, such as fine powders or abrasive substances.
Key Features and Advantages
HeadPowder, a leading manufacturer based in Shandong, China, offers advanced metering bin pumps that incorporate several key features to enhance performance and durability. These features include a robust hopper design that minimizes material degradation and blockages, a precision metering valve that ensures consistent flow rates, and a pressure vessel that maintains stable air pressure. The company’s products are engineered to handle a wide range of materials, from low-density powders to high-density granules, with minimal maintenance requirements. The use of high-quality materials and advanced manufacturing techniques ensures that the equipment operates reliably over extended periods, reducing downtime and operational costs for industrial clients.
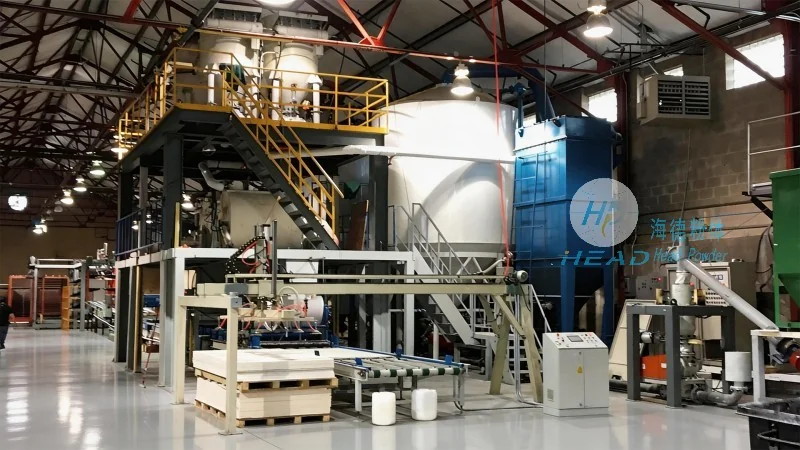
One of the significant advantages of metering bin pumps is their ability to provide precise material control, which is crucial for processes that require exact dosing or batching. This accuracy helps in maintaining product consistency and reducing waste, leading to improved overall efficiency. Additionally, the pneumatic conveying system associated with these pumps offers a flexible and cost-effective solution for material transport, as it eliminates the need for complex mechanical conveying systems. The compact design of the metering bin pump also allows for easy integration into existing production lines, making it a versatile choice for various industrial applications.
Applications and Industrial Use Cases
Metering bin pumps are widely used in various industries due to their adaptability and efficiency. In the chemical industry, they are employed to transport reactive powders and liquids, ensuring safe and controlled handling. The food processing sector utilizes these pumps for conveying ingredients like flour, sugar, and spices, maintaining hygiene and product quality. The mining industry also benefits from metering bin pumps, as they help in transporting ore and other bulk materials from processing plants to storage or further processing facilities. These applications highlight the versatility of the equipment and its importance in modern industrial operations.
The design of metering bin pumps allows for customization to meet specific operational requirements. For instance, the size of the hopper and the capacity of the metering chamber can be adjusted based on the volume of material to be handled. The air pressure and flow rate can also be optimized to suit different material characteristics and conveying distances. This flexibility makes the equipment suitable for a wide range of industrial settings, from small-scale operations to large-scale manufacturing plants.




