HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced dust-free automatic pneumatic conveying systems. These systems are engineered to efficiently transport bulk materials while maintaining a clean and controlled environment, making them ideal for industries where dust contamination is a critical concern.
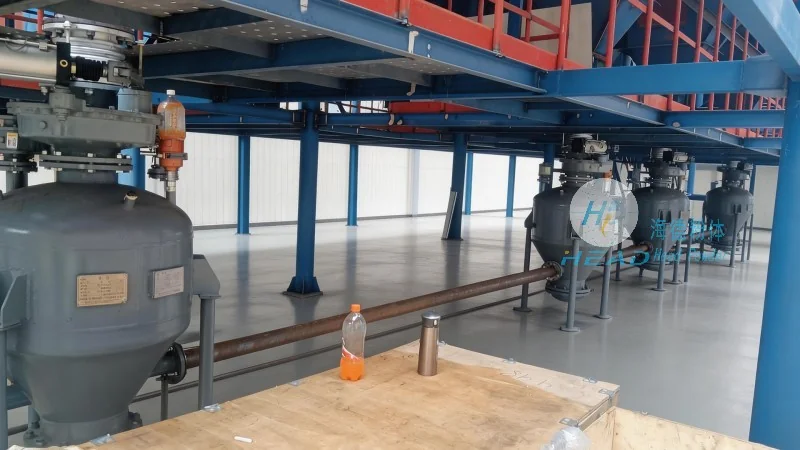
Overview of Dust-Free Automatic Pneumatic Conveying Equipment
Dust-free automatic pneumatic conveying equipment is a sophisticated solution for material handling, combining the benefits of pneumatic transport with advanced filtration and sealing technologies. The primary goal of such systems is to move powders, granules, and other dry bulk materials from one location to another without exposing them to the ambient air or vice versa. This ensures that the material remains free from contamination and that the surrounding environment is protected from dust emissions.
Key Components and Structure of the Equipment
The core structure of a dust-free automatic pneumatic conveying system typically includes several essential components, each playing a crucial role in the overall operation. The main parts are the material feed hopper, the air supply system (including a blower or compressor), the conveying line (usually a flexible or rigid tube), the separation and collection units, and the filtration system. The feed hopper is designed to store and meter the material, ensuring a consistent flow into the system. The air supply unit generates the necessary pressure or vacuum to move the material through the conveying line. The conveying line, often made of stainless steel or other corrosion-resistant materials, is equipped with appropriate fittings and valves to control the flow direction and speed. The separation and collection units are responsible for directing the material to its final destination, such as a silo or processing unit, while the filtration system captures any dust particles that may escape, ensuring compliance with environmental regulations and maintaining a clean working environment.
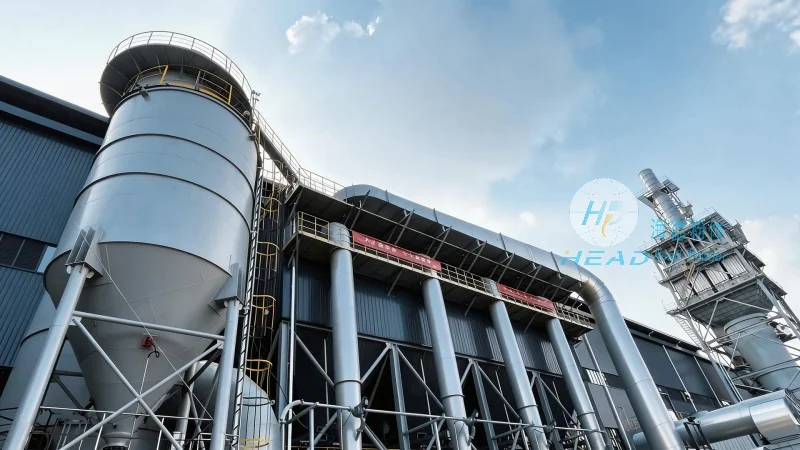
Working Principle of the Pneumatic Conveying System
The operation of a dust-free automatic pneumatic conveying system is based on the principle of air movement. In a typical setup, the material is fed into the system from the hopper, and the air supply unit creates a pressure differential. This pressure difference causes the material to be entrained in the air stream and carried through the conveying line to the collection point. The system can operate in either positive pressure or negative pressure modes, depending on the specific application and material characteristics. Positive pressure systems use compressed air to push the material forward, while negative pressure systems use vacuum to pull the material through the line. The choice of mode depends on factors such as the material's density, flowability, and the distance to be covered. The filtration system is integrated into the design to capture any fine particles that may be released during the conveying process, preventing dust from escaping into the environment and ensuring that the material remains clean and free from contaminants.
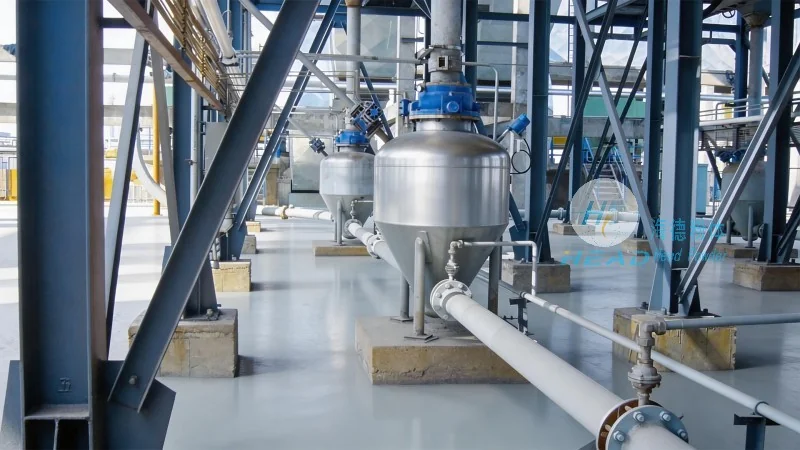
Advantages of Dust-Free Automatic Pneumatic Conveying Equipment
Implementing a dust-free automatic pneumatic conveying system offers numerous advantages for industrial applications. Firstly, it provides a highly efficient method for transporting bulk materials over long distances without the need for mechanical components like conveyors or elevators, which can be prone to maintenance issues and material degradation. Secondly, the sealed system prevents dust contamination, which is critical in industries such as pharmaceuticals, food processing, and electronics manufacturing, where product purity and worker safety are paramount. Thirdly, the system is energy-efficient compared to traditional methods, as it uses compressed air to move the material, reducing the need for heavy machinery and associated power consumption. Additionally, the compact design of these systems allows for easy integration into existing production lines, minimizing space requirements and installation costs. The durability and reliability of the equipment, coupled with minimal maintenance requirements, further enhance its appeal for long-term industrial use.
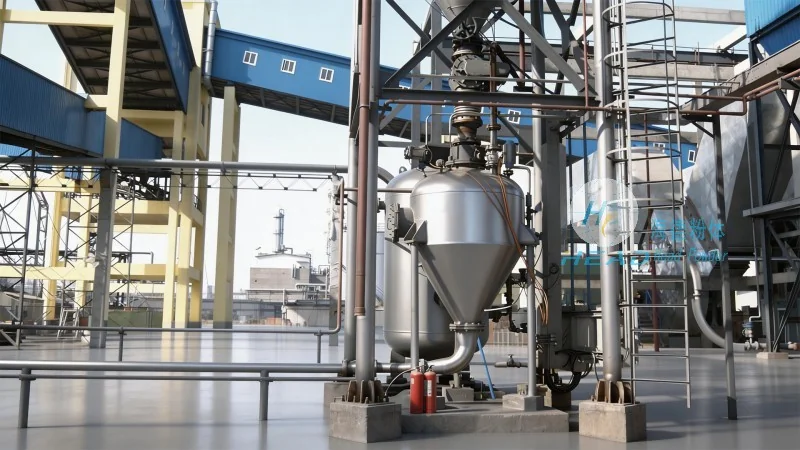
Application Scenarios and Industries
Dust-free automatic pneumatic conveying equipment is widely used across various industries due to its versatility and effectiveness. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and other powders, ensuring that the materials remain sterile and free from contamination. In the food processing sector, it handles ingredients like flour, sugar, and spices, maintaining product quality and safety standards. The electronics manufacturing industry utilizes these systems to transport fine powders and components, preventing dust buildup that could affect the performance of sensitive equipment. Additionally, in the chemical and chemical processing industries, the equipment is employed to handle powders and granules, ensuring that the material is transported safely and without exposure to the environment. The ability to handle a wide range of materials, from fine powders to coarse granules, makes the system suitable for diverse applications across different sectors.
Conclusion and Company Information
HeadPowder, with its headquarters in Shandong, China, is committed to providing high-quality dust-free automatic pneumatic conveying equipment that meets the stringent requirements of modern industrial applications. By combining advanced engineering, robust materials, and efficient design, the company ensures that its products deliver reliable performance and long-term value. The dust-free pneumatic conveying systems are designed to enhance operational efficiency, improve product quality, and maintain a safe working environment, making them an essential investment for industries that prioritize precision and cleanliness. With a focus on innovation and customer satisfaction, HeadPowder continues to lead the way in the development of cutting-edge material handling solutions.




