Small bag pneumatic conveying equipment is a specialized system designed for the efficient transport of bulk materials, particularly in industrial settings where precise and controlled material handling is crucial. This equipment utilizes compressed air to move powders, granules, or other particulate materials from one location to another, offering advantages such as minimal product contamination, reduced maintenance requirements, and the ability to operate in enclosed environments. The system is widely used across various industries, including pharmaceuticals, food processing, and chemical manufacturing, where maintaining product integrity and safety is paramount.
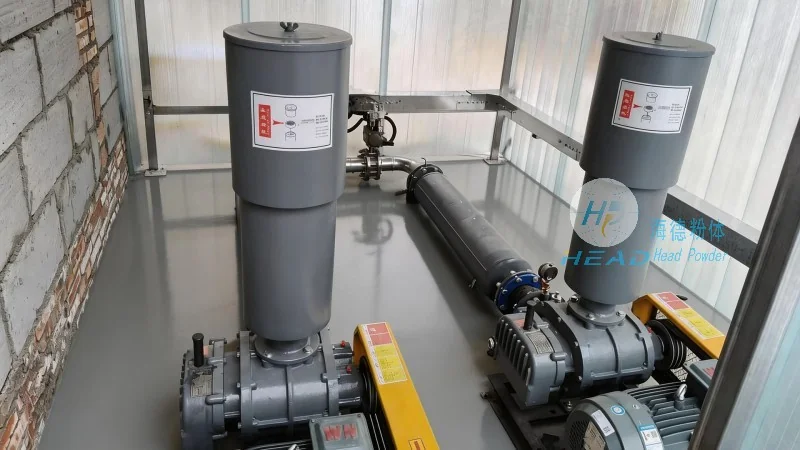
Structural Principles of Small Bag Pneumatic Conveying Equipment
The core of small bag pneumatic conveying equipment lies in its integrated components and the principles of air flow dynamics. The system typically consists of a hopper or feed hopper, a conveying line (often equipped with a flexible hose or rigid pipe), a receiver or discharge hopper, and a blower or air compressor that generates the necessary air pressure. The hopper is where the material is stored and fed into the system, while the conveying line transports the material to the receiver. The blower provides the motive force, creating a pressure differential that propels the material through the line. Key components include the feed mechanism (such as a rotary valve or screw feeder), the air filter and regulator to maintain air quality and pressure, and the control system that manages the flow rate and pressure. The design of the conveying line, including its diameter and length, is critical to ensure efficient material transport without excessive pressure loss or material degradation.
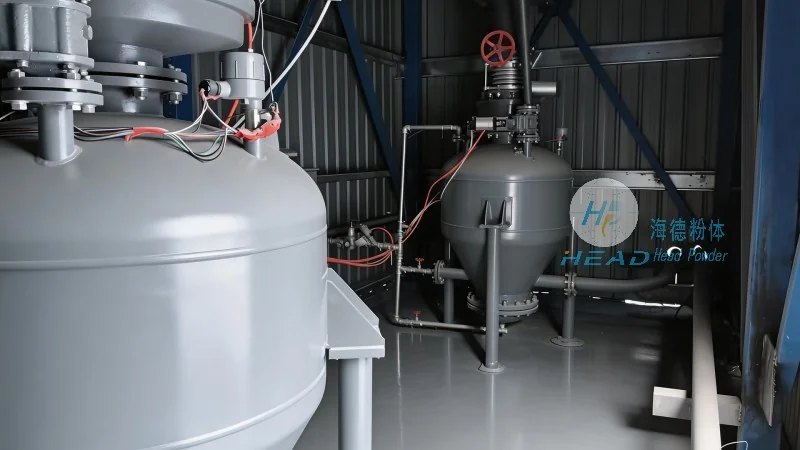
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the manufacturer of small bag pneumatic conveying equipment, is a leading company based in Shandong, China. With a strong focus on engineering excellence and customer satisfaction, HeadPowder specializes in the design, manufacturing, and supply of pneumatic conveying systems tailored to diverse industrial needs. The company's headquarters is located in Shandong, where it leverages advanced technology and experienced engineering teams to develop high-quality equipment that meets international standards. HeadPowder's commitment to innovation and quality has made it a trusted partner for businesses seeking reliable and efficient material handling solutions. The company's products are known for their durability, efficiency, and adaptability, catering to a wide range of applications from small-scale operations to large industrial facilities.
Key Features and Benefits of Small Bag Pneumatic Conveying Equipment
Small bag pneumatic conveying equipment offers several key features that make it an attractive choice for material transport. One of the primary benefits is its ability to handle a variety of materials, including fine powders, coarse granules, and even sticky or abrasive substances. The enclosed system prevents dust and contamination, ensuring that the transported material remains clean and free from external pollutants. Additionally, the equipment operates quietly and with minimal vibration, reducing noise pollution and improving workplace safety. The system is also flexible, allowing for easy integration with existing production lines and the ability to adjust the conveying rate as needed. Another advantage is the reduced need for manual handling, as the equipment automates the material transport process, enhancing operational efficiency and reducing labor costs. The compact design of small bag systems makes them suitable for spaces with limited room, and they can be customized to fit specific operational requirements, such as varying material types or throughput rates.
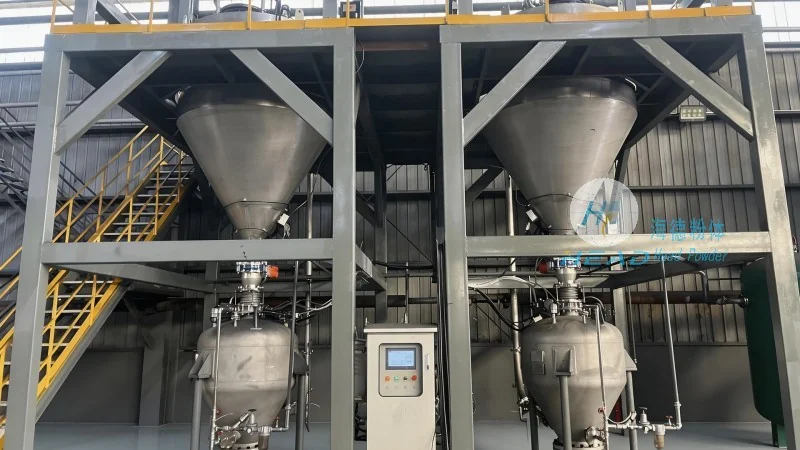
Applications and Industries Served
Small bag pneumatic conveying equipment is utilized in numerous industries where bulk material handling is essential. In the pharmaceutical industry, the equipment is used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring that the materials are handled in a sterile and controlled environment. The food processing industry benefits from the system's ability to handle food-grade powders and granules, maintaining hygiene standards and preventing cross-contamination. The chemical industry uses small bag systems to transport chemicals, powders, and other hazardous materials, providing a safe and efficient method of transport. Other applications include the handling of minerals, plastics, and agricultural products, where the equipment's versatility and reliability are valued. The equipment is particularly suitable for applications requiring high precision, such as in research and development laboratories or in manufacturing processes where material purity is critical.




