HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in the design and production of pneumatic conveying systems tailored for limestone powder applications. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in various industrial settings.
Understanding the Core Principle of Pneumatic Conveying for Limestone Powder
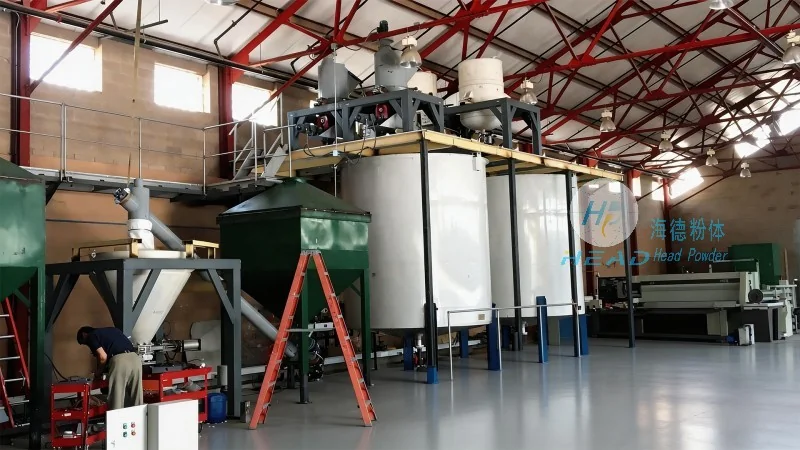
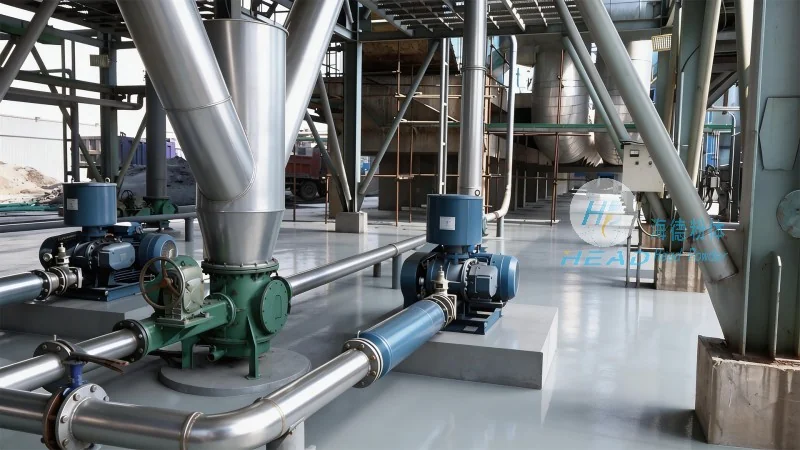
The pneumatic conveying system for limestone powder operates on the principle of transporting bulk materials through a pipeline using air or gas as the conveying medium. Unlike traditional mechanical conveyors, this method eliminates the need for physical contact between the material and the conveyor components, thereby reducing wear and tear and minimizing the risk of contamination. The system typically consists of a feeding device, a conveying pipeline, a separation unit, and a discharge outlet. The feeding device, often a rotary valve or a feeder, introduces the limestone powder into the pipeline at a controlled rate. As the material enters the pipeline, a fan or blower generates a flow of air, which propels the powder particles through the system. The separation unit, such as a cyclone or a bag filter, then separates the powder from the air stream, allowing the powder to be discharged into the target container while the air is either recirculated or vented to the atmosphere. This process ensures efficient and continuous material transport with minimal downtime and maintenance requirements.
Key Working Scene Characteristics of Limestone Powder Pneumatic Conveying Machines
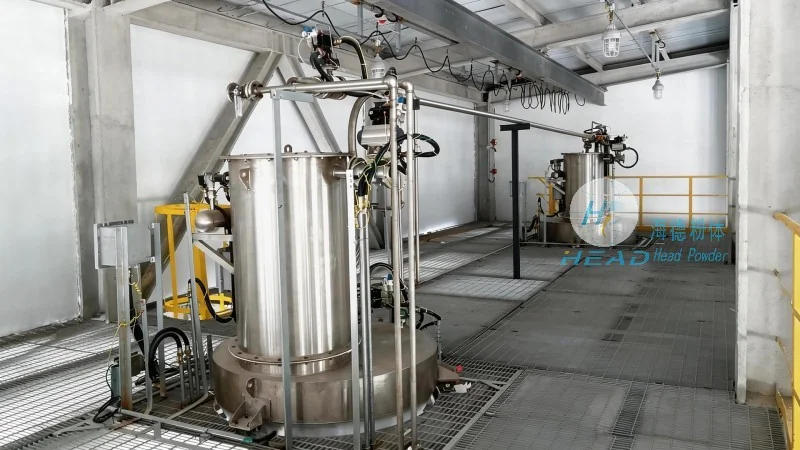
The working scene characteristics of limestone powder pneumatic conveying machines are tailored to meet the specific demands of industrial applications. These characteristics include high efficiency in material transport, low energy consumption, and the ability to handle fine powders without clogging or degradation. The systems are designed to operate in environments where dust control is critical, as limestone powder can be a fine, airborne particulate that requires effective containment to prevent health hazards and environmental pollution. Additionally, the flexibility of pneumatic conveying allows for the integration of multiple feeding and discharge points, enabling complex material flow paths in large-scale production facilities. The compact design of these machines also makes them suitable for installations with limited space, as they do not require extensive floor space or complex infrastructure compared to traditional conveyors. Another important characteristic is the adaptability to varying material properties, such as moisture content and particle size distribution, which can affect the conveying performance. Advanced control systems are often integrated into the equipment to optimize the air flow and material feed rate, ensuring consistent and reliable operation under different operating conditions.
Application Scenarios and Industrial Benefits
Limestone powder pneumatic conveying machines are widely used in various industrial sectors, including cement production, chemical processing, and food processing. In cement manufacturing, these systems are crucial for transporting limestone raw materials from storage silos to the grinding mills, where they are processed into cement clinker. The high efficiency and low maintenance of the pneumatic conveying systems contribute to increased production throughput and reduced operational costs in cement plants. In the chemical industry, limestone powder is used as a raw material in the production of calcium carbonate and other chemical products. The ability of the pneumatic conveying system to handle fine powders and maintain product purity is essential for meeting the stringent quality standards in chemical manufacturing. Similarly, in the food industry, limestone powder is used as a dietary supplement or as a processing aid. The hygienic design of the pneumatic conveying equipment ensures that the material remains free from contamination, meeting the strict regulations for food processing. The industrial benefits of using these systems extend beyond material transport efficiency, as they also contribute to improved workplace safety by reducing manual handling of powders and minimizing dust exposure. This leads to a healthier working environment and lower risk of respiratory illnesses among workers.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a reputable company dedicated to providing high-quality pneumatic conveying solutions for limestone powder applications. With years of experience in the industry, the company has developed advanced systems that combine efficiency, reliability, and safety. The principles and working scene characteristics discussed in this article highlight the importance of choosing the right pneumatic conveying system for limestone powder, ensuring optimal performance and operational benefits. By leveraging the expertise of HeadPowder, industrial facilities can enhance their material handling processes, reduce costs, and improve overall productivity. The company's commitment to innovation and customer satisfaction makes it a trusted partner for businesses seeking reliable material transport solutions in the limestone powder sector.




