Mobile powder conveyors are essential equipment in various industrial sectors, enabling efficient and reliable transportation of bulk powders. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality mobile powder handling solutions. This article delves into the working principle and key features of these systems, offering insights into their functionality and benefits.
Working Principle of Mobile Powder Conveyors
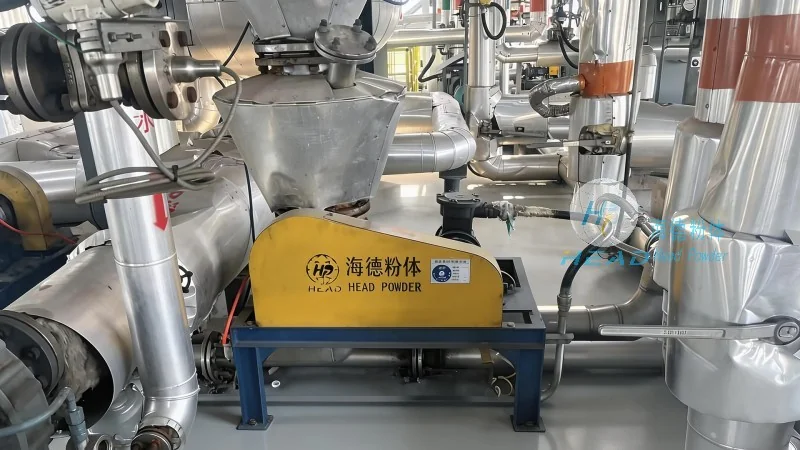
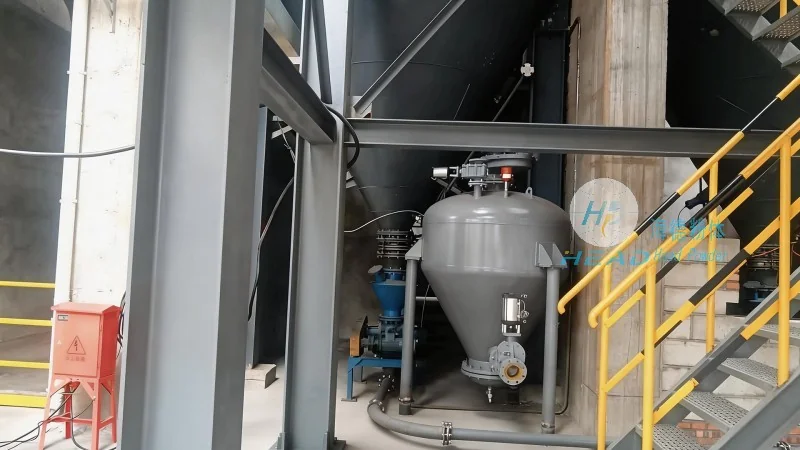
The operation of mobile powder conveyors typically involves a combination of mechanical and pneumatic systems designed to move powders from a source to a destination. The core mechanism often relies on a vacuum or pressure-driven air flow that draws or pushes the powder through a pipeline network. For instance, in a suction-based system, a fan or blower creates a negative pressure that pulls the powder from the loading point into the conveying line. The powder is then transported through the pipeline, often mixed with air, and discharged at the receiving end. Some systems may also incorporate mechanical components, such as screw conveyors or augers, to assist in the movement of the powder, especially in cases where the material is prone to clogging or requires additional mixing. The control system manages the flow rate, pressure, and direction of the conveying process, ensuring optimal performance and preventing issues like blockages or material degradation.
Key Features of Mobile Powder Conveyors
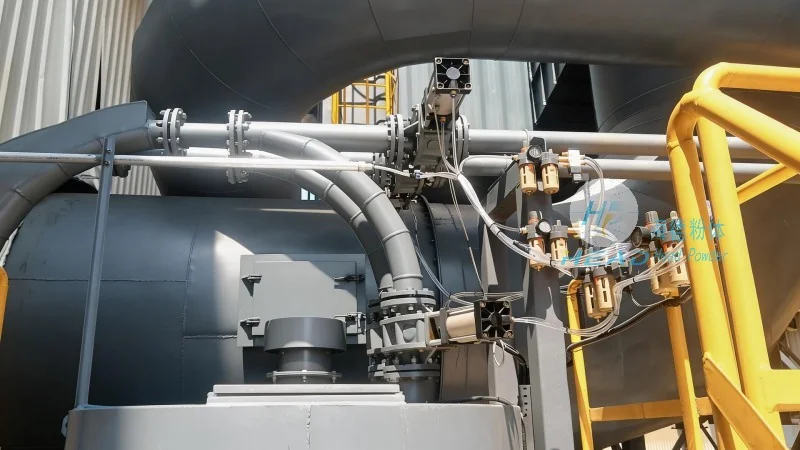
Mobile powder conveyors are distinguished by several key features that enhance their utility in industrial applications. Firstly, their mobility allows for flexible deployment across different production sites or work areas, eliminating the need for fixed infrastructure. This flexibility is particularly valuable in industries where production lines are temporary or require frequent reconfiguration. Secondly, these systems offer high efficiency in terms of material handling, capable of transporting large volumes of powders at consistent speeds. The design minimizes material loss and contamination, ensuring product integrity throughout the conveying process. Additionally, mobile powder conveyors are often equipped with advanced control technologies, such as variable frequency drives (VFDs) and sensors, which enable precise regulation of the conveying parameters and real-time monitoring of system performance. This leads to improved operational efficiency and reduced downtime. Another notable feature is their adaptability to various powder types, including fine powders, granules, and bulk materials, making them suitable for a wide range of applications. The robust construction and durable components ensure long-term reliability and low maintenance costs, contributing to overall cost-effectiveness.
About Shandong HeadPowder Engineering Co., Ltd.
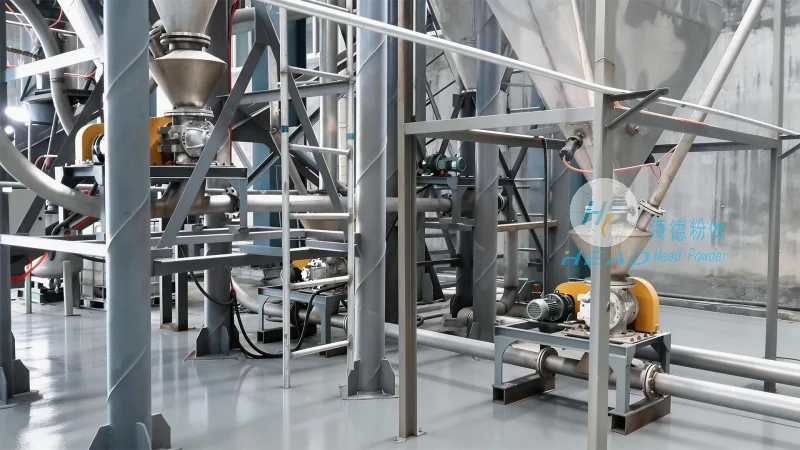
As a reputable manufacturer of mobile powder conveyors, Shandong HeadPowder Engineering Co., Ltd. is committed to delivering innovative and reliable solutions for powder handling challenges. With a strong focus on research and development, the company continuously improves its products to meet the evolving needs of the industry. HeadPowder's mobile powder conveyors are engineered with precision, incorporating advanced technologies and high-quality materials to ensure superior performance and durability. The company's dedication to customer satisfaction and technical excellence has established it as a trusted partner in the field of bulk material handling. Based in Shandong, China, HeadPowder serves clients globally, providing tailored solutions that enhance operational efficiency and productivity.




