Bulk bag unloading and powder material transport systems are critical components in industrial material handling, particularly for processing and transporting bulk powders efficiently. These systems are designed to handle large quantities of powders from bulk bags, ensuring safe and efficient transfer to storage or processing equipment. The technology behind these systems integrates mechanical, pneumatic, and sometimes hydraulic components to achieve seamless material flow while maintaining product integrity.
Structural Components and Operational Principles
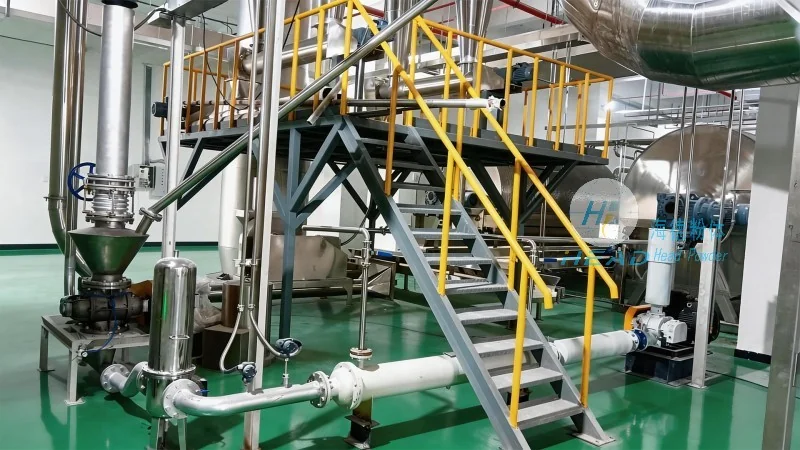
The core structure of a bulk bag unloading system typically includes several key components: a bulk bag support frame, a discharge valve or spout, a hopper or receiving container, and a conveying mechanism such as a screw conveyor, pneumatic conveyor, or bucket elevator. The support frame securely holds the bulk bag in place, preventing it from shifting during the unloading process. The discharge valve, often a bottom-discharge or top-discharge type, allows controlled release of the powder from the bag. The hopper collects the material and funnels it into the conveying system, which then transports the powder to the desired destination.
Pneumatic Conveying Systems: A Common Application
Pneumatic conveying is a widely used method in bulk bag unloading due to its ability to handle a variety of powder types, including fine, dusty, or abrasive materials. This system uses compressed air to create a flow of material through a pipeline. The powder is drawn from the bulk bag into the hopper and then propelled through the conveying line to the storage silo or processing unit. Pneumatic systems can be categorized into pressure and vacuum types, with pressure systems using positive pressure to push material and vacuum systems using negative pressure to pull it. The choice between these depends on factors like material properties, distance, and system layout.
Screw Conveyors: Mechanical Conveying Solutions
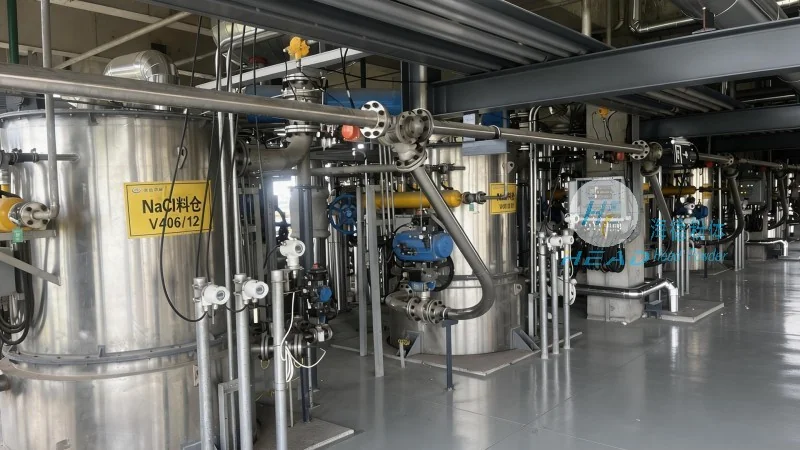
For applications requiring mechanical conveying, screw conveyors are a reliable option. These systems use a rotating screw (auger) to move powder through a trough or tube. Screw conveyors are suitable for handling dry, free-flowing powders and can be designed in various configurations, such as horizontal, vertical, or inclined, to suit different operational needs. They offer advantages like simplicity, low maintenance, and the ability to handle abrasive materials. However, they may not be suitable for very fine or dusty powders that could cause clogging or wear.
Ensuring Product Integrity and Safety
When handling powders, maintaining product integrity and ensuring operator safety are paramount. Bulk bag unloading systems are equipped with features to prevent dust generation, such as dust collection hoods and filtration systems. These systems capture airborne particles, reducing environmental contamination and protecting workers from inhalation hazards. Additionally, the design of the discharge valve and conveying components minimizes material degradation, ensuring that the powder remains in its original state throughout the handling process.
Applications in Various Industries
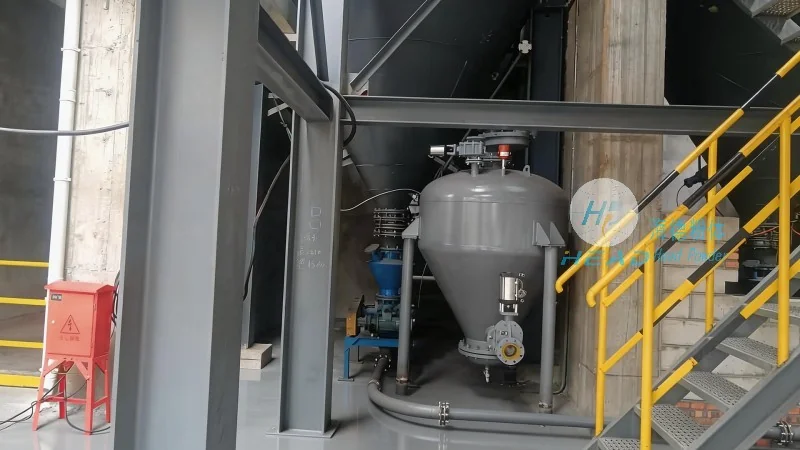
Bulk bag unloading and powder transport systems are utilized across multiple industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, these systems are essential for handling active pharmaceutical ingredients (APIs) and excipients, where contamination control and product purity are critical. In the food industry, they are used for processing ingredients like flour, sugar, and spices, ensuring that the final product meets safety and quality standards. The chemical industry relies on these systems for handling raw materials and intermediates, while the mining sector uses them to transport minerals and ores from bulk bags to processing facilities.
Customization and Integration with Existing Systems
HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in designing and manufacturing customized bulk bag unloading and powder transport systems. The company's expertise lies in tailoring solutions to meet specific operational requirements, including material type, processing capacity, and environmental considerations. Their systems can be integrated with existing production lines or designed as standalone units, providing flexibility for different industrial setups. The company's commitment to quality and innovation ensures that their products are durable, efficient, and compliant with industry standards.




