Smart bulk bag unloading and powder material handling systems represent a critical advancement in industrial material processing, particularly for companies dealing with bulk powders. These systems are designed to efficiently transfer materials from bulk bags (also known as super sacks or FIBCs) into processing equipment, storage silos, or other handling systems. The technology integrates advanced engineering principles to ensure safe, reliable, and automated operation, addressing the challenges associated with traditional manual or semi-automated unloading methods.
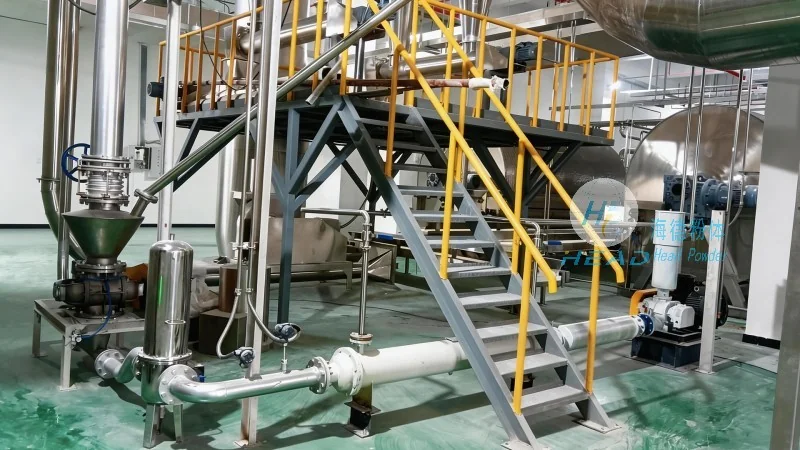
Overview of Smart Bulk Bag Unloading Systems
Smart bulk bag unloading systems are engineered to streamline the process of handling bulk powders, which are commonly used in industries such as food, pharmaceuticals, chemicals, and agriculture. These systems typically consist of a hopper, a discharge valve, and a conveyor or feeding mechanism that connects the bulk bag to the downstream processing equipment. The key advantage of these systems lies in their ability to automate the unloading process, reducing labor costs, minimizing material loss, and enhancing operational safety.
Structural Principles of Smart Bulk Bag Unloading Equipment
The structural design of smart bulk bag unloading systems is based on several fundamental principles to ensure optimal performance. The primary components include a bulk bag support frame, a discharge mechanism (often a rotary valve or a pneumatic or hydraulic actuator), and a material transfer system (such as a screw conveyor or a pneumatic conveyor). The support frame is designed to securely hold the bulk bag in place, while the discharge mechanism controls the flow rate of the material. The material transfer system then transports the powder to the desired destination. Additionally, these systems often incorporate features like level sensors, pressure relief valves, and dust collection systems to enhance safety and efficiency.
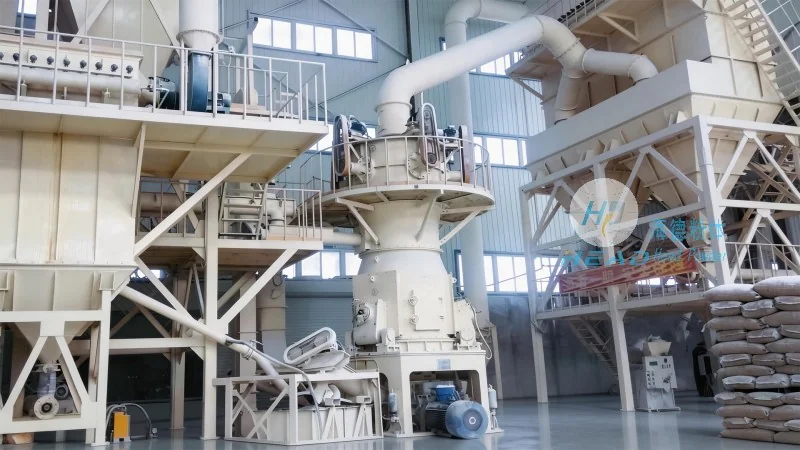
Working Mechanisms and Operational Efficiency
The working mechanisms of smart bulk bag unloading systems involve a sequence of automated steps. Initially, the bulk bag is placed onto the support frame, and the system's sensors detect the bag's position and weight. Once the bag is properly positioned, the discharge valve is activated, allowing the material to flow into the hopper. The material transfer system then moves the powder to the processing equipment or storage silo. The system may also include features like bag emptying indicators, which signal when the bag is fully emptied, and automatic shut-off valves to prevent overfilling or material spillage. This automated process significantly reduces the time and labor required for unloading, while maintaining high levels of accuracy and safety.
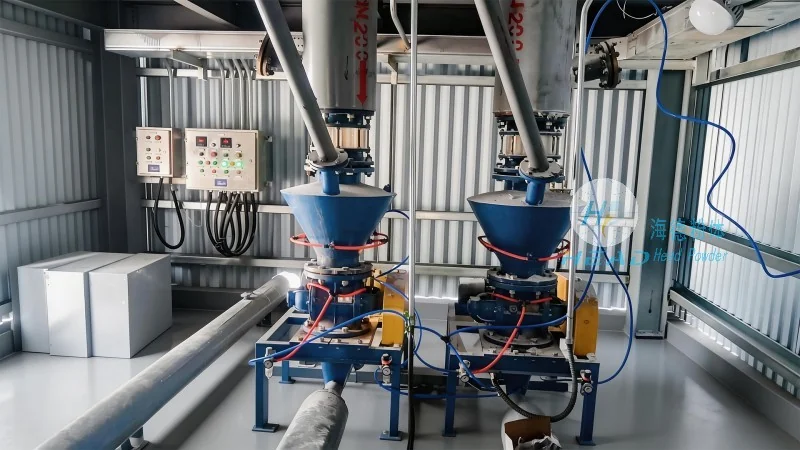
Key Features and Advantages of Smart Bulk Bag Unloading Systems
Smart bulk bag unloading systems offer several advantages over traditional methods. These include improved material handling efficiency, reduced labor costs, enhanced safety through automated operations, and minimized material loss due to precise control of the discharge process. Additionally, these systems are designed to handle a wide range of powder characteristics, including different densities, flowabilities, and moisture contents. The integration of sensors and control systems allows for real-time monitoring and adjustment of the unloading process, ensuring consistent performance and product quality. Furthermore, the modular design of these systems allows for easy integration with existing processing lines, making them a versatile solution for various industrial applications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of advanced powder handling equipment. The company specializes in the design, development, and production of smart bulk bag unloading systems and other powder processing solutions. HeadPowder's products are engineered to meet the specific needs of various industries, providing reliable and efficient solutions for bulk powder handling. The company is committed to innovation and quality, with a focus on delivering products that enhance operational efficiency and safety. HeadPowder's headquarters is located in Shandong, China, where the company operates a state-of-the-art manufacturing facility and a research and development center. The company's team of experienced engineers and technicians ensures that each product meets the highest standards of performance and durability.




