Mineral sand powder conveying systems are critical in industrial processes, particularly for transporting fine particulate materials like mineral sands. These systems are engineered to move bulk materials efficiently from one location to another while preserving the material's integrity and quality. The technology integrates mechanical engineering with material handling expertise to ensure reliable and consistent operation across various industrial applications.
Key Components and Structural Design
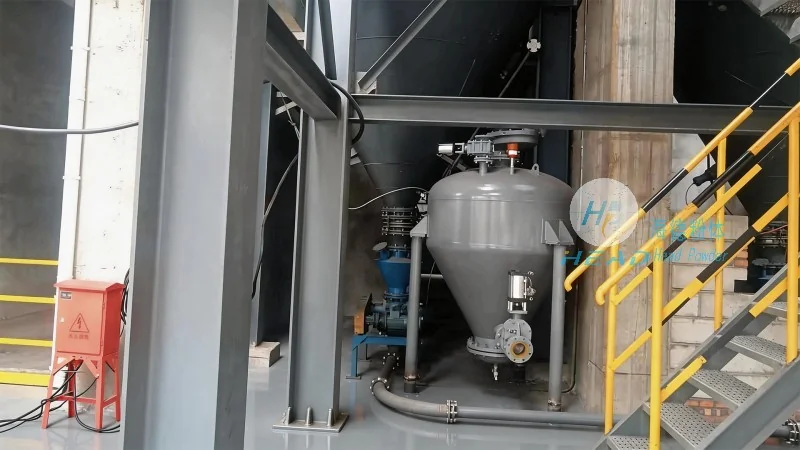
The fundamental components of a mineral sand powder conveying system include the feeding mechanism, conveying pipeline, drive system, and control unit. The feeding mechanism, typically a hopper or rotary valve, ensures a steady material flow into the system. The conveying pipeline—often metal or flexible hoses—is tailored to handle mineral sand characteristics such as particle size, density, and moisture content. The drive system, an electric motor with a gearbox, provides the necessary power to move material through the pipeline. The control unit, equipped with sensors and a programmable logic controller (PLC), monitors performance and adjusts parameters to maintain optimal operation.
Working Principles and Operational Mechanisms
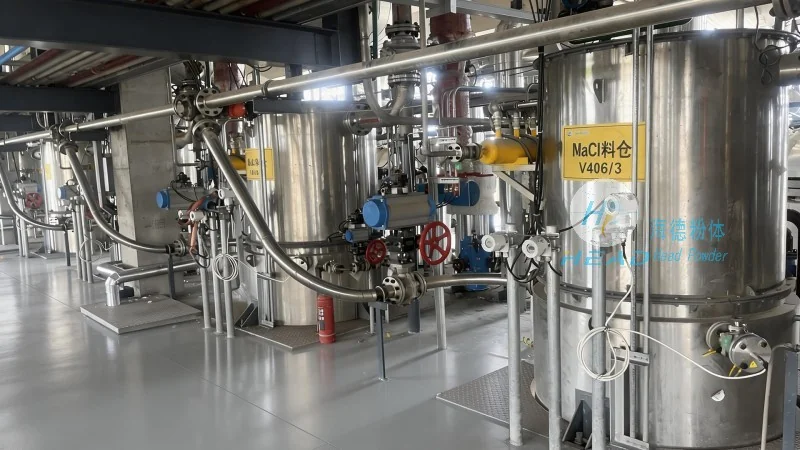
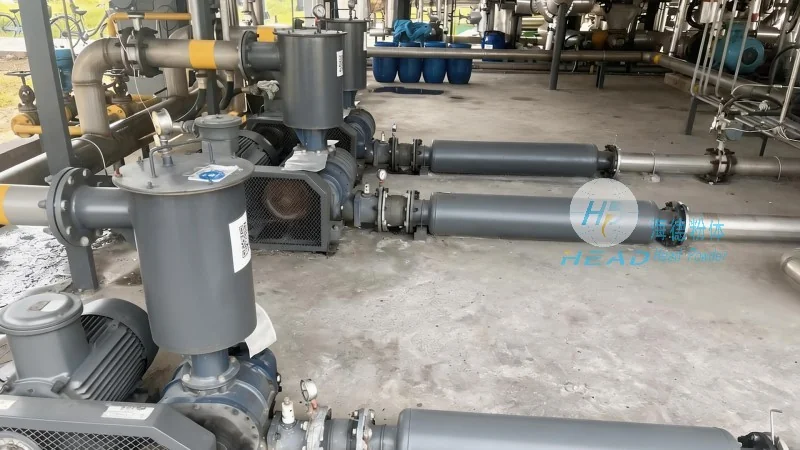
The operation of these systems follows core principles, with common methods including pneumatic and mechanical conveying. Pneumatic conveying uses compressed air to suspend and transport material through a pipeline, while mechanical conveying employs screw or belt conveyors. The choice depends on material properties, distance, and flow rate. Both methods aim to minimize degradation, prevent blockages, and enhance energy efficiency. The systems are designed to handle abrasive or corrosive materials, making them suitable for diverse industries like mining, chemical processing, and food production.
Advantages and Industrial Applications
Mineral sand powder conveying systems offer significant advantages, including automated, continuous material transport that reduces manual handling risks. They accommodate a wide range of materials and can integrate with other equipment (e.g., classifiers, dryers) to form complete production lines. For industries reliant on mineral sand processing, these systems boost productivity and lower operational costs. The reliability and efficiency of such systems are vital for maintaining competitiveness in modern industrial settings.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
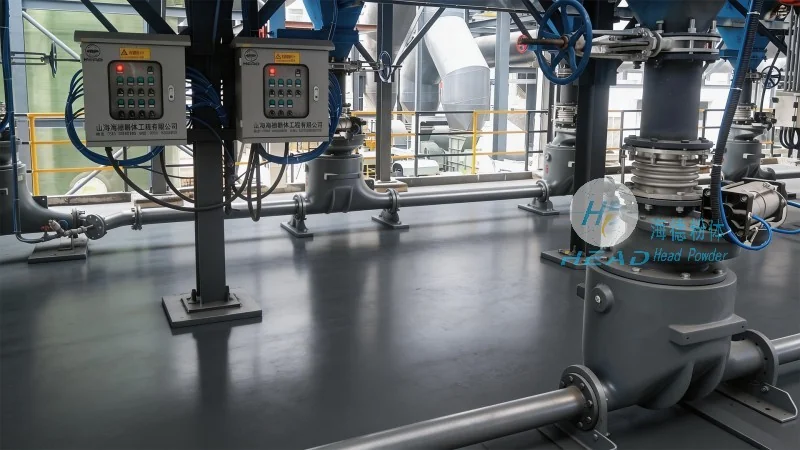
Shandong HeadPowder Engineering Co., Ltd., branded as headpowder, is a leading manufacturer and supplier of mineral sand powder conveying systems. Headquartered in Shandong, China, the company has built a strong reputation for innovative, reliable solutions. With extensive industry experience, headpowder offers tailored conveying solutions to meet client needs. The company's commitment to quality and customer satisfaction has established it as a trusted partner for businesses requiring efficient material handling across sectors like mining and chemical processing.




