HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust collection powder conveying systems. These systems are engineered to efficiently handle and transport fine powders and dust from industrial processes, ensuring optimal performance and reliability in various applications. This article will explore the working principle and key features of such equipment, highlighting how they contribute to improved operational efficiency and safety.
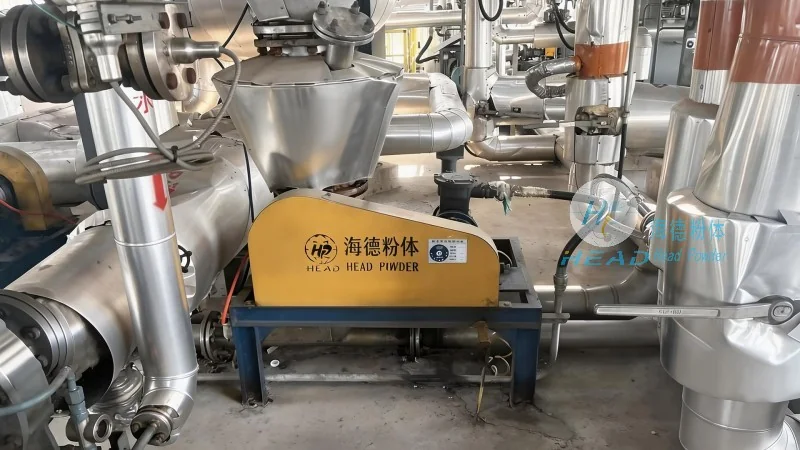
Working Principle of the Dust Collection Powder Conveying System
The dust collection powder conveying system operates by integrating several components to create a closed-loop or semi-closed-loop system for material handling. At its core, the system typically includes a dust collector, a conveying device (such as a pneumatic or mechanical conveyor), and associated control mechanisms. The process begins with the dust or powder being generated in an industrial setting, such as a manufacturing or processing plant. The dust collector then captures the airborne particles, separating them from the air stream and collecting them in a hopper or container. Once collected, the powder is transferred to the conveying system, which then transports the material to its designated destination, such as a storage silo, processing unit, or disposal area.
For pneumatic conveying systems, compressed air is used to create a flow that propels the powder through a network of pipes. The air pressure and flow rate are carefully controlled to ensure the material is moved smoothly without causing excessive wear or degradation. Mechanical conveyors, on the other hand, use rotating components like screws or belts to transport the powder, often in a more direct and contact-based manner. Both methods are designed to maintain the integrity of the powder, preventing clumping or agglomeration during transport. The system also incorporates sensors and controls to monitor pressure, flow, and material levels, allowing for real-time adjustments to maintain optimal performance.
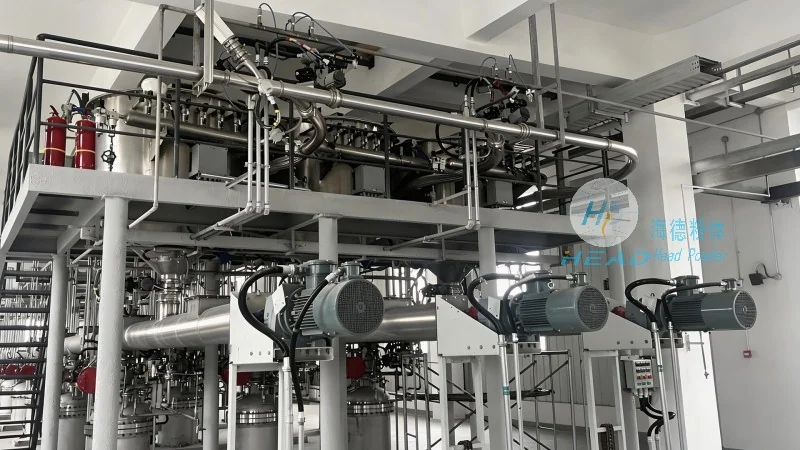
Key Features of the Dust Collection Powder Conveying System
HeadPowder's dust collection powder conveying systems are characterized by several notable features that enhance their functionality and user experience. One of the primary advantages is their high efficiency in material handling, capable of transporting large volumes of powder with minimal energy consumption. The systems are designed to minimize material loss and contamination, ensuring that the transported powder remains clean and free from foreign particles. This is particularly important in industries where product purity is critical, such as pharmaceuticals, food processing, or chemical manufacturing.
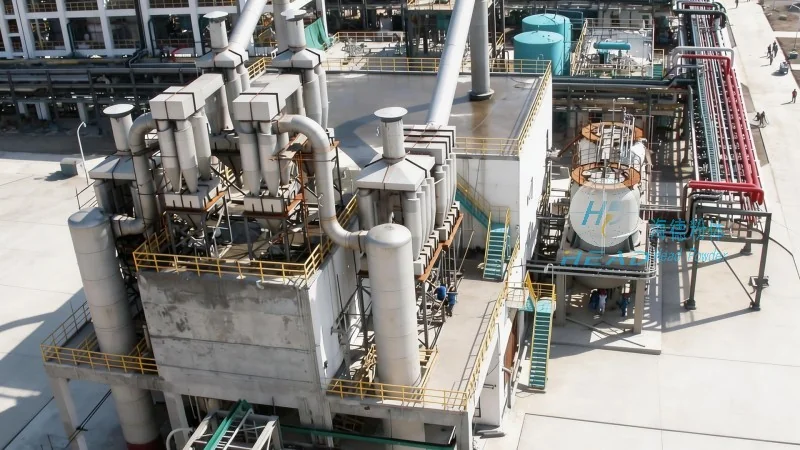
Another key feature is the system's adaptability to different powder types and particle sizes. Whether dealing with fine powders, coarse granules, or sticky materials, the equipment can be customized to meet specific operational requirements. This flexibility allows users to integrate the system into existing processes without significant modifications, reducing downtime and installation costs. The systems also prioritize safety, incorporating features like explosion-proof designs for hazardous environments and overpressure protection to prevent accidents. Additionally, the equipment is built with durable materials, such as stainless steel or corrosion-resistant alloys, to withstand harsh industrial conditions and extend service life.
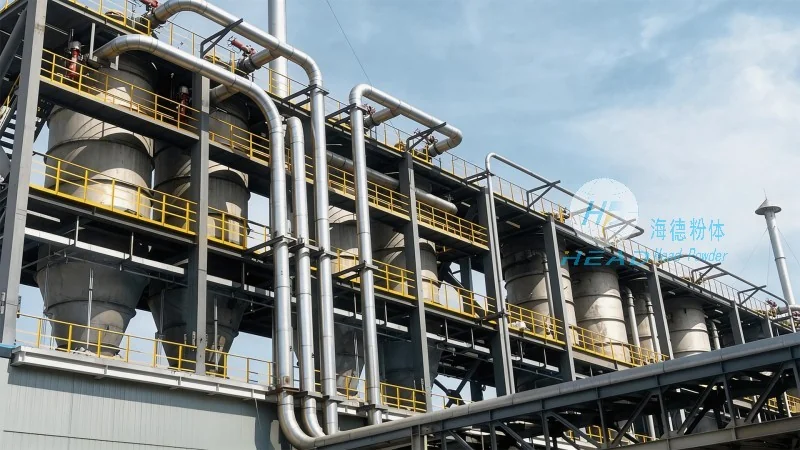
Furthermore, the dust collection powder conveying systems from HeadPowder are equipped with advanced control systems that enable remote monitoring and operation. Users can access real-time data on system performance, including flow rates, pressure, and material levels, through user-friendly interfaces. This allows for proactive maintenance and troubleshooting, reducing downtime and increasing overall productivity. The systems are also designed for easy maintenance, with accessible components and clear documentation, making it simple for operators to perform routine checks and repairs.
In summary, the dust collection powder conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. combine advanced technology with robust design to provide efficient and reliable solutions for powder handling. By understanding the working principle and key features of these systems, users can make informed decisions about integrating them into their industrial processes, ultimately improving operational efficiency and safety.




