For industries dealing with bulk materials like distillers grains, efficient and reliable material handling is crucial. Pneumatic conveying systems offer a solution that enhances operational efficiency while ensuring product integrity. This article explores the application of pneumatic conveying in the bulk handling of distillers grains, highlighting the technology's benefits and practical implementation.
Understanding Pneumatic Conveying Systems
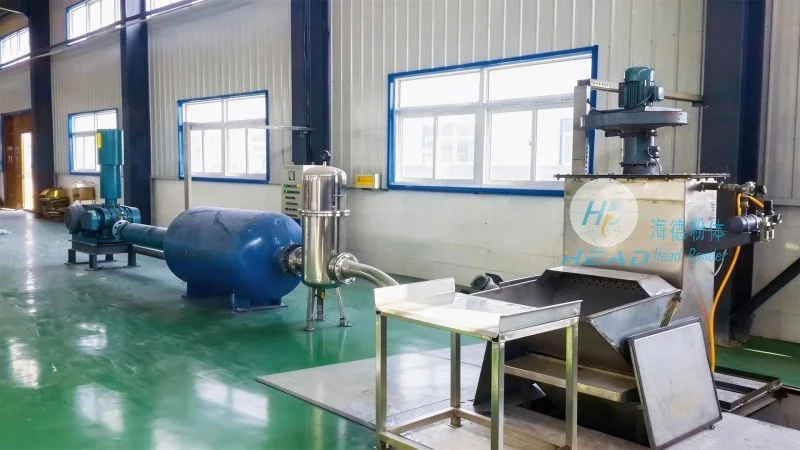
Pneumatic conveying uses pressurized air or vacuum to transport dry bulk materials through a pipeline. The system typically consists of a hopper for material storage, a conveyor line, and a receiver for the discharged material. There are two main types: pressure and vacuum systems. Pressure systems push material through the pipeline using compressed air, while vacuum systems draw material into the line using a vacuum pump. Each type has advantages depending on the material characteristics and distance to be covered.
Application in Distillers Grains Handling
Distillers grains, a byproduct of ethanol production, are often handled in large quantities. Traditional methods like belt conveyors or bucket elevators may face challenges with material flow, dust generation, and contamination risks. Pneumatic conveying provides a more hygienic and controlled approach. The system can transport distillers grains from storage silos to processing units or for further use in animal feed production. The ability to handle fine powders and maintain a closed system reduces the risk of dust exposure and cross-contamination, which is critical in food and feed industries.
Key Features and Benefits
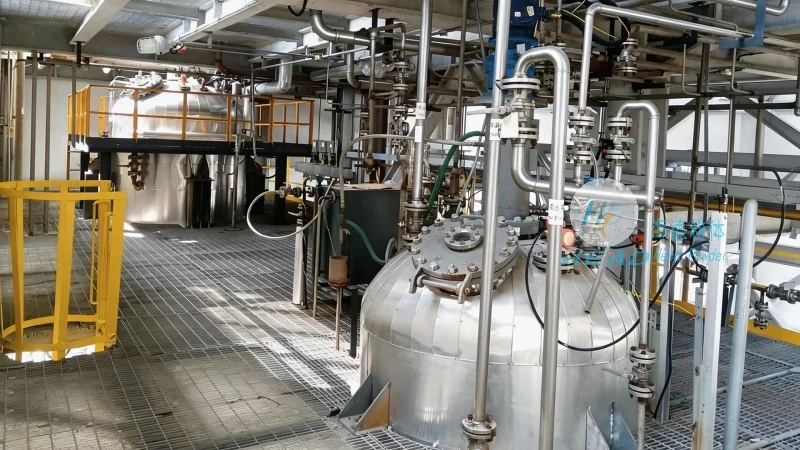
The pneumatic conveying system for distillers grains offers several key benefits. Firstly, it ensures a continuous and uniform flow of material, minimizing downtime and improving production throughput. Secondly, the enclosed pipeline design prevents dust from entering the environment, enhancing workplace safety and compliance with environmental regulations. Thirdly, the system can handle varying material densities and moisture contents without clogging, making it versatile for different processing stages. Additionally, the technology reduces the need for manual handling, lowering labor costs and the risk of human error in material transfer.
System Components and Design Considerations
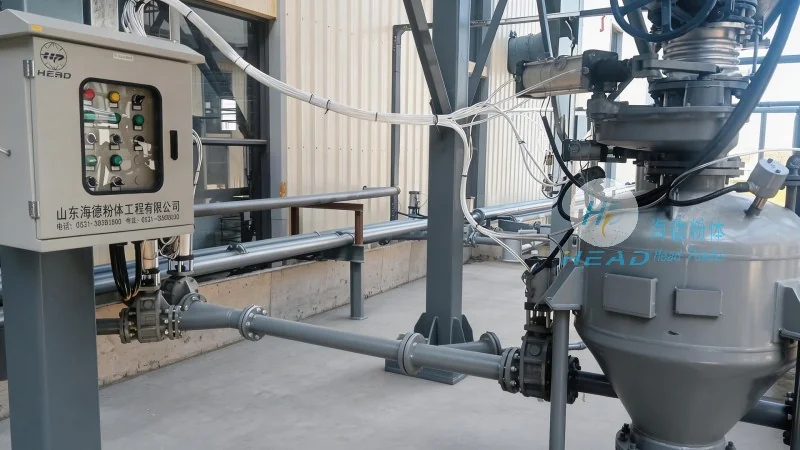
The effectiveness of a pneumatic conveying system depends on proper component selection and design. Key components include the hopper, which must be designed to prevent material bridging and ensure consistent feed. The conveyor line, typically made of stainless steel or other corrosion-resistant materials, is chosen based on the material's abrasiveness and moisture content. The receiver or discharge hopper is designed to collect the material smoothly and prevent re-entrainment of dust. Design considerations also include the air velocity required to transport the material, which must be sufficient to overcome friction and gravity but not so high as to cause excessive energy consumption or material degradation. Proper sizing of the air compressor or vacuum pump is essential to maintain the required pressure or vacuum levels throughout the system.
Operational Efficiency and Maintenance
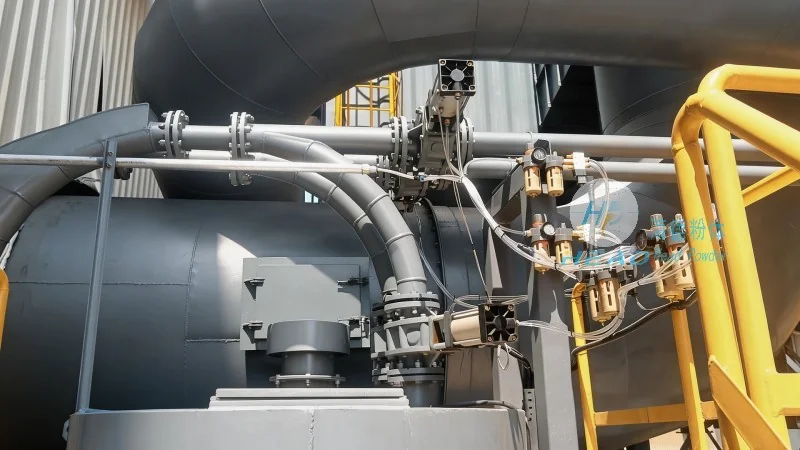
Operational efficiency is a primary concern when implementing a pneumatic conveying system. Regular maintenance is crucial to ensure the system operates at optimal performance. This includes checking for leaks in the pipeline, cleaning the hopper and receiver to prevent material buildup, and inspecting the air compressor or vacuum pump for wear and tear. The use of filters and cyclones in the system helps to remove dust and debris from the air stream, protecting the equipment and maintaining air quality. Proper maintenance schedules, based on the system's usage and material characteristics, can extend the lifespan of the equipment and reduce long-term operational costs.
Conclusion
Pneumatic conveying systems provide an efficient and reliable solution for the bulk handling of distillers grains. By leveraging pressurized air or vacuum to transport materials, these systems enhance operational efficiency, maintain product quality, and improve workplace safety. For companies in the ethanol and animal feed industries, investing in a well-designed pneumatic conveying system can lead to significant improvements in productivity and cost-effectiveness. With proper component selection, design, and maintenance, pneumatic conveying remains a preferred technology for handling distillers grains and other bulk materials.




