Pharmaceutical pneumatic conveying equipment is a specialized system engineered for the safe and efficient transport of powders and bulk materials within pharmaceutical manufacturing environments. These systems are critical in ensuring compliance with stringent regulatory standards, such as those set by the FDA and GMP (Good Manufacturing Practice), which require precise control over material handling to prevent contamination and maintain product integrity. The equipment is designed to handle sensitive pharmaceutical powders, including active pharmaceutical ingredients (APIs), excipients, and other raw materials, while minimizing the risk of cross-contamination and ensuring consistent product quality.
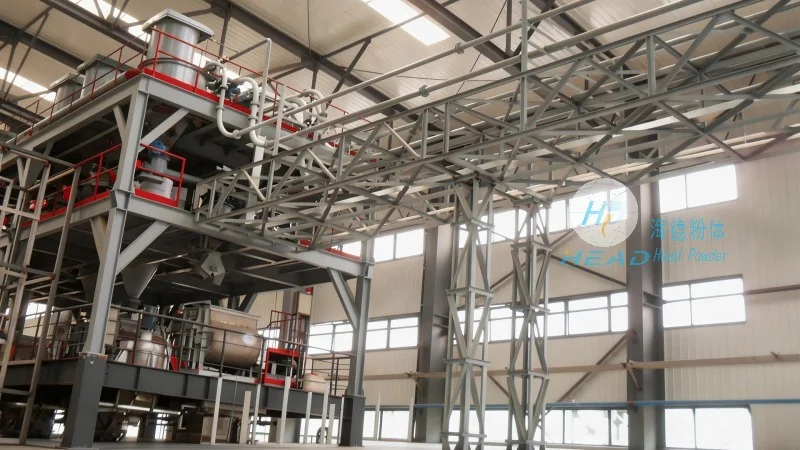
Key Components of Pharmaceutical Pneumatic Conveying Systems
The structure of a pharmaceutical pneumatic conveying system typically consists of several key components that work in tandem to achieve reliable material transport. These components include the hopper or feeder, which holds the bulk material and regulates its flow into the system; the conveying line, which can be either positive pressure or negative pressure (or a combination of both), depending on the application; the air compressor or vacuum pump, which provides the necessary pressure or suction to move the material; and the separation or collection equipment, such as cyclones or filters, which separate the conveyed material from the air stream and return it to the process or storage.
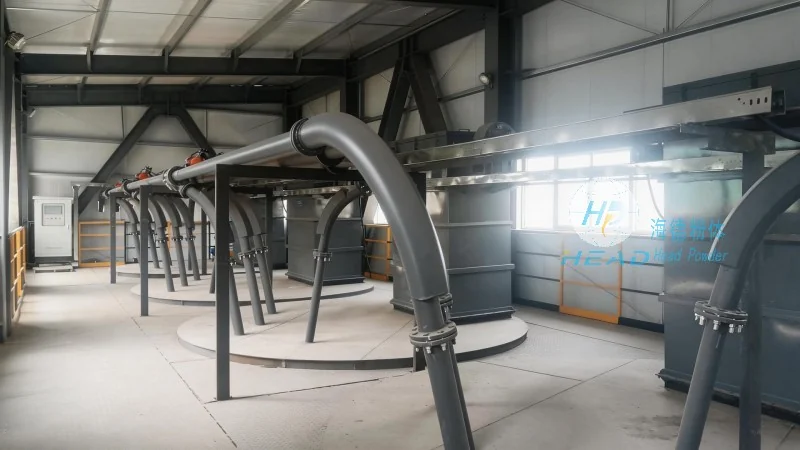
How Pharmaceutical Pneumatic Conveying Works: The Principle of Operation
The operation of pharmaceutical pneumatic conveying systems is based on the fundamental principle of using air to transport solid particles. In positive pressure systems, compressed air is introduced into the conveying line, creating a pressure differential that pushes the material forward. The material is suspended in the air stream as it travels through the line, and the air velocity is carefully controlled to prevent particle degradation or agglomeration. In negative pressure systems, a vacuum is created at the receiving end, drawing the material through the line. Both systems rely on precise control of air flow, pressure, and velocity to ensure efficient and gentle handling of the powder.
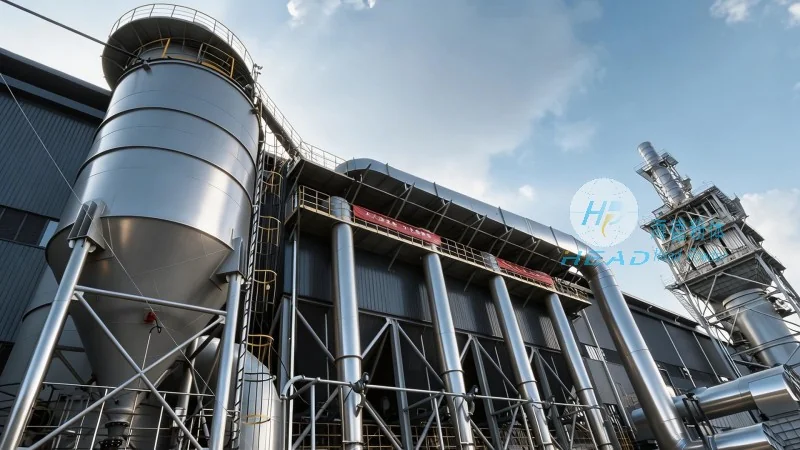
Benefits of Using Pharmaceutical Pneumatic Conveying Equipment
Implementing pharmaceutical pneumatic conveying equipment offers numerous advantages for pharmaceutical manufacturers. One of the primary benefits is the ability to handle sensitive materials without the need for mechanical contact, which reduces the risk of contamination and product degradation. The system also provides a closed-loop operation, minimizing dust emissions and environmental impact, which is essential for maintaining cleanroom standards. Additionally, pneumatic conveying systems offer flexibility in material handling, allowing for the transport of powders over long distances and through complex layouts without the need for multiple transfer points. This reduces downtime and improves overall operational efficiency.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer of pharmaceutical pneumatic conveying equipment. With a focus on innovation and adherence to industry standards, the company specializes in designing and manufacturing systems tailored to the unique needs of the pharmaceutical sector. HeadPowder's products are engineered to meet the highest regulatory requirements, ensuring safety, reliability, and performance in pharmaceutical manufacturing environments. The company's commitment to quality and customer satisfaction has established it as a trusted partner for pharmaceutical companies seeking advanced powder handling solutions.
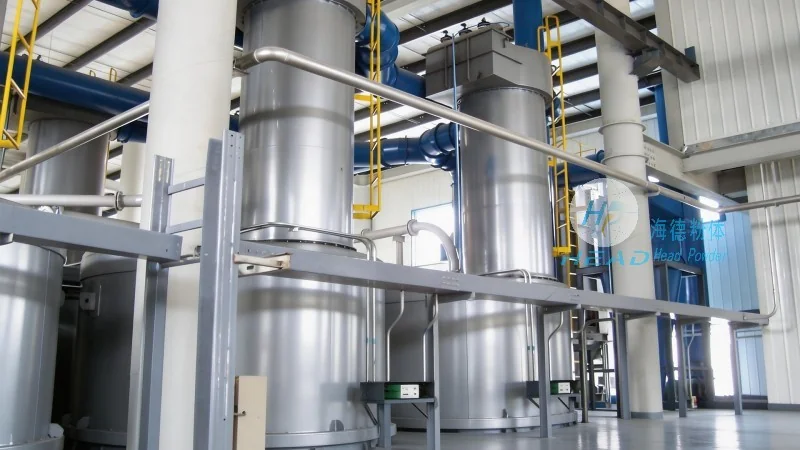
Conclusion: The Importance of Reliable Pharmaceutical Pneumatic Conveying Systems
In conclusion, pharmaceutical pneumatic conveying equipment plays a vital role in modern pharmaceutical manufacturing, providing a safe, efficient, and compliant method for handling powders and bulk materials. The structure and principle of these systems are designed to meet the stringent demands of the industry, ensuring product integrity and regulatory compliance. As a leader in the field, Shandong HeadPowder Engineering Co., Ltd. continues to advance the technology and provide solutions that enhance operational efficiency and product quality in pharmaceutical production. By investing in reliable pneumatic conveying systems, pharmaceutical manufacturers can ensure the safety and effectiveness of their products while maintaining competitive advantages in the market.




