Efficient and reliable transportation of bulk powders like sulfur is crucial in industrial processes. Pneumatic conveying systems offer a solution that minimizes material loss, reduces contamination risks, and enhances operational safety compared to traditional methods such as belt conveyors or bucket elevators. This article explores the principles and applications of sulfur pneumatic conveying, highlighting how specialized equipment from Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions headquartered in Shandong, China, can optimize material handling in sulfur processing facilities.
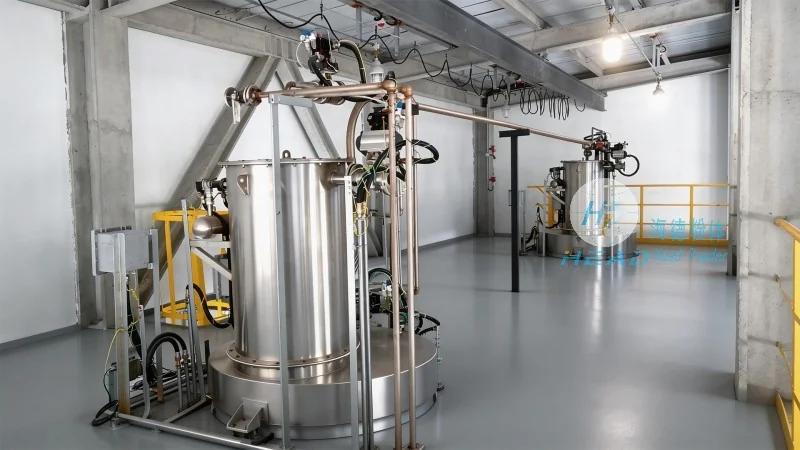
Understanding Pneumatic Conveying for Sulfur Handling
Pneumatic conveying utilizes air flow to transport solid materials through a pipeline system. In the case of sulfur, which is often in powder or granular form, this method ensures a clean, dust-free transfer that aligns with stringent industrial standards. The process typically involves a blower or compressor that generates the necessary air pressure to move the material. The system can be categorized into two main types: dilute phase and dense phase, each offering distinct advantages depending on the material characteristics and distance of transport.
Key Components of a Sulfur Pneumatic Conveying System
At the core of any effective sulfur pneumatic conveying system are several critical components. The blower or compressor provides the driving force, generating the air pressure required to move the material. Hoppers or feeders are used to introduce the sulfur into the system, ensuring a consistent flow. The pipeline network connects the various components, including bends, elbows, and straight sections, which are designed to minimize pressure loss and maintain material velocity. At the receiving end, a separator or cyclone separates the sulfur from the air, allowing for safe discharge into storage or processing units. Additionally, filters and dust collection systems are essential to maintain air quality and comply with environmental regulations.
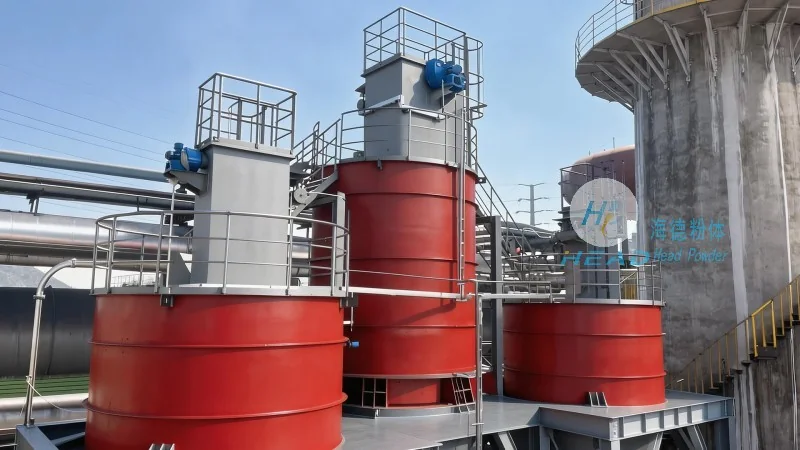
Advantages of Pneumatic Conveying for Sulfur
Compared to conventional material handling methods, pneumatic conveying offers several advantages for sulfur transport. One of the most significant benefits is the reduction of material degradation and contamination. Unlike mechanical systems that may cause abrasion or introduce foreign particles, pneumatic systems keep the sulfur in a controlled environment, preserving its quality for downstream processes. This is particularly important in sulfur applications where purity is critical, such as in the production of sulfuric acid or other chemical derivatives. Furthermore, pneumatic conveying systems are highly flexible, allowing for easy integration into existing industrial layouts and enabling changes in material flow direction without major modifications.
Applications in Sulfur Processing Facilities
Sulfur pneumatic conveying is widely used in various stages of sulfur processing. In mining operations, it is employed to transport raw sulfur from storage silos to processing units, ensuring a continuous supply of material. During the refining process, the system can handle sulfur in different forms, from fine powders to larger granules, adapting to the varying characteristics of the material. In chemical plants, pneumatic conveying is used to move sulfur to reactors or reactors, where it is used as a raw material in the production of sulfur compounds. The ability to handle both dry and slightly moist sulfur makes this system versatile for diverse industrial applications.
Customization and Scalability: Tailoring Solutions by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of sulfur handling facilities. The company understands that each industrial application has unique requirements, such as varying sulfur properties, transport distances, and environmental constraints. By leveraging advanced engineering and years of industry experience, HeadPowder provides solutions that optimize efficiency, reduce operational costs, and enhance safety. The company’s team of experts works closely with clients to assess their material handling challenges and develop tailored systems that meet their specific needs. Whether it's a small-scale operation or a large industrial plant, HeadPowder offers scalable solutions that can be expanded or modified as the facility grows.
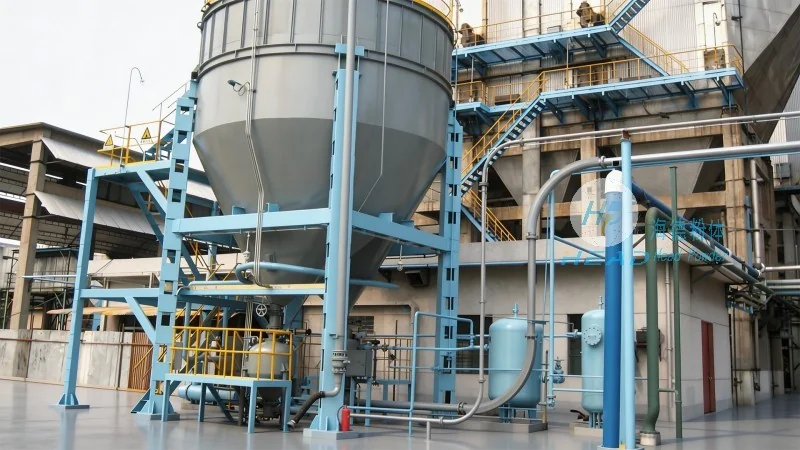
Ensuring Reliability and Longevity: Maintenance and Support
Reliability is a top priority in sulfur pneumatic conveying systems, as any downtime can disrupt production and lead to significant financial losses. Shandong HeadPowder Engineering Co., Ltd. emphasizes the importance of regular maintenance and provides comprehensive support to ensure the longevity of their systems. The company offers maintenance services, including routine inspections, component replacement, and troubleshooting. By adhering to manufacturer-recommended maintenance schedules, clients can minimize the risk of system failures and extend the lifespan of their equipment. Additionally, HeadPowder provides technical support and training to help facility operators maintain optimal performance and troubleshoot issues efficiently.
Conclusion: Enhancing Efficiency in Sulfur Handling with Pneumatic Conveying
Pneumatic conveying represents a sophisticated and efficient method for transporting sulfur and other bulk powders. By leveraging the principles of air flow and specialized equipment, this technology offers significant advantages over traditional material handling methods. The systems provided by Shandong HeadPowder Engineering Co., Ltd. are designed to meet the highest standards of performance, reliability, and safety, ensuring that sulfur processing facilities can operate at peak efficiency. As industries continue to demand more efficient and sustainable material handling solutions, pneumatic conveying remains a key technology in optimizing sulfur handling processes.




