Introduction to Cornstarch Pneumatic Conveying Equipment: Structure and Working Principle
Release time:2026-09-22 00:01:33
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional manufacturer specializing in the design, development, and production of pneumatic conveying equipment. The company is headquartered in Shandong, China, and has established a strong reputation in the industry for its high-quality products and reliable service. With years of experience in the field, headpowder focuses on providing customized solutions for various material handling needs, particularly in the processing of powders and granules.
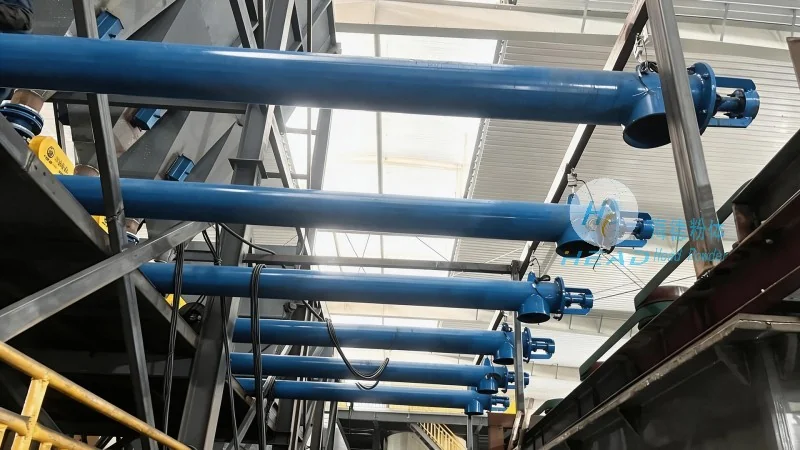
Cornstarch Pneumatic Conveying Equipment Overview
The cornstarch pneumatic conveying equipment produced by headpowder is specifically designed for the efficient and safe transportation of cornstarch and similar powders. This equipment utilizes pneumatic technology to move materials through a pipeline system, eliminating the need for traditional mechanical conveyors that may cause contamination or material degradation. The system is equipped with advanced control mechanisms to ensure precise flow rates and consistent material handling, making it ideal for applications in food processing, pharmaceuticals, and other industries where product purity is critical.
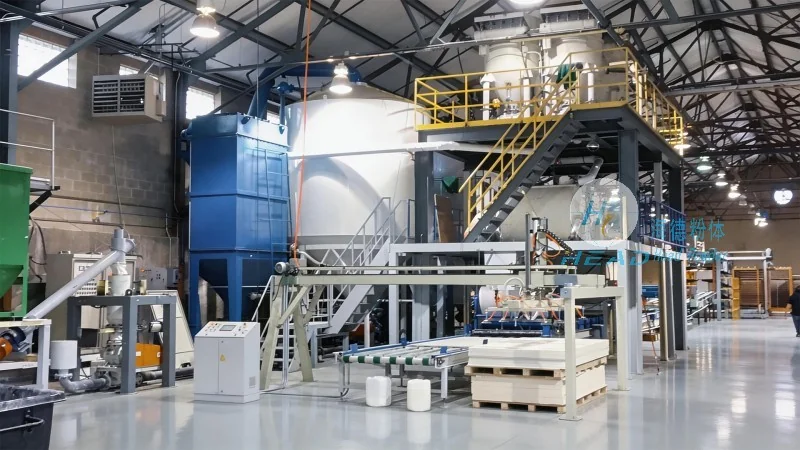
Structure and Working Principle of the Pneumatic Conveying System
The cornstarch pneumatic conveying machine consists of several key components, each playing a crucial role in the overall operation. The main parts include a hopper for material storage, a rotary valve for controlled material discharge, a pipeline system for material transport, and a dust collector to ensure air filtration and environmental compliance. The working principle involves the creation of a low-pressure or high-pressure air flow within the pipeline. When the material is discharged from the hopper into the pipeline, the air flow entrains the powder particles, carrying them to the destination point. The system can operate in both dilute-phase and dense-phase modes, allowing for flexibility in handling different material properties and flow rates.
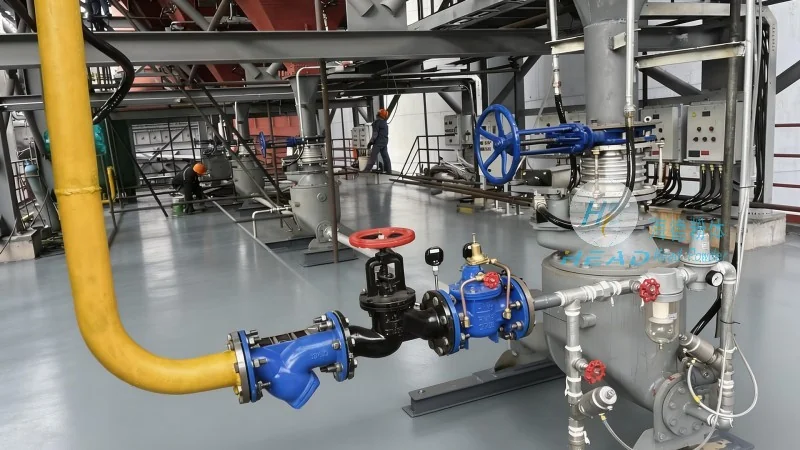
Advantages and Performance Characteristics
Headpowder's cornstarch pneumatic conveying equipment offers several advantages over traditional conveying methods. Firstly, it provides a clean and hygienic conveying process, which is essential for food-grade applications. The system minimizes product contamination and reduces the risk of dust explosions by using sealed pipelines and effective dust control measures. Secondly, the equipment is highly efficient, with low energy consumption and minimal maintenance requirements. The advanced control systems allow for real-time monitoring and adjustment of the conveying process, ensuring optimal performance and reducing downtime. Additionally, the modular design of the equipment enables easy installation and integration into existing production lines, making it a cost-effective solution for businesses looking to upgrade their material handling capabilities.




