Headpowder, the abbreviation for Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of air-pneumatic conveying systems. The company is headquartered in Shandong, China, and specializes in designing, manufacturing, and delivering advanced environmental air-pneumatic conveying solutions. With a focus on innovation and quality, Headpowder aims to provide efficient and sustainable material handling systems for various industries.
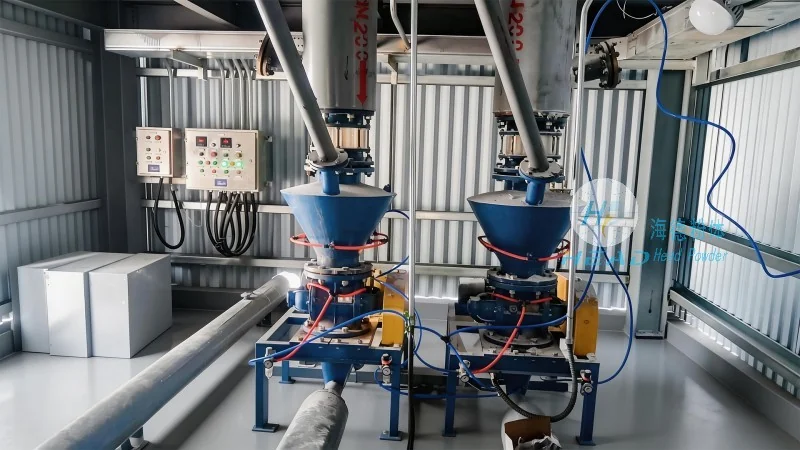
Understanding Air-Pneumatic Conveying Systems
At the heart of Headpowder's offerings are air-pneumatic conveying systems, which utilize compressed air to transport bulk materials from one location to another. This technology offers a clean, dust-free, and efficient method for handling a wide range of materials, including powders, granules, and small particles. The core principle involves creating a flow of air through a pipeline, which draws the material into the system and transports it to the desired destination. This approach eliminates the need for traditional mechanical components like belts or buckets, reducing maintenance and operational costs.
Structural Components and Working Principles
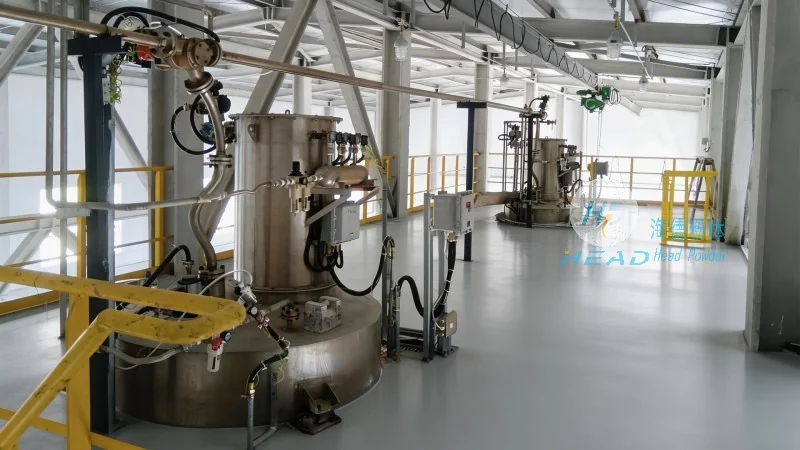
The structure of an air-pneumatic conveying system typically consists of several key components, each playing a crucial role in the overall operation. The main parts include a material hopper, an air compressor, a pipeline network, and a discharge outlet. The material hopper serves as the storage container, where the bulk material is loaded. The air compressor generates the necessary pressure to move the material through the pipeline. The pipeline network connects the hopper to the discharge point, with various fittings and valves to control the flow. The discharge outlet is where the material is released into the final destination, such as a silo or processing unit. The system operates by first loading the material into the hopper, then activating the air compressor to create a pressure differential. This pressure differential draws the material into the pipeline, where it is carried by the air flow to the discharge point. The entire process is automated, ensuring consistent and reliable material transport.
Environmental Benefits and Advantages
One of the primary advantages of air-pneumatic conveying systems is their environmental friendliness. Unlike traditional mechanical systems, which often generate dust and require frequent cleaning, air-pneumatic systems operate in a sealed environment, minimizing dust emissions and improving workplace safety. This makes them ideal for industries where air quality and worker health are critical concerns. Additionally, the systems are energy-efficient, as they use compressed air to move materials, reducing the need for additional machinery and lowering operational costs. The sealed design also prevents material contamination, ensuring that the transported goods remain clean and free from external pollutants. For companies looking to enhance their sustainability efforts, air-pneumatic conveying systems offer a practical and effective solution.
Applications in Various Industries
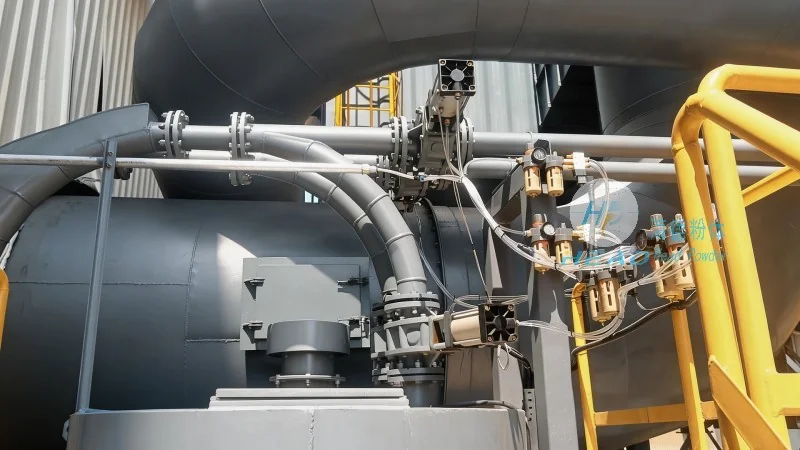
Headpowder's air-pneumatic conveying systems are versatile and can be applied across multiple industries. In the food and pharmaceutical sectors, these systems are used to transport ingredients and products with strict hygiene requirements, ensuring that the materials remain uncontaminated. In the chemical industry, they handle powders and granules that may be hazardous or reactive, providing a safe and controlled method of transport. The construction industry utilizes these systems for transporting cement, sand, and other building materials, improving efficiency on job sites. Additionally, in the agricultural sector, air-pneumatic conveyors are used to move grain and other agricultural products, reducing labor costs and improving processing speed. The adaptability of these systems makes them suitable for a wide range of applications, from small-scale operations to large industrial facilities.
Quality Assurance and Customization
Headpowder places a strong emphasis on quality assurance, ensuring that all components of the air-pneumatic conveying systems meet high standards. The company uses advanced manufacturing techniques and rigorous testing procedures to guarantee the reliability and durability of its products. Each system is customized to meet the specific needs of the client, whether it involves handling a particular type of material, operating in a specific environment, or meeting regulatory requirements. The company works closely with clients to understand their requirements and develop tailored solutions that optimize performance and efficiency. This approach ensures that the final product is not only effective but also cost-efficient and sustainable.




