The pneumatic conveying system designed for sodium nitrate material handling represents a sophisticated solution in bulk material transport. This system, developed by Shandong HeadPowder Engineering Co., Ltd., is engineered to efficiently move sodium nitrate from storage to processing units, ensuring minimal material loss and optimal operational efficiency. The system integrates advanced pneumatic technology with robust engineering, making it suitable for various industrial applications where sodium nitrate is a critical component.
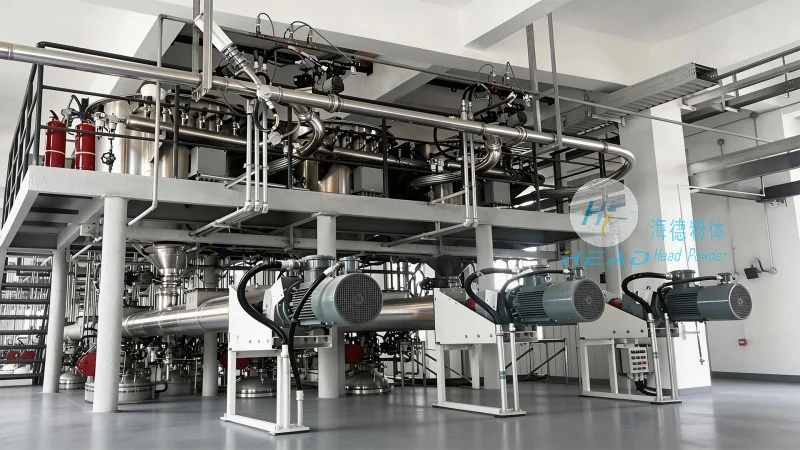
Key Components of the System
The pneumatic conveying system for sodium nitrate consists of several key components that work in tandem to achieve seamless material transport. These include the material hopper, which serves as the storage and feeding unit; the air compressor, responsible for generating the necessary air pressure to move the material; the conveying pipeline, which transports the sodium nitrate through the system; and the control system, which monitors and regulates the entire process. Each component is meticulously designed to handle the specific characteristics of sodium nitrate, such as its granular structure and potential sensitivity to moisture or temperature changes.
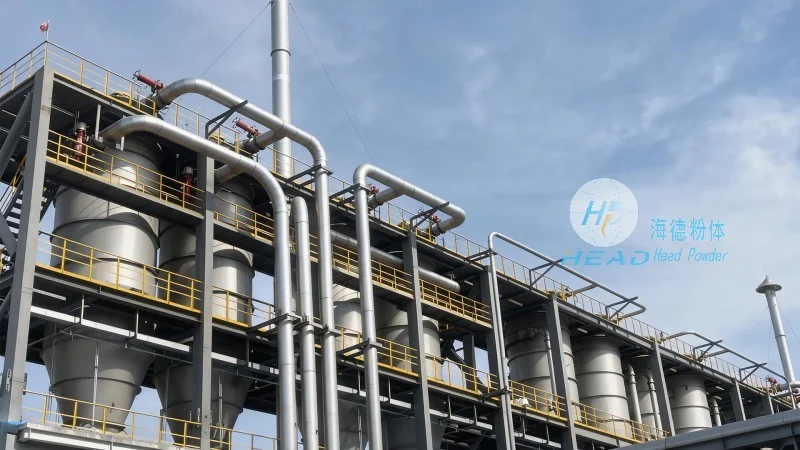
The Operation Process of the System
The operation of the sodium nitrate pneumatic conveying system follows a systematic sequence to ensure consistent and reliable material transport. Initially, sodium nitrate is fed into the material hopper from a storage silo or container. The control system then activates the air compressor, which generates a high-pressure air stream. This air stream is introduced into the conveying pipeline, creating a flow that draws the sodium nitrate particles into the system. As the material travels through the pipeline, it is propelled by the air pressure, moving from the hopper to the destination point, such as a processing unit or a storage tank. The system continuously monitors the flow rate and pressure to maintain optimal performance, adjusting the air compressor output as needed to prevent blockages or material degradation.
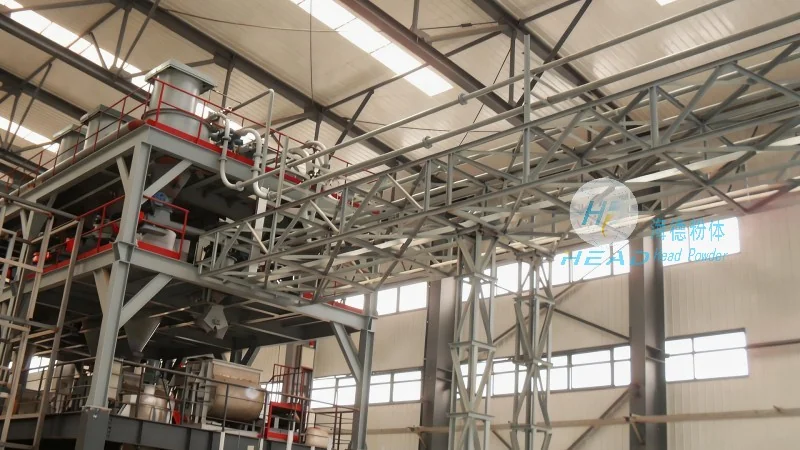
Working Principle Explained
The working principle of the sodium nitrate pneumatic conveying system is based on the principles of fluid dynamics and particle transport. The system utilizes a combination of pressure and suction to move the material. In the pressure mode, the air compressor provides a positive pressure that pushes the sodium nitrate particles through the pipeline. In the suction mode, a vacuum is created at the receiving end, drawing the material from the hopper. This dual-mode operation allows for flexibility in transporting sodium nitrate over varying distances and heights. The system's design ensures that the air and material mixture remains stable, preventing segregation or caking of the sodium nitrate particles, which could affect the system's efficiency or the quality of the material being transported.
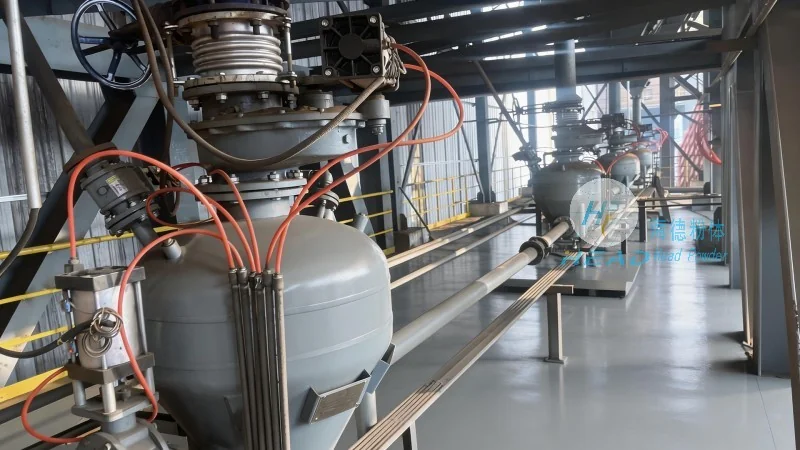
Benefits and Applications in Industrial Settings
The pneumatic conveying system for sodium nitrate offers several advantages in industrial applications. One of the primary benefits is the reduction in material handling time and labor costs, as the system automates the transport process. Additionally, it minimizes material loss and contamination, which is crucial for sodium nitrate, a material often used in food processing, fertilizers, or chemical manufacturing. The system's ability to handle large volumes of sodium nitrate efficiently makes it ideal for bulk production facilities. Shandong HeadPowder Engineering Co., Ltd. has tailored this system to meet the specific needs of various industries, ensuring that clients can achieve reliable and cost-effective material transport solutions.




