Principle and Working Scene Characteristics of Vacuum Material Handling Equipment
Release time:2026-09-19 11:01:30
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industries that require efficient and safe material transfer, vacuum material handling equipment has become a critical solution. This equipment operates on the principle of creating a negative pressure environment to draw and transport bulk materials through a network of pipes. Understanding its working mechanism and the diverse applications it supports is essential for selecting the right system for specific operational needs.
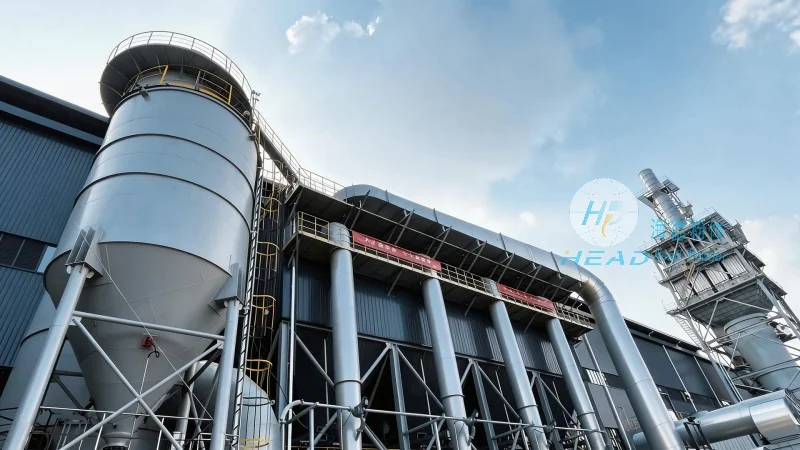
The Working Principle of Vacuum Material Handling Systems
Vacuum material handling systems rely on a central vacuum pump or fan to generate a negative pressure within the system. This vacuum is maintained throughout the pipeline network, creating a pressure differential that pulls material from the source into the system. The process typically involves a hopper or loading point where materials are introduced, a vacuum pump that drives the airflow, and a series of ducts or pipes that transport the material to the discharge point. The entire system is designed to ensure consistent material flow while maintaining the integrity of the material being handled.
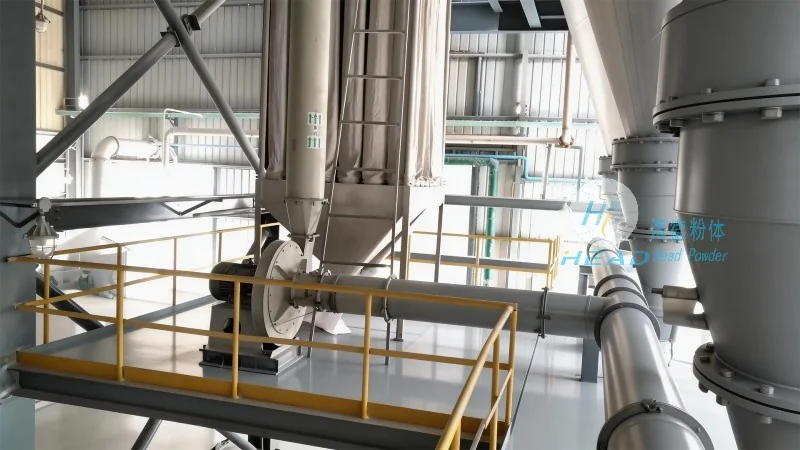
Key Working Scene Characteristics
The effectiveness of vacuum material handling equipment is defined by several key characteristics that make it suitable for a wide range of industrial applications. These include the ability to handle fine powders and granules without degradation, the provision of a dust-free and enclosed environment that enhances safety and compliance with regulations, and the flexibility to integrate with existing production lines. Additionally, the system's ability to operate quietly and with minimal maintenance makes it a preferred choice for continuous operations in various sectors.
Application Scenarios in Various Industries
In the chemical industry, vacuum material handling is used to transport reactive powders and chemicals safely, preventing contamination and exposure risks. The pharmaceutical sector benefits from its ability to maintain sterile conditions and ensure product purity, which is crucial for drug manufacturing. Food processing industries utilize these systems to handle ingredients like flour, sugar, and spices, ensuring food safety standards are met while maintaining product quality. Other applications include the handling of metal powders in metallurgy and the transfer of agricultural products in the agricultural sector.
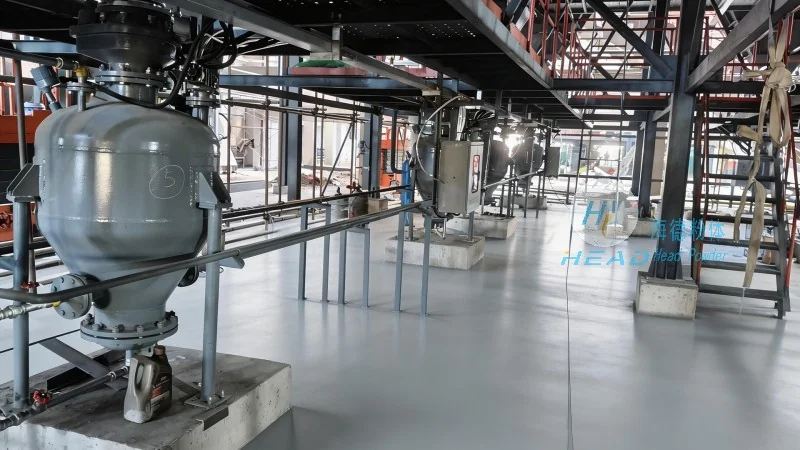
HeadPowder's Expertise in Vacuum Material Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in designing and manufacturing vacuum material handling equipment tailored to meet the unique requirements of different industries. With a focus on the fundamental principles of negative pressure technology and the diverse working scene characteristics, HeadPowder provides customized solutions that enhance operational efficiency and safety. The company's products are engineered to handle a variety of materials, from fine powders to bulk granules, and are designed to integrate seamlessly into existing production environments. By leveraging their expertise in vacuum technology, HeadPowder ensures that clients receive reliable and efficient material handling systems that meet industry standards and regulatory requirements.




