Coal fly ash, a byproduct of coal combustion, is a crucial material in various industrial applications. Efficient handling and transportation of this material are essential for optimizing production processes and ensuring environmental compliance. This article explores the principles underlying coal fly ash material handling and highlights the key characteristics of its working scenarios, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
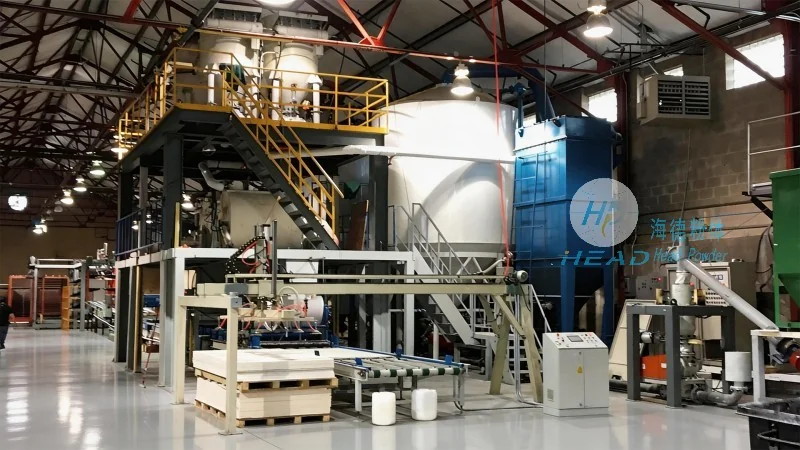
Introduction to Coal Fly Ash Material Handling
Coal fly ash, also known as fly ash, is a fine powder produced during the combustion of coal in thermal power plants. It consists of microscopic particles of silica, alumina, and other minerals. Due to its fine texture and high volume, transporting coal fly ash requires specialized equipment and systems to ensure safety, efficiency, and environmental protection. The handling of coal fly ash involves several stages, including collection, storage, and transportation to end-use locations such as concrete production facilities, brick factories, or landfills.
HeadPowder: A Leading Provider in Coal Fly Ash Handling Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent company dedicated to providing comprehensive solutions for coal fly ash material handling. With a strong presence in China, particularly in Shandong province, HeadPowder has established itself as a trusted partner for industries relying on coal fly ash. The company specializes in designing, manufacturing, and implementing advanced material handling systems tailored to the unique challenges of coal fly ash transportation.
The Principles of Coal Fly Ash Material Handling
The core principles of coal fly ash material handling revolve around ensuring the safe and efficient movement of this fine material. Key principles include:
Minimizing dust generation and airborne emissions to comply with environmental regulations and protect worker health.
Optimizing material flow to reduce energy consumption and operational costs.
Ensuring the integrity of the material during transport to prevent segregation and loss of valuable components.
Adapting systems to handle varying ash characteristics, such as moisture content and particle size distribution.
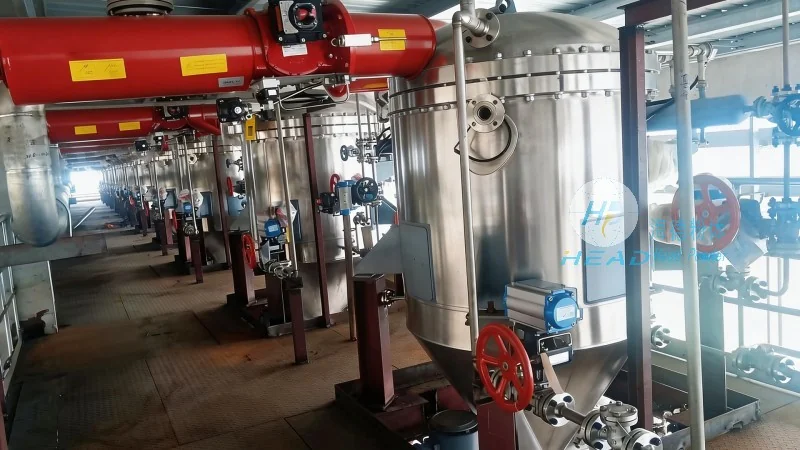
Advanced technologies, such as pneumatic conveying systems and bulk material handling equipment, are employed to meet these principles. Pneumatic conveying, for instance, uses air pressure to transport coal fly ash through pipelines, offering a dust-free and efficient method for long-distance transportation. HeadPowder's expertise lies in customizing these systems to match the specific requirements of each client, ensuring optimal performance and reliability.
Working Scene Characteristics of Coal Fly Ash Material Handling
The working scenarios for coal fly ash material handling vary based on the application and location. Key characteristics include:
Industrial settings, such as thermal power plants and concrete production sites, where large volumes of ash are generated and need to be transported to processing facilities.
Construction and infrastructure projects that utilize coal fly ash as a supplementary cementitious material in concrete, requiring consistent and reliable supply.
Environmental management scenarios, including ash storage and disposal, where containment and controlled release are critical.
Urban and remote locations, necessitating flexible and adaptable handling systems that can operate in diverse environmental conditions.
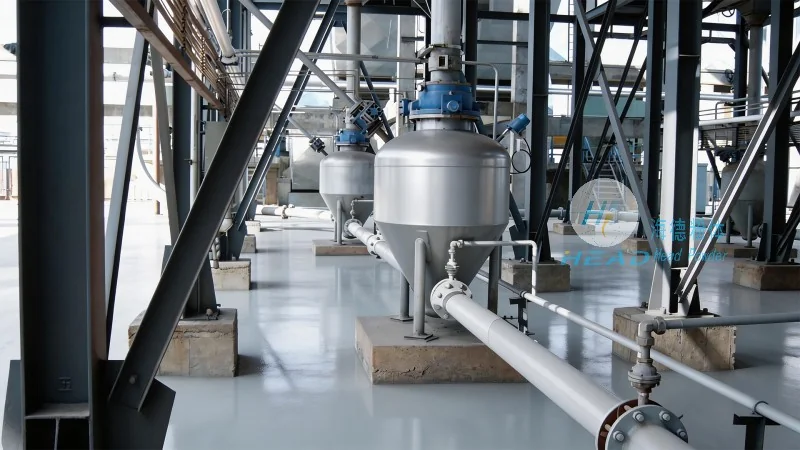
HeadPowder's systems are designed to accommodate these diverse working scenarios. For example, in industrial plants, the company provides integrated material handling solutions that include ash collection hoppers, conveyor belts, and pneumatic conveying pipelines. In construction sites, HeadPowder's equipment ensures that coal fly ash is delivered in a controlled manner, supporting the production of high-quality concrete with enhanced durability and sustainability.
Advantages of HeadPowder's Coal Fly Ash Handling Systems
HeadPowder's coal fly ash material handling systems offer several advantages that make them ideal for modern industrial applications:
Enhanced safety through dust control and enclosed systems, reducing health risks for workers and minimizing environmental impact.
Increased efficiency with optimized material flow, leading to lower operational costs and higher productivity.
Customization to meet specific material characteristics and application requirements, ensuring tailored solutions for each client.
Reliability and durability of equipment, designed to withstand the harsh conditions associated with coal fly ash handling.
By adhering to these principles and characteristics, HeadPowder's solutions contribute to the efficient and sustainable use of coal fly ash, supporting industries in achieving their operational and environmental goals. The company's commitment to innovation and customer satisfaction ensures that clients receive the best possible material handling solutions for their coal fly ash needs.




