For pharmaceutical and nutraceutical manufacturers, the efficient and reliable handling of capsule materials is a critical aspect of production. The capsule material conveying system, a specialized piece of equipment designed to transport and manage capsule products, plays a vital role in ensuring smooth workflow and maintaining product integrity. This article delves into the working principle and key features of such systems, highlighting how they contribute to operational efficiency and quality control in the manufacturing process.
Understanding the Working Principle of Capsule Material Conveying Systems
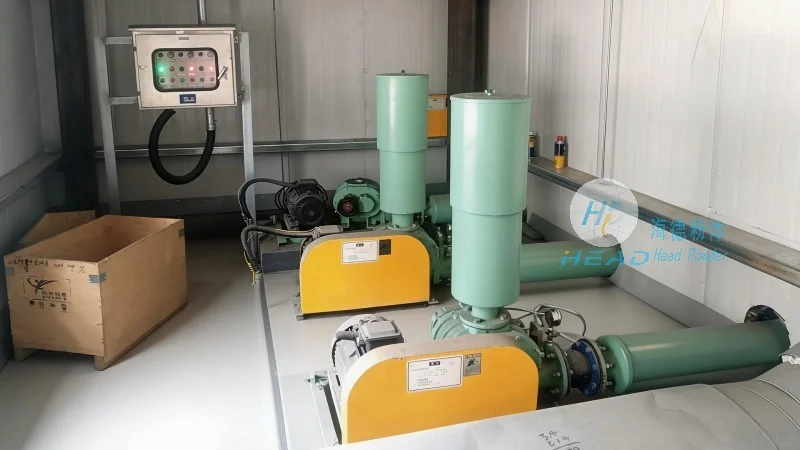
The core function of a capsule material conveying system is to move capsule products from one stage of production to another with precision and minimal disruption. These systems typically operate through a combination of mechanical components and control mechanisms that work in tandem to achieve seamless material transfer. The process generally begins with the loading of capsules into the system, which may involve a hopper or feeding mechanism that ensures a consistent flow of material. From there, the capsules are transported via conveyor belts, rollers, or other guided pathways, depending on the system design. Advanced systems may incorporate sensors and feedback loops to monitor the speed and quantity of capsules, allowing for real-time adjustments to maintain optimal performance. The final stage involves the discharge of capsules into a collection container or directly to the next processing unit, such as a filling or packaging machine. This entire process is designed to minimize product damage, reduce downtime, and enhance overall productivity.
Key Features of Capsule Material Conveying Systems
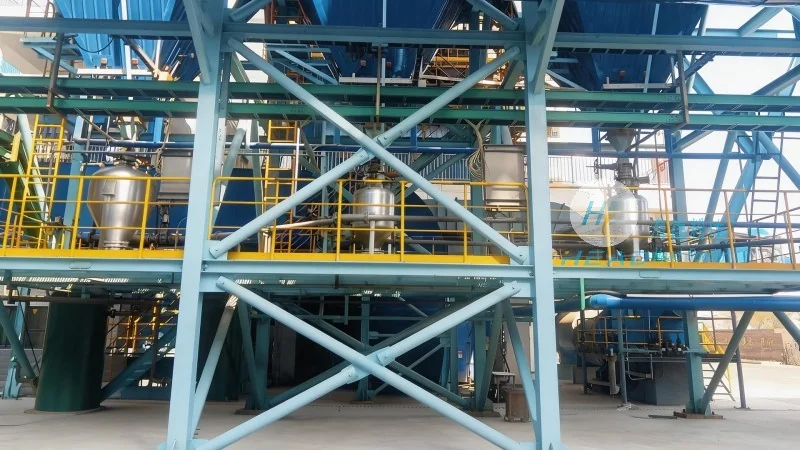
Modern capsule material conveying systems are equipped with several features that enhance their functionality and adaptability to various production needs. One of the most notable features is the ability to handle different capsule sizes and types, including hard gelatin capsules, soft gel capsules, and even specialized formulations. This versatility allows manufacturers to use a single system for multiple product lines, reducing inventory and operational costs. Another critical feature is the integration of cleaning and maintenance protocols, which are essential for maintaining hygiene standards in pharmaceutical and food industries. Many systems are designed with easy-to-clean surfaces and removable components, facilitating regular sanitation to prevent contamination. Additionally, advanced systems may include automation capabilities, such as programmable logic controllers (PLCs) and user-friendly interfaces, enabling operators to adjust settings quickly and efficiently. This automation not only improves operational efficiency but also reduces the risk of human error. Furthermore, the systems often incorporate safety features, such as emergency stop buttons and protective guards, to ensure the well-being of operators and compliance with safety regulations. These features collectively contribute to a safer, more reliable, and more efficient production environment.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
At the forefront of providing innovative solutions for capsule material handling, Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer specializing in the design and production of high-quality conveying systems. With a strong commitment to quality and customer satisfaction, the company has established itself as a trusted partner for pharmaceutical and nutraceutical manufacturers worldwide. Headquartered in Shandong, China, the company leverages decades of industry experience and cutting-edge technology to develop systems that meet the evolving demands of the market. The team at HeadPowder is dedicated to delivering customized solutions tailored to each client's specific requirements, ensuring that the systems are optimized for their unique production processes. By focusing on both functionality and durability, HeadPowder aims to enhance the efficiency and reliability of capsule material handling for its clients, contributing to their overall success in the competitive manufacturing landscape.
Conclusion
In conclusion, capsule material conveying systems are essential components in the production workflow of capsule-based products. Their working principle, which involves precise material transport and real-time monitoring, ensures that capsules are handled efficiently and with minimal risk of damage. The key features of these systems, including versatility, hygiene compliance, automation, and safety, further enhance their value to manufacturers. As a leading provider in the industry, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and deliver high-quality solutions that meet the stringent requirements of the pharmaceutical and nutraceutical sectors. By investing in such systems, manufacturers can improve operational efficiency, maintain product quality, and stay competitive in the global market.




