Wheat negative pressure pneumatic conveying equipment represents a sophisticated solution for the efficient and reliable transportation of wheat and related grain products. This technology operates by creating a vacuum or negative pressure environment within a pipeline system, which draws the material from a source, such as a storage silo or hopper, and transports it to a designated destination, like a processing facility or storage area. The design of these systems is pivotal for optimizing material handling efficiency, energy consumption, and overall operational safety in agricultural and food processing applications.
Key Technical Aspects and System Components
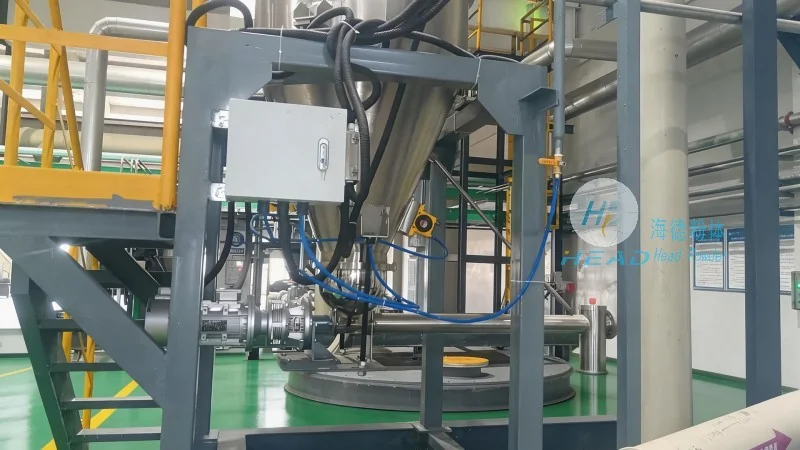
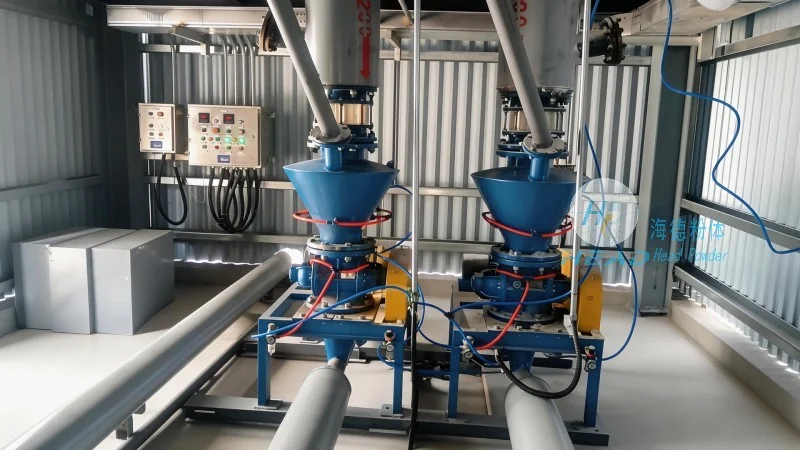
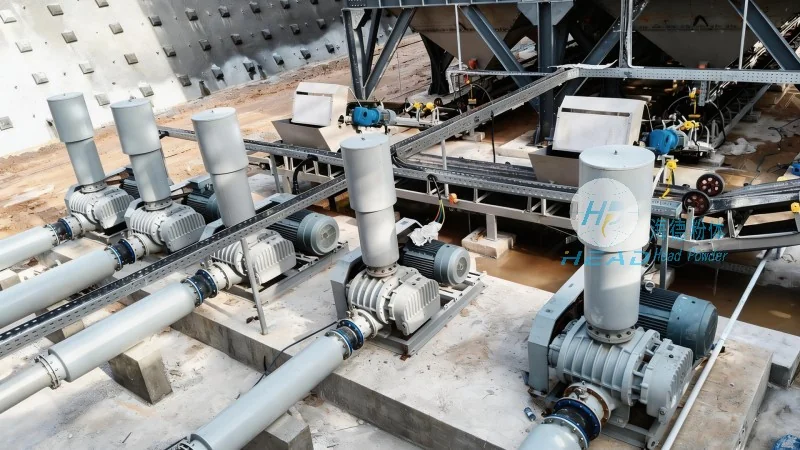
HeadPowder, a prominent manufacturer headquartered in Shandong, China, specializes in the development and production of advanced wheat negative pressure pneumatic conveying equipment. The core components of such systems typically include a vacuum pump or fan to generate the necessary negative pressure, an inlet hopper or feeder for material loading, and a network of pipelines designed to guide the material flow. The equipment is engineered to handle various grain types, including wheat, with consistent performance and minimal material degradation. Technical specifications may vary based on the specific application, but common features include adjustable flow rate controls, pressure monitoring systems, and material separation mechanisms to prevent blockages and ensure smooth operation. The system also incorporates safety features, such as pressure relief valves and emergency shut-off mechanisms, to protect against operational hazards.
Operational Advantages and Industry Applications
The wheat negative pressure pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers several significant operational advantages. One of the primary benefits is the reduction in labor costs associated with manual material handling, as the system automates the loading, conveying, and unloading processes. Additionally, the negative pressure environment helps in maintaining high hygiene standards by minimizing direct human contact with the grain, which is crucial for food safety and quality control. The system also enhances safety by eliminating the need for manual lifting and moving of heavy grain loads, reducing the risk of workplace injuries. Furthermore, the equipment is capable of handling large volumes of material efficiently, making it suitable for both small-scale and large-scale agricultural operations. Its applications span across various stages of grain processing, including from storage to processing and packaging, providing a seamless material flow solution.
Customization, Installation, and After-Sales Support
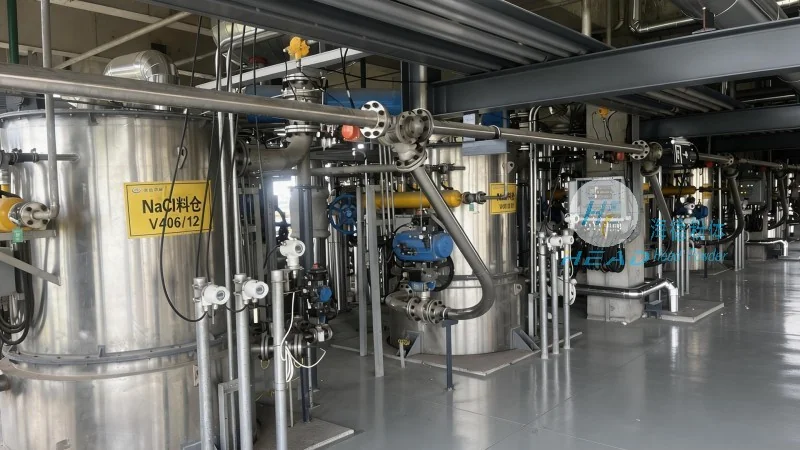
HeadPowder provides customized solutions tailored to the unique requirements of each client. The company’s engineering team works closely with customers to assess their operational needs, space constraints, and material characteristics, and then designs a system that meets all these criteria. The equipment is manufactured using high-quality materials, such as stainless steel and corrosion-resistant alloys, to ensure durability and long-term performance under demanding conditions. After installation, HeadPowder offers comprehensive training programs to ensure that the client’s personnel can operate and maintain the system effectively. The company also provides regular maintenance services and technical support to address any issues that may arise during operation. The commitment to quality and customer satisfaction is evident in its after-sales service, which includes warranty coverage and prompt response to service requests.




