Efficiently transporting solid powders is a critical challenge in many industrial processes. Pneumatic conveying systems offer a solution by utilizing air flow to move powders from one location to another, eliminating the need for mechanical components like belts or buckets. This method is widely used in sectors such as food processing, pharmaceuticals, and chemical manufacturing due to its ability to handle delicate materials without contamination or degradation.
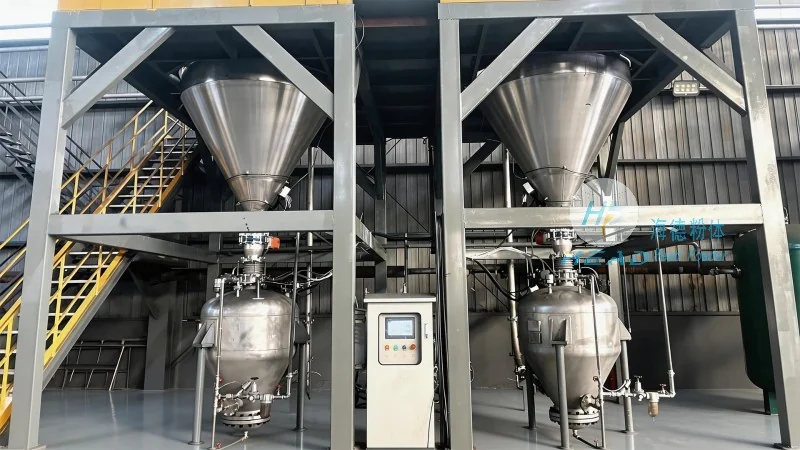
Pneumatic Conveying Systems: The Core Technology
Pneumatic conveying relies on the principle of using compressed air or gas to create a flow that carries powder particles. There are two main types: dilute phase and dense phase. Dilute phase systems use higher air velocities to transport powders in a dispersed state, suitable for long-distance and high-speed applications. Dense phase systems, on the other hand, operate at lower velocities, ensuring gentle handling of sensitive materials. The choice between these systems depends on the material's properties, such as particle size, density, and moisture content, as well as the required distance and throughput.
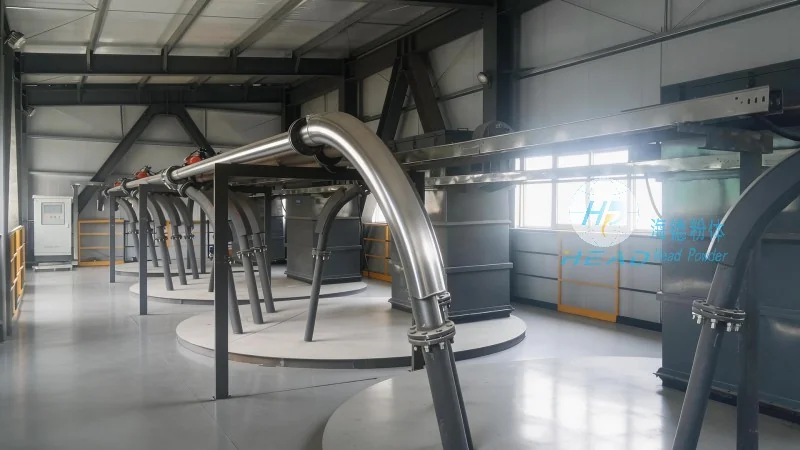
HeadPowder Engineering: Experts in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced pneumatic conveying systems. With a strong presence in China, particularly in Shandong, the company specializes in designing, manufacturing, and installing customized solutions tailored to the unique needs of each client. HeadPowder's team of engineers and technicians leverages decades of experience to develop systems that optimize material handling efficiency while minimizing operational costs and maintenance requirements.
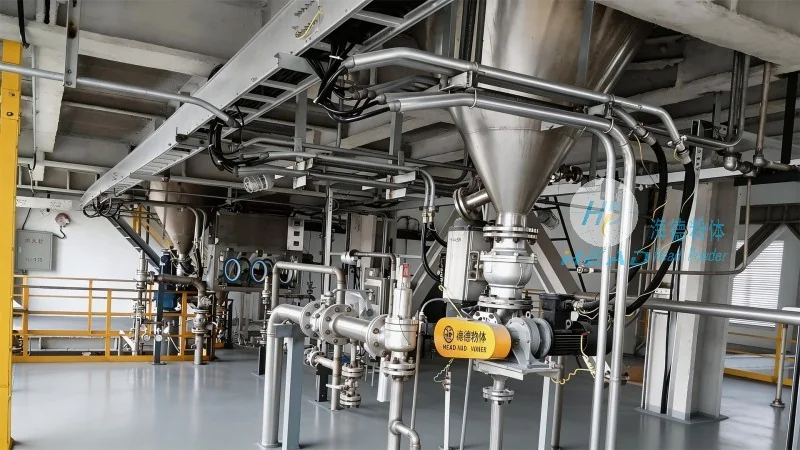
Key Features and Advantages of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems are engineered with several key features that enhance performance and reliability. These include high-efficiency air compressors that ensure consistent air pressure, advanced material feeders that prevent blockages and ensure uniform flow, and robust pipeline designs that minimize pressure drop and energy consumption. The company's systems are also designed for easy integration with existing production lines, reducing downtime during installation and operation. Additionally, HeadPowder prioritizes safety and compliance, incorporating features such as explosion-proof designs for hazardous materials and automated monitoring systems to detect and address issues in real-time.
Applications and Industries Served
The versatility of pneumatic conveying makes it suitable for a wide range of applications across various industries. In the food and beverage sector, HeadPowder's systems are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and contamination-free handling. In the pharmaceutical industry, the gentle and sterile nature of pneumatic conveying is crucial for transporting active pharmaceutical ingredients (APIs) and other sensitive materials. Chemical manufacturers benefit from the system's ability to handle corrosive or abrasive powders without damaging equipment. Furthermore, the technology is applied in mining and minerals processing to transport raw materials and finished products efficiently.
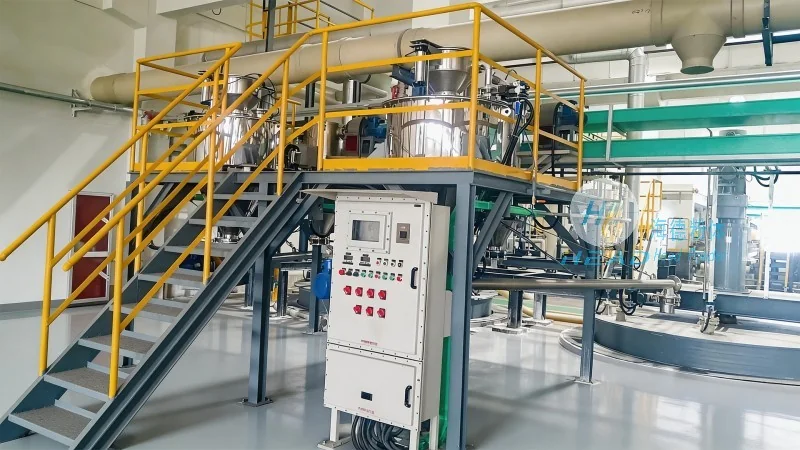
Customization and After-Sales Support
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers comprehensive customization services to meet specific needs. This includes selecting the appropriate conveying type (dilute or dense phase), determining the optimal air velocity and pressure, and designing the system layout to fit the client's facility. After the system is installed, HeadPowder provides ongoing support, including regular maintenance, spare parts availability, and technical assistance. The company's commitment to customer satisfaction is reflected in its long-term partnerships with clients who rely on its systems for consistent and reliable performance.




