HeadPowder, an industry leader in material handling technology, specializes in providing advanced pneumatic conveying systems tailored for the transportation of rare earth powders. With a strong presence in Shandong, China, the company combines decades of engineering expertise and innovative solutions to meet the unique challenges of transporting fine and abrasive materials like rare earth powders over extended distances.
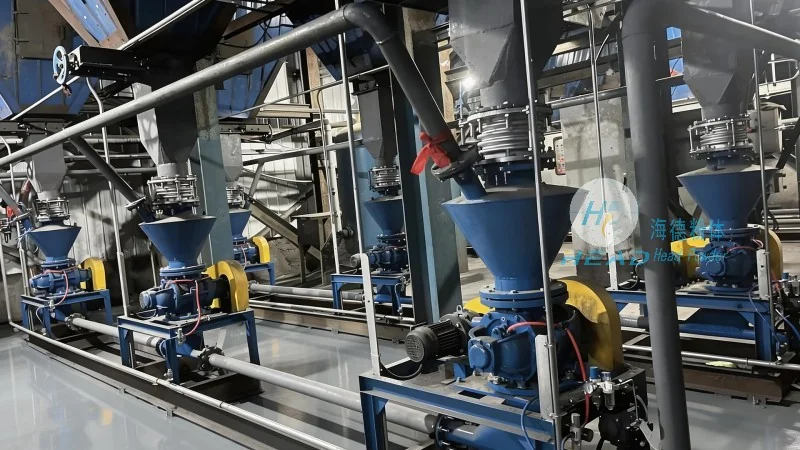
Advanced Pneumatic Conveying Systems for Rare Earth Powders
Our core product, the rare earth powder pneumatic conveying system, is engineered to overcome the traditional limitations of material transport, such as distance and material handling efficiency. By utilizing air as the conveying medium, this system enables seamless and efficient movement of rare earth powders from source to destination, ensuring minimal loss, reduced contamination, and enhanced operational reliability. The system is designed to handle the specific properties of rare earth powders, including their fine particle size and potential for static electricity, which are critical factors in maintaining product quality and system performance.
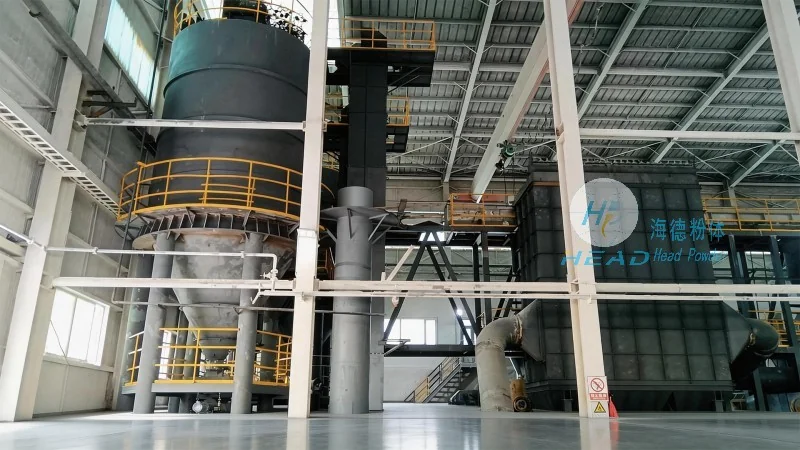
Key Advantages of Our Pneumatic Conveying Solutions
Implementing our rare earth powder pneumatic conveying system offers several distinct advantages for industrial applications. Firstly, it significantly reduces the need for traditional bulk handling equipment, such as conveyor belts or trucks, thereby lowering operational costs and space requirements. Secondly, the system minimizes material degradation and contamination, which is essential for maintaining the purity and quality of rare earth powders—critical for their use in high-tech industries like electronics and renewable energy. Additionally, the technology provides greater flexibility in layout and process integration, allowing for customized solutions that adapt to specific production line configurations. Finally, the system enhances safety by eliminating manual handling of hazardous or fine powders, reducing the risk of dust explosions and worker exposure.
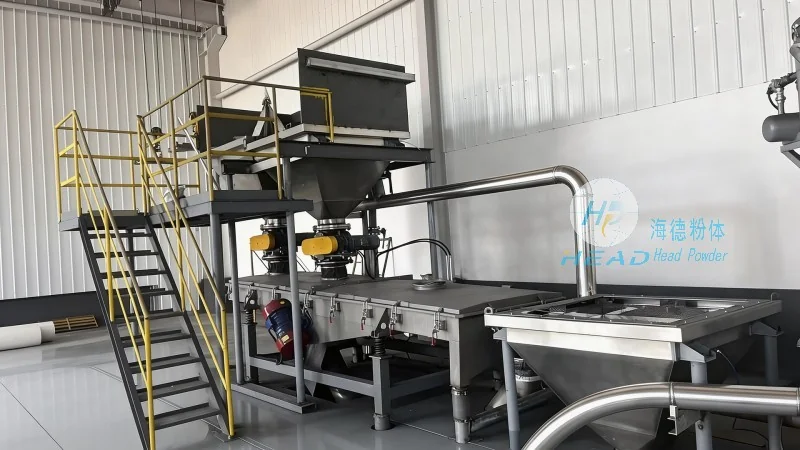
Technical Features and Innovations
Our pneumatic conveying systems incorporate several technical innovations to ensure optimal performance and reliability. The system utilizes a combination of positive and negative pressure modes, allowing for both low and high-pressure applications depending on the distance and material characteristics. This dual-mode capability ensures efficient transport even over long distances, typically up to several kilometers, without compromising on material integrity. Furthermore, the system includes advanced filtration and separation mechanisms to prevent particle accumulation and maintain consistent air quality, which is vital for preventing system blockages and ensuring continuous operation. The use of high-quality materials, such as corrosion-resistant stainless steel, ensures durability and longevity, even in harsh industrial environments where rare earth powders may be corrosive or abrasive.
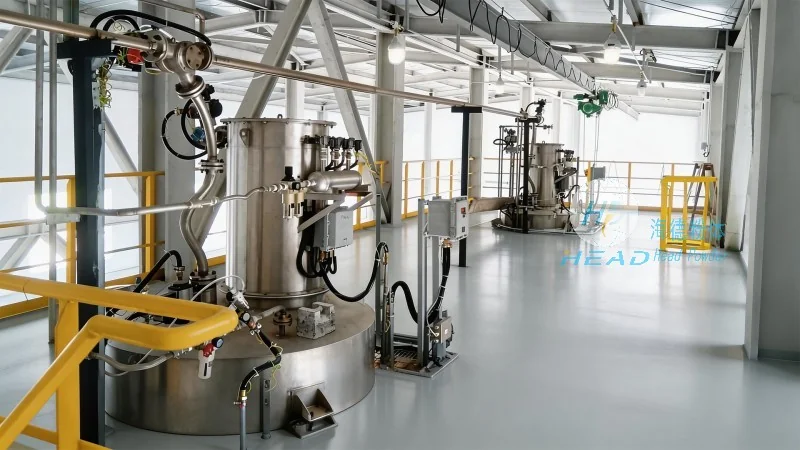
Customized Solutions for Diverse Industrial Needs
HeadPowder understands that each industrial application has unique requirements. Therefore, we offer customized pneumatic conveying solutions that are tailored to the specific needs of our clients. Whether the goal is to transport rare earth powders from a storage silo to a processing plant, or to move materials between different production stages, our systems are designed to integrate seamlessly with existing infrastructure. Our engineering team works closely with clients to assess their operational parameters, including material flow rates, distance, and environmental constraints, to develop a solution that maximizes efficiency and minimizes downtime. By leveraging our expertise in material handling and pneumatic technology, we provide solutions that not only meet but exceed industry standards, ensuring long-term performance and customer satisfaction.




