Efficient and environmentally friendly material handling is a critical concern in modern industrial operations, particularly in the processing of coke particles. Pneumatic conveying systems offer a sophisticated solution to transport coke from one location to another while minimizing environmental impact and operational costs. This article explores the benefits, applications, and technical aspects of coke particle pneumatic conveying, highlighting how it serves as a superior alternative to traditional methods.
About HeadPowder Engineering Co., Ltd.
HeadPowder, a leading provider in the field of material handling solutions, specializes in designing and manufacturing advanced pneumatic conveying systems. With a strong commitment to innovation and sustainability, the company has established itself as a trusted partner for industries relying on coke processing and transportation. HeadPowder's expertise lies in developing customized solutions that meet the unique demands of each client, ensuring optimal performance and reliability. The company is headquartered in Shandong, China, and has built a reputation for delivering high-quality, durable equipment tailored to the needs of its clients.
Key Features of Coke Particle Pneumatic Conveying Systems
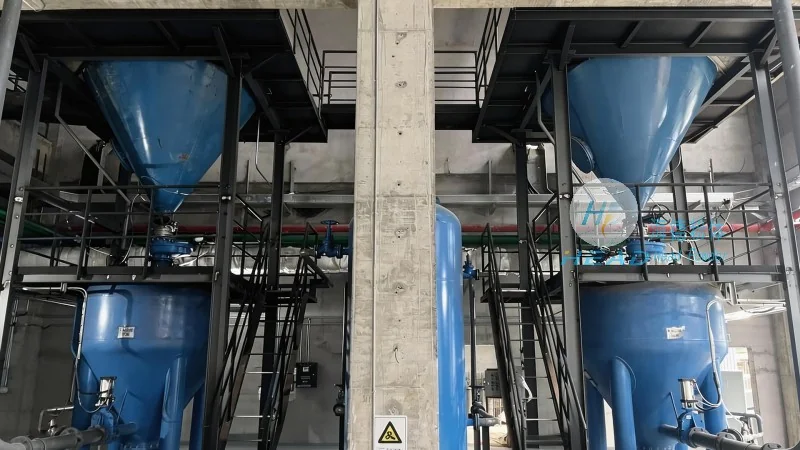
The core of a coke particle pneumatic conveying system is its ability to transport bulk materials through a network of pipes using air or other gases. This method eliminates the need for mechanical components like belts or buckets, reducing maintenance requirements and enhancing safety. The system typically consists of a hopper for material storage, a rotary valve to control the flow of coke, a conveyor line where the material is propelled by air, and a receiver to collect the material at the destination. HeadPowder's systems are engineered with high-quality materials such as stainless steel and corrosion-resistant alloys, ensuring durability even in harsh industrial environments. Advanced control technologies, including PLC (Programmable Logic Controller) systems, are integrated to monitor and regulate the conveying process, ensuring smooth and continuous operation.
Efficiency and Environmental Benefits
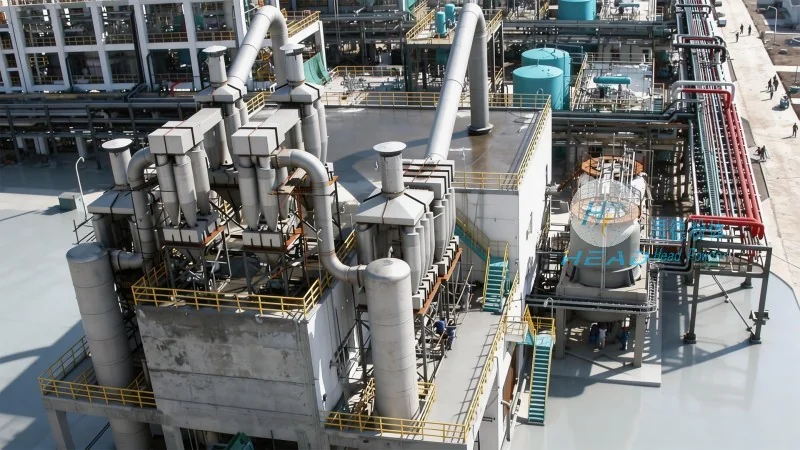
Compared to traditional conveyor systems, pneumatic conveying offers significant advantages in terms of energy efficiency and environmental protection. By utilizing compressed air, the system minimizes dust emissions and prevents material contamination, which is crucial for maintaining a clean and safe working environment. Additionally, the absence of moving parts reduces energy consumption, leading to lower operational costs over time. HeadPowder's solutions are designed to comply with environmental regulations, making them an ideal choice for companies aiming to reduce their carbon footprint while improving productivity. The system also reduces the risk of material spillage and cross-contamination, which is vital in industries where product purity is paramount.
Applications in Industrial Settings
Coke particle pneumatic conveying is widely used in various industrial applications, including steel production, chemical processing, and power generation. In steel mills, for example, the system efficiently transports coke from storage facilities to blast furnaces, ensuring a steady supply of raw materials. The blast furnaces require a consistent flow of coke to maintain optimal combustion, and the pneumatic system provides this reliability. In chemical plants, it helps in the handling of coke-derived products, such as coke oven gas and byproducts, facilitating seamless production processes. The versatility of the system allows it to handle different particle sizes and moisture levels, making it adaptable to diverse industrial needs. Whether it's a small-scale operation or a large industrial plant, HeadPowder's systems are designed to meet the specific requirements of each application.
Technical Advancements and Customization
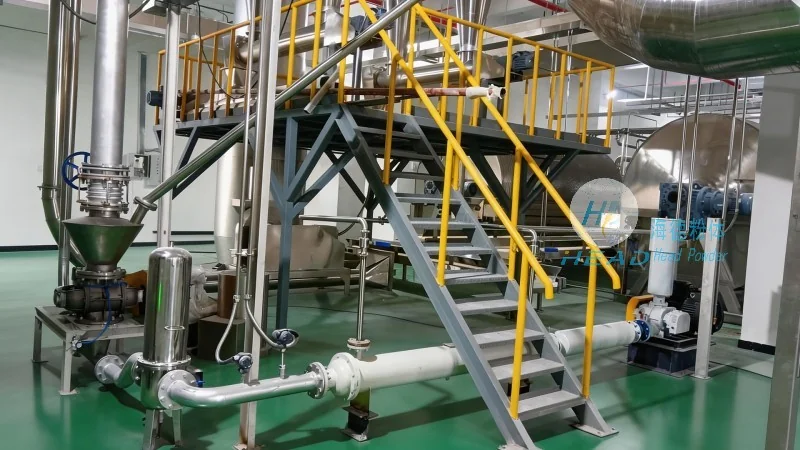
HeadPowder Engineering Co., Ltd. leverages cutting-edge technology to enhance the performance of its coke particle pneumatic conveying systems. The company employs advanced simulation tools to optimize system design, ensuring that each component operates at peak efficiency. Customization is a key strength of HeadPowder, as they work closely with clients to understand their specific requirements and tailor solutions accordingly. For instance, the system can be adjusted to handle varying coke particle sizes, from fine powders to larger lumps, by modifying the hopper and valve designs. The company also offers options for different air pressures and flow rates, allowing for flexibility in operation. Additionally, HeadPowder provides comprehensive support services, including installation, maintenance, and training, to ensure that clients can maximize the benefits of their investment.
Conclusion and Contact Information
As the demand for sustainable and efficient material handling solutions grows, coke particle pneumatic conveying stands out as a reliable and eco-friendly option. HeadPowder Engineering Co., Ltd. continues to lead the industry with its innovative products and commitment to excellence. By choosing a pneumatic conveying system from HeadPowder, industries can enhance their operational efficiency, reduce environmental impact, and achieve long-term cost savings. The company's headquarters is located in Shandong, China, and it serves clients globally with its advanced technology and customer-centric approach. For more information about their solutions, please contact HeadPowder Engineering Co., Ltd. for a consultation tailored to your specific needs.




